
ماكينة حقن ونفخ عالية الإنتاجية EP80 بقوة 800 كيلو نيوتن، معدات تشكيل زجاجات خالية من الزوائد
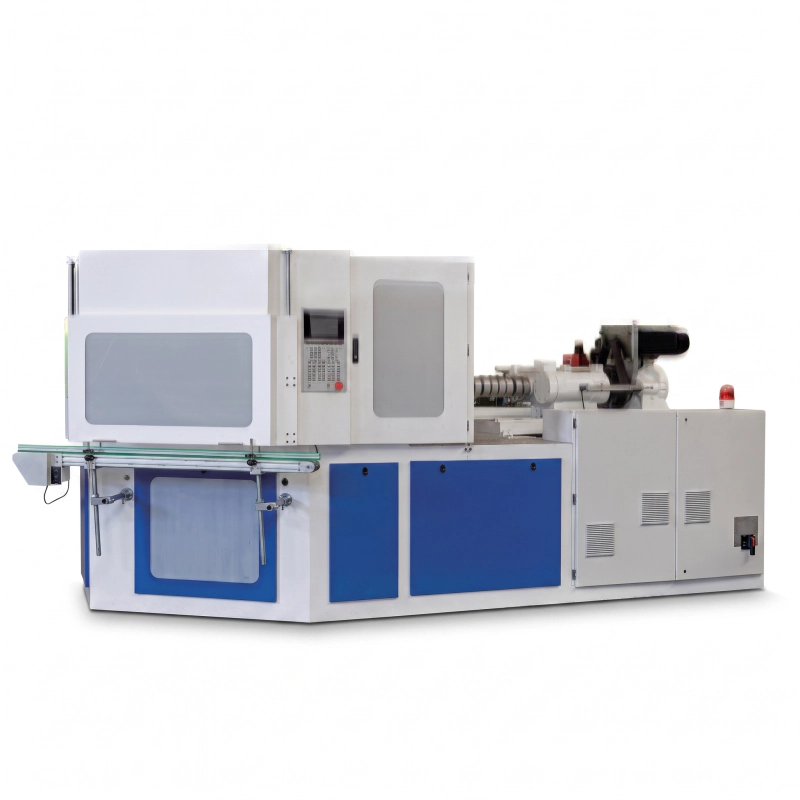
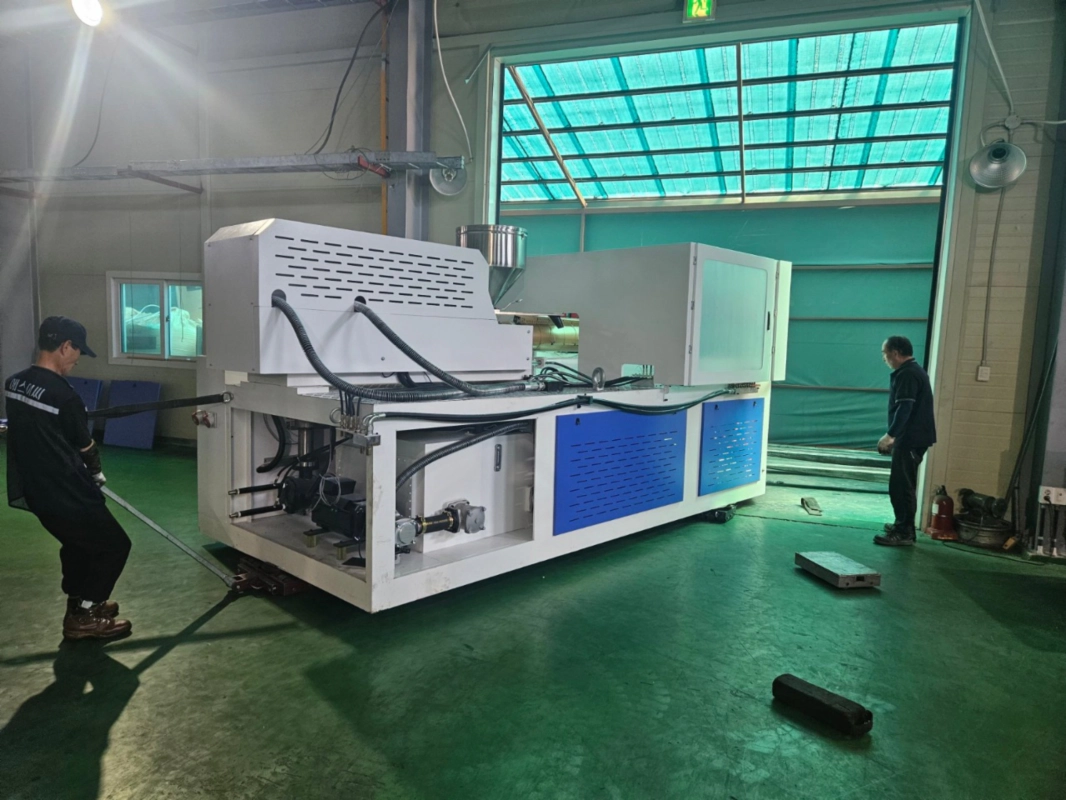
EVER POWER EP80 injection blow molding machine offers 800KN clamping force, 466g injection weight, up to 20 cavities at 10ml. Dual hydraulic system standard, high-precision angle divider for mold-tower synchronization. Produces 1-2000ml flash-free bottles for pharma, cosmetic and food industries. CE ISO, 4s dry cycle, 10 Ton.
What Is the EVER POWER EP80 One-Step Injection Blow Molding Machine?
The EVER POWER EP80 is a fully automatic one-step IBM (Injection Blow Molding) machine engineered for precision hollow container production. As a dedicated مصنع آلات حقن القوالب بالنفخلقد ركزت شركة EVER POWER عقودًا من الخبرة في مجال الأدوات والعمليات في هذا النموذج، مما أدى إلى تقديم آلة يتم فيها إكمال الزجاجة بأكملها - من حقن الشكل الأولي إلى النفخ النهائي إلى الإخراج - في دورة آلة واحدة دون تدخل المشغل، ودون نقل المواد بين الآلات، ودون الوميض ونفايات خط الفصل التي تميز أنظمة نفخ البثق.
هذا آلة IBM بخطوة واحدة is the preferred choice for pharmaceutical bottle blowing and cosmetic container manufacturing where dimensional consistency is non-negotiable. Each cycle on the EP80 runs three simultaneous operations: while new preforms are being injection-molded at Station 1, the previous batch is being blown to final shape at Station 2, and the completed bottles from Station 2 are being stripped and conveyed to the outfeed conveyor at Station 3. This triaxial parallelism means the productive output equals the injection cycle time alone - not the sum of injection plus blowing plus ejection - giving the EP80 a significant throughput advantage over two-stage stretch blow systems for small and medium volume containers.
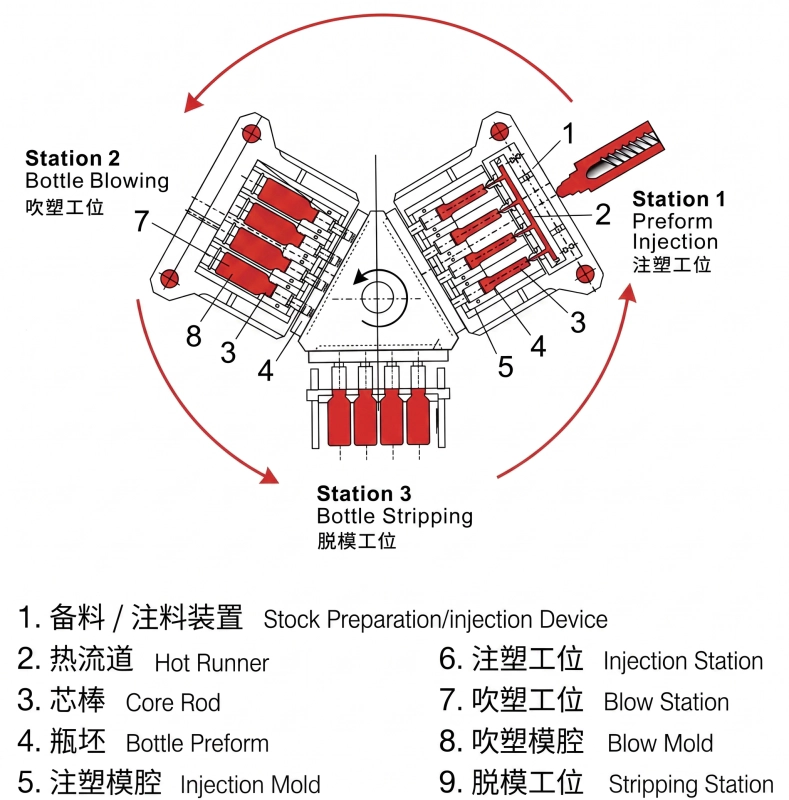
Three-Station Process: How the EP80 Works
المحطة 1 - حقن القوالب الأولية
تُصهر حبيبات البلاستيك في الأسطوانة وتُحقن في تجويف الحقن تحت ضغط مُتحكم به. يتم تشكيل عنق الزجاجة وشكل الخيط بدقة في قالب الحقن. يُفتح قالب الحقن، وينتقل المندريل الحامل للشكل الأولي الساخن إلى المحطة 2 عبر البرج الدوار.
المحطة 2 - التشكيل بالنفخ
يُنفخ القالب الساخن بالهواء المضغوط من قلب القالب. ويتحدد شكل الزجاجة بالكامل بواسطة تجويف قالب النفخ. ينفخ الهواء القالب للخارج باتجاه جدران القالب المبردة، فتأخذ الزجاجة أبعادها النهائية. يُفتح القالب وتتقدم وحدة النفخ إلى المحطة 3.
المحطة 3 - الإخراج والنقل
تُزال الزجاجات المبردة بعد الانتهاء من تصنيعها من القوالب وتُفرغ على سير النقل. وبما أن المحطات الثلاث تعمل في وقت واحد، فإن الدورة تتكرر باستمرار. لا توجد عملية ثانوية، ولا مكبس لإزالة الزوائد، ولا حاجة لإعادة تسخين الزجاجات - فالعمليات الثلاث تشترك في دورة واحدة.
Main Technical Parameters - EVER POWER EP80
| المعلمة | البند (EN) | وحدة | الحلقة 80 |
|---|---|---|---|
| نظام الحقن | |||
| قطر البرغي | قطر البرغي | مم | 55 mm |
| نسبة طول/قطر البرغي | برغي L/D | - | 22:1 |
| وزن الحقنة | وزن الحقنة | ز | 466 g |
| الطاقة الحرارية | الطاقة الحرارية | كيلوواط | 18 KW |
| مناطق تسخين البراميل | عدد مناطق البراميل | - | 4+N |
| السكتة الدماغية الناتجة عن الحقن | السكتة الدماغية الناتجة عن الحقن | مم | 180 mm |
| نظام التثبيت | |||
| قوة مشبك الحقن | قوة تثبيت الحقن | KN | 800 |
| شوط فتح الحقن | شوط فتح الحقن | مم | 140 مم |
| قوة مشبك النفخ | قوة النفخ في عملية التثبيت | KN | 120 |
| ضربة فتح النفخ | ضربة الفتح للنفخ | مم | 140 مم |
| ارتفاع مصعد البرج | ارتفاع رفع الطاولة الدوارة | مم | 70 مم |
| قالب | |||
| أقصى حجم للوحة (الطول × العرض) | أقصى حجم للوحة (الطول × العرض) | مم | 800x400 mm |
| سُمك القالب | سُمك القالب | مم | 280 mm |
| أقصى قطر للزجاجة | قطر الزجاجة | مم | 120 مم |
| أقصى ارتفاع للزجاجة | ارتفاع الزجاجة | مم | 220 مم |
| نطاق حجم الزجاجة | حجم الزجاجة المناسب | مل | 1-2000 |
| ضربة التعرية | ضربة التعرية | مم | 230 مم |
| النظام الهيدروليكي | |||
| الضغط الهيدروليكي | الضغط الهيدروليكي | ميجا باسكال | 14 |
| قوة المحرك | قوة المحرك | كيلوواط | 18.5+18.5 KW |
| مدة دورة التجفيف | دورة التجفيف | S | 4 |
| القوة الكاملة | القوة الكاملة | كيلوواط | 55 |
| الطاقة التشغيلية | الطاقة التشغيلية | % | 52-70 |
| معايير أخرى | |||
| ضغط الهواء المضغوط | مين إير | ميجا باسكال | 0.7-1.2 |
| سعة الهواء | سعة الهواء المضغوط | م3/دقيقة | 0.7 |
| تدفق مياه التبريد | تدفق المياه | متر مكعب/ساعة | 4 |
| ضغط ماء التبريد | ضغط ماء التبريد | ميجا باسكال | 0.3-0.4 |
| الأبعاد (الطول × العرض × الارتفاع) | الأبعاد الكلية | م | 4.5x1.6x2 M |
| الوزن الصافي | الوزن الصافي | طن | 10 Ton |
ملاحظة: جميع المعايير هي للإشارة فقط. تحتفظ شركة إيفر باور بالحق في تعديل المواصفات نتيجة لتحسينات المعدات.
Max Cavity Count per Container Volume (EP80 - For Reference)
| مقدار | 10 مل | 30 مل | 60 مل | 100 مل | 250 مل | 500 مل | 1000 مل |
|---|---|---|---|---|---|---|---|
| الحد الأقصى للتسوس | 20 | 18 | 14 | 12 | 8 | 5-6 | 3-4 |
Core Hardware Architecture of the EP80
إطار فولاذي كامل على الطراز الأوروبي
CNC-machined monolithic machine bed and platen mounts ensure parallelism between injection and blow clamping platens. Tie-bar surfaces are induction-hardened. The EP80 clamping force is 20-30% above equivalent-tonnage competitors due to the boosted pressurized clamping structure.
برغي وبرميل ثنائي المعدن
The plasticizing unit uses a bimetallic-lined barrel and a hardened alloy screw rated for glass-fiber and mineral-filled compounds. The EP80 screw diameter of 55 mm at 22:1 L/D delivers thorough homogenization with a 466 g shot capacity, covering the full range of bottle weights for this tonnage class.
صمام تناسبي للتحكم الهيدروليكي
يتم تنظيم كل من ضغط الحقن وضغط النفخ عبر صمامات هيدروليكية تناسبية مؤازرة. يتيح ذلك إمكانية التحكم في عملية الحقن على مراحل متعددة (سرعة التعبئة، والتحويل، وضغط التعبئة) للأشكال الأولية ذات الجدران الرقيقة، والتحكم الدقيق في معدل ضغط النفخ الذي يزيل عيوب التمدد الشعاعي الشائعة في أنظمة صمامات النفخ أحادية المرحلة.
نظام تحكم بشاشة لمس PLC
The EP80 control panel runs a full-color PLC touch-screen with parameter recipe storage. All process variables - temperatures, pressures, velocities, timings - are set and monitored from a single screen. Alarm history, production counters and fault codes are logged and displayed in real time.
نظام قنوات ساخنة مُحسَّن
صُممت مشعبة القنوات الساخنة لقالب الحقن لضمان تدفق خالٍ من المناطق الميتة، مما يقلل من انحراف الوزن بالجرام في جميع التجاويف. كما أن دقة التحكم في درجة الحرارة، التي تصل إلى ±1 درجة مئوية، تمنع تدهور المواد الحساسة للحرارة، وهي ضرورية للحفاظ على شفافية متسقة في العبوات الشفافة.
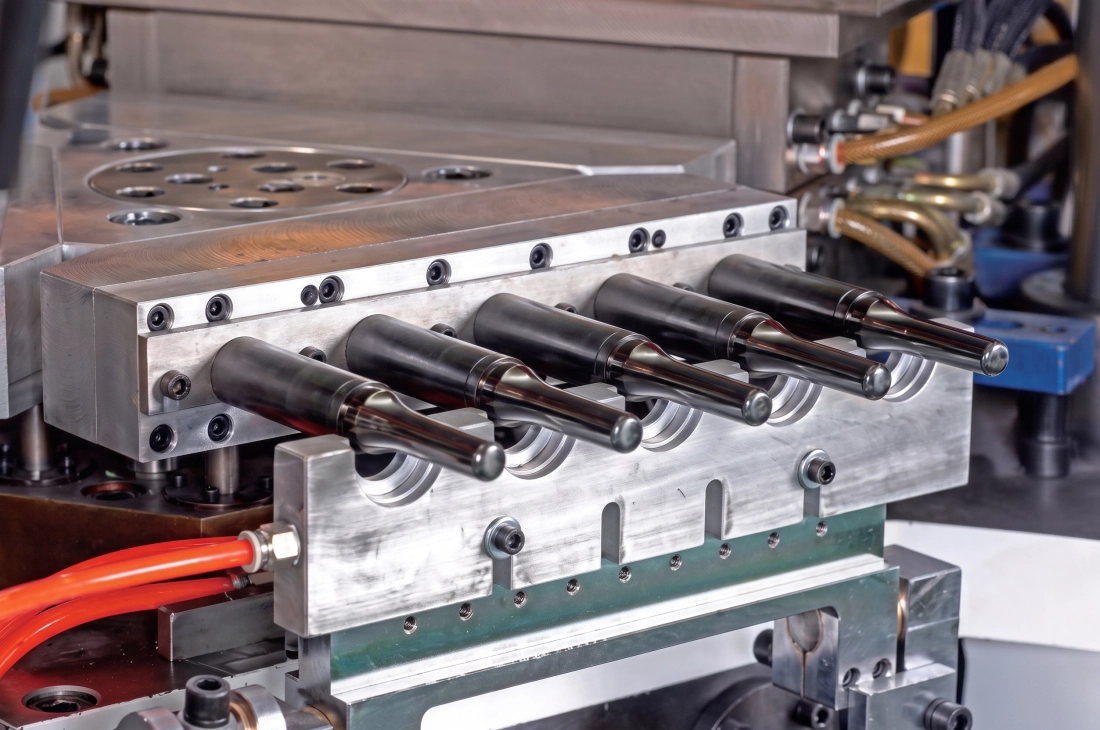
تصميم خاص لقضيب الصيد
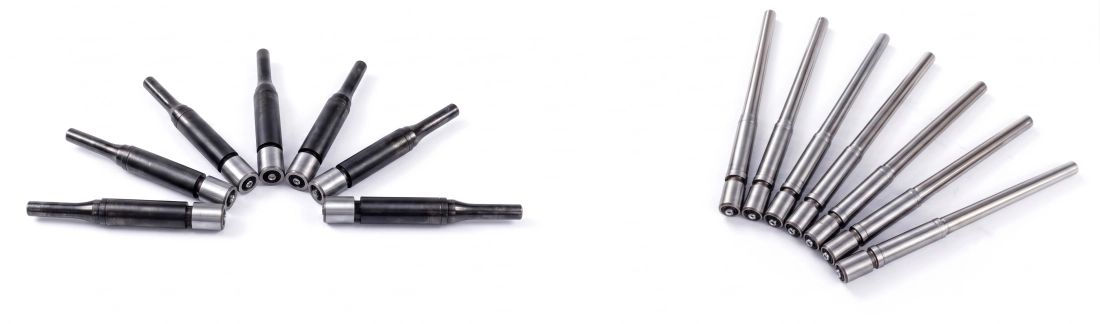
The mandrels (core rods) feature internal cooling channels that reduce core temperature between the injection and blow stations, accelerating the cooling phase. Fast-cycle mandrels enable the EP80 to achieve a 4 S dry cycle without sacrificing preform cooling uniformity or dimensional stability.
التشكيل بالنفخ بالحقن مقابل التشكيل بالنفخ بالبثق: لماذا تفوز شركة IBM في مجال الحاويات الدقيقة؟
Buyers evaluating hollow container equipment often compare IBM and EBM on capital cost alone. The EP80 is more than a machine choice - it is a process choice that determines your long-term production economics and the quality ceiling your facility can achieve. The comparison below reflects real production differences that directly affect your cost per thousand bottles and your ability to win pharmaceutical and cosmetic supply contracts.
| لا. | عنصر المقارنة | نفخ الحقن (IBM) | النفخ بالبثق (EBM) |
|---|---|---|---|
| 1 | اتساق وزن الزجاجة | تفاوت الوزن تقريبًا 1% | تفاوت الوزن تقريبًا 3% |
| 2 | توحيد سمك الجدار | سماكة جدار موحدة في جميع أنحاء الجدار | يتراوح سمك الجدار بين 10 و20% |
| 3 | عنق الزجاجة / الخيط | لا فلاش، ولا خط فرق على الرقبة | علامة قطع، قاعدة وعنق ضعيفان |
| 4 | التحدب القاعدي | تحدب إيجابي قوي، قاعدة مستقرة | ضعف التحدب نتيجة لحام القرص |
| 5 | نفايات المواد | صفر نفايات - لا فائض ولا خردة | 20-40% بقايا من فلاش الضغط |
| 6 | إمكانية الجدران فائقة الرقة | أقل ملاءمة للجدران الرقيقة جداً | يمكن تعديل سمك الجدار عبر وحدة التحكم |
| 7 | الحساسية البيئية | غير حساس للتغيرات المحيطة | يلزم إجراء تعديلات متكررة |
| 8 | عدد التجاويف والناتج | تجويف عالٍ، إنتاجية عالية، فوهة مسطحة | عدد أقل من التجاويف، إنتاج أقل، رقبة غير متساوية |
| 9 | عمر القالب وتكلفته | عمر طويل للقالب، مناسب لعمليات الإنتاج بكميات كبيرة ومستمرة | عمر أقصر للقالب، وتكلفة أولية أقل |
| 10 | بصمة أرضية | نظام متكامل صغير الحجم، بصمة صغيرة | معدات مساعدة إضافية، مساحة أرضية أكبر |
| 11 | تشكيل الحاويات البيضاوية | يُعد تشكيل الأشكال البيضاوية أكثر صعوبة | يسهل تشكيل الأشكال البيضاوية |
Application Fields and Container Types for the EP80
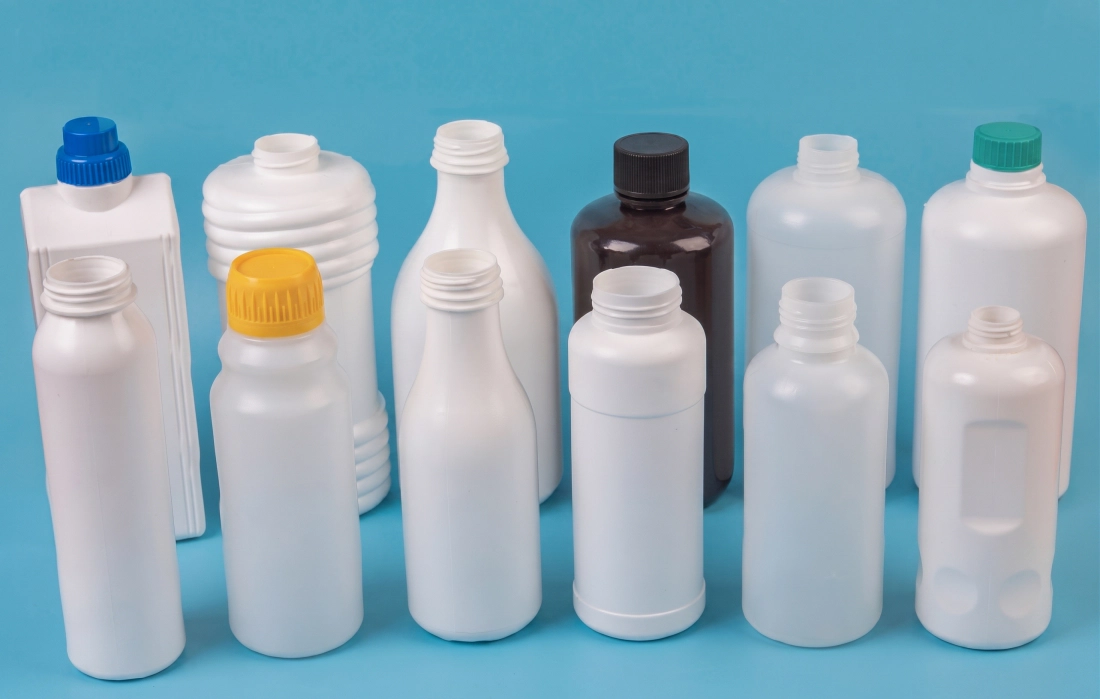
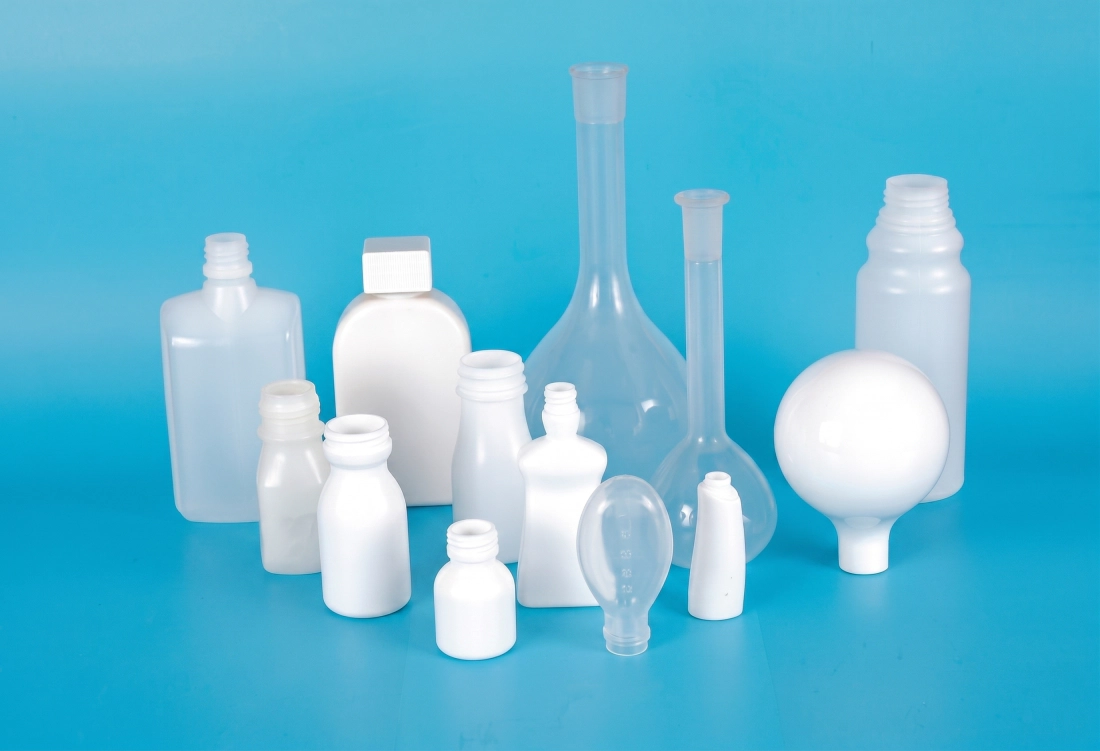
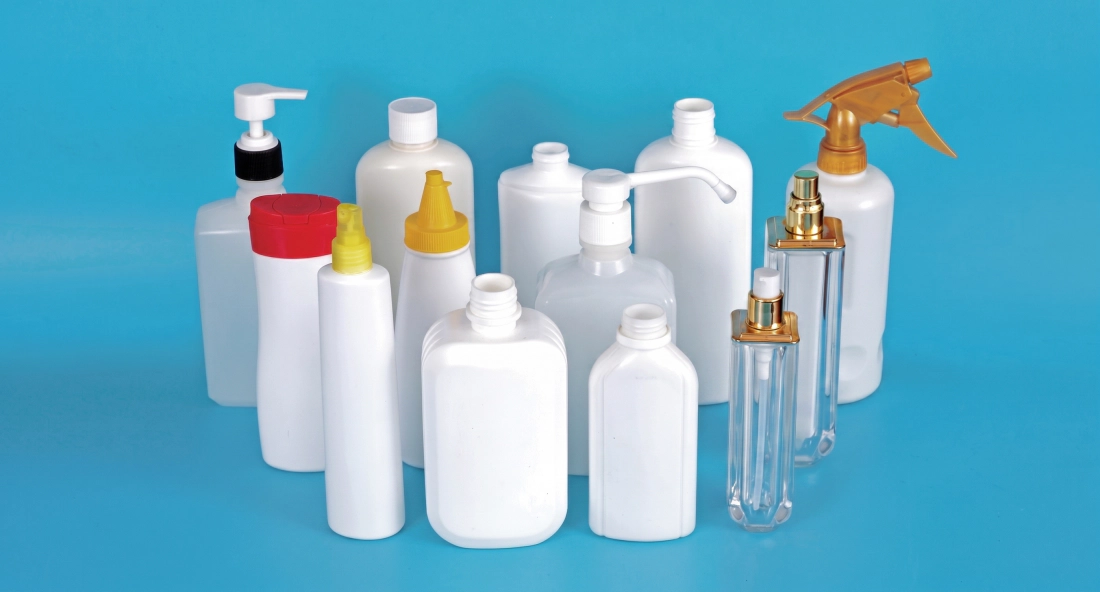
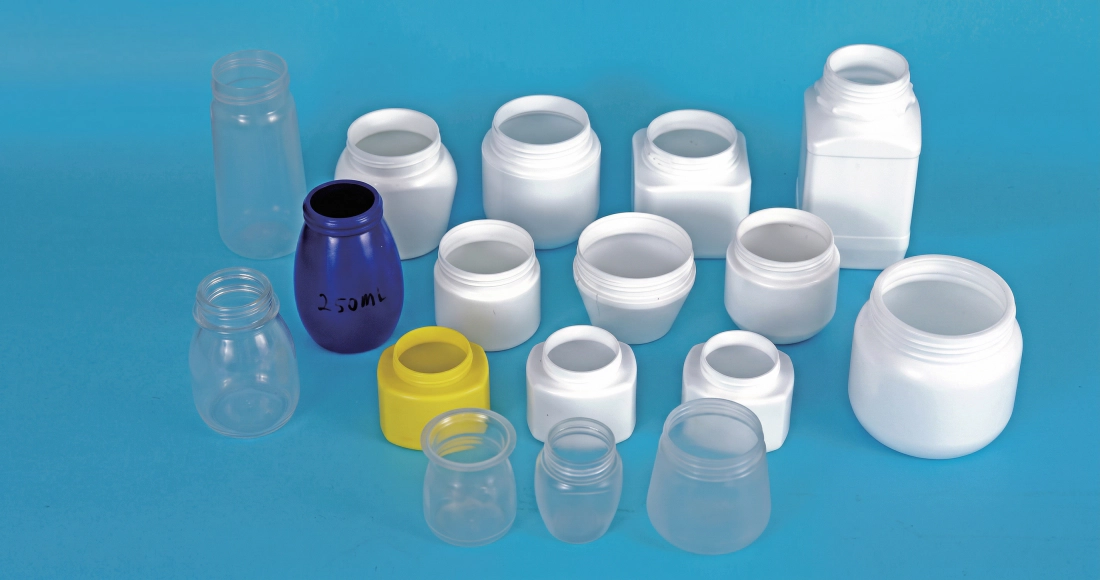
The EP80 is designed to produce bottles and containers from 1ml to the maximum volume for this model, covering the full range of primary packaging needs across four major market verticals. The table below shows the container types and industry segments where this معدات نفخ وحقن القوالب الأوتوماتيكية يحقق أعلى عائد تجاري له.
صناعة الأدوية
- زجاجات قطرات العين (بولي إيثيلين منخفض الكثافة، 5-30 مل)
- عبوات أقراص وكبسولات فموية (بولي إيثيلين عالي الكثافة، 30-500 مل)
- بخاخات الأنف وزجاجات المضخة (PP)
- زجاجات أدوية سائلة مزودة بأغطية مقاومة للأطفال
- قوارير اللقاحات والكواشف (LDPE، 1-20 مل)
- عبوات حبوب من البولي إيثيلين عالي الكثافة (HDPE) باللونين الكهرماني والأبيض، مطابقة لمعايير التصنيع الجيد (GMP).
صناعة مستحضرات التجميل
- زجاجات مزيل العرق الدوارة (بولي إيثيلين، 50-100 مل)
- أنابيب الماسكارا وزجاجات الفرشاة (بولي بروبيلين، 5-20 مل)
- زجاجات طلاء الأظافر (PS، 10-30 مل)
- زجاجات غسول وسيروم بمضخة (PCTG، 30-200 مل)
- برطمانات كريم واسعة الفوهة (PP/PS)
- زجاجات كريم الأساس والتونر
منتجات وأغذية الأطفال
- زجاجات إرضاع الأطفال (PP، PPSU، 150-300 مل)
- زجاجات قياس حليب الأطفال
- عبوات العسل والشراب (مصنوعة من البولي إيثيلين منخفض الكثافة)
- عبوات مشروبات خاصة صغيرة الحجم
- زجاجات عينات الزيت الصالح للأكل
- عبوات الزبادي ومنتجات الألبان
المواد الكيميائية والصناعية اليومية
- عبوات الشامبو والبلسم (HDPE/PP)
- موزعات معقم اليدين واللوشن
- زجاجات عينات سوائل السيارات
- زجاجات مركزات المواد الكيميائية الزراعية
- عبوات منتجات التنظيف
- زجاجات كواشف صناعية ذات أعناق دقيقة
Three-Station Rotary Indexing Precision: Engineering the 120-Degree Transfer
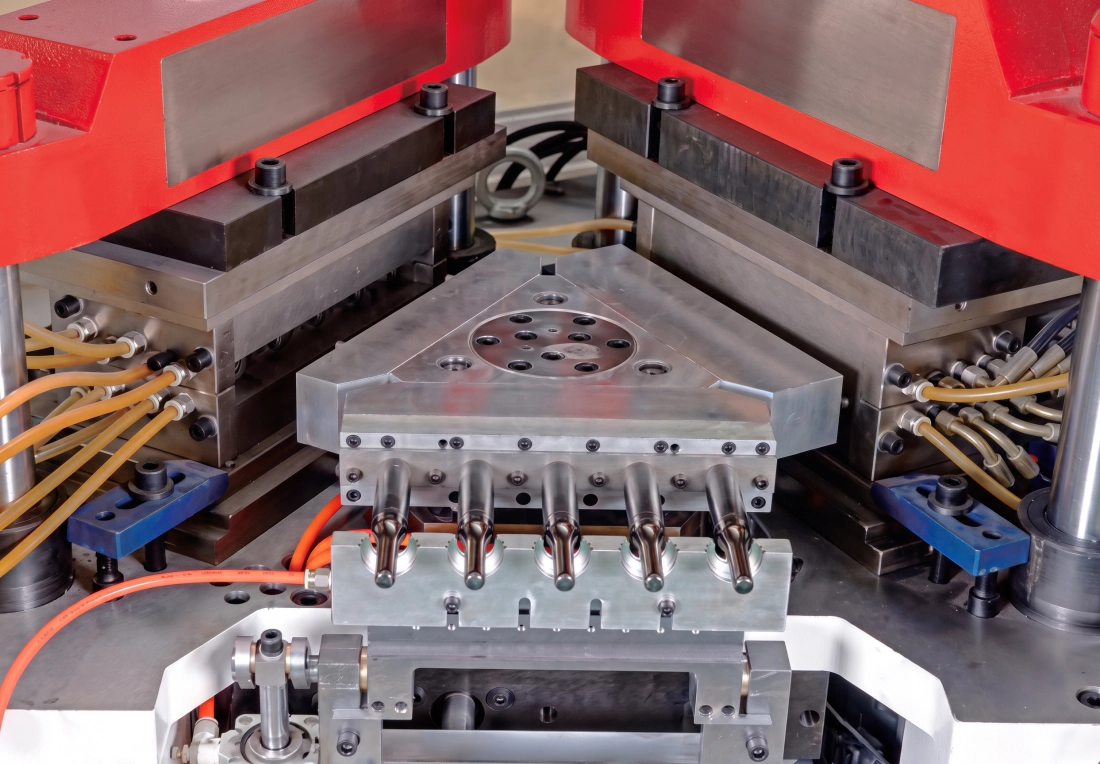
The heart of the one-step IBM process is the rotating turret that carries the mandrel array through three 120-degree stations simultaneously: injection, blow molding, and ejection. On the EP80, this critical mechanism uses a high-precision angle divider - a purpose-built indexing unit derived from machining center rotary table technology - that achieves positional repeatability better than 0.02 degrees per cycle.
Why does this matter? The mandrels, carrying the hot preform from the injection station to the blow station, must align with the blow mold cavities to within a few tenths of a millimeter. Any angular error means the preform enters the blow cavity off-center, resulting in uneven wall distribution, eccentricity of the bottle body, or worse - the mandrel strikes the cavity wall and causes tool damage. The standard angle divider on the EP80 ensures that even at production speeds of 4 seconds per cycle, the transfer is completed with hydraulic deceleration that eliminates mechanical shock to both the indexing mechanism and the mold.
The EP80 implements turret lift and rotation as synchronized motions - the turret rises to clear the mold parting line and rotates simultaneously, reducing the non-productive transfer time to an absolute minimum. The dual hydraulic circuit standard on this model means injection and clamping circuits operate independently, so clamping force build-up does not create pressure disturbance in the injection circuit during the holding phase. This separation also enables finer proportional valve control over blow pressure, critical when forming thin-walled LDPE bottles where even 0.05 MPa of excess blow pressure causes webbing or shoulder deformation.
Investment Return and Production Efficiency Analysis: Why Choose the EP80?
The acquisition cost of the EP80 must be evaluated against five measurable efficiency drivers that determine cost per thousand bottles and payback period. Purchasing engineers who evaluate only machine price - without these five factors - systematically undervalue the IBM platform and overestimate EBM economics for their target application.
1. صفر نفايات فلاش
لا تُنتج تقنية IBM أي مخلفات أو نفايات ناتجة عن خطوط الإنتاج. بينما تُنتج تقنية EBM ما بين 20 و401 طن من وزن الزجاجات كنفايات في كل دورة. وبإنتاج 200 طن من البولي بروبيلين سنويًا، توفر تقنية IBM الخالية من النفايات ما بين 40 و80 طنًا من الراتنج سنويًا. وبسعر 1500 دولار أمريكي للطن، يصل إجمالي التوفير في المواد الخام إلى ما بين 60,000 و120,000 دولار أمريكي سنويًا من آلة واحدة فقط.
2. لا يوجد عمل لإزالة الزوائد
EBM requires a secondary deflashing operation - either inline mechanical or manual - adding labor cost, a second machine footprint, and an additional quality failure point. IBM bottles from the EP80 come off the conveyor with zero post-processing required before filling or labeling, saving 1-3 operators per shift.
3. إنتاجية دورة التجفيف القصيرة
The EP80 achieves a 4 S dry cycle. With 14 cavities at 60ml, annual output at 6,000 hours run time exceeds 75.0 million bottles. This throughput concentration into a single compact machine reduces total asset investment per unit of capacity versus multi-machine EBM lines at equivalent output.
4. تغيير القوالب بسرعة
The injection mold and blow mold on the EP80 can be changed in 2-4 hours by a trained two-person team. Recipe recall from the PLC removes setup time entirely for repeat jobs. Facilities running 8-15 SKUs on a single EP80 achieve mold changeover frequency of 2-4 per week with total changeover downtime below 10% of available production hours.
البصمة البيئية وكفاءة استخدام المرافق
The EP80 footprint of 4.5x1.6x2 M consolidates injection, blow and ejection into a single machine envelope. Compare this to a two-machine EBM line (extruder plus blow machine, plus deflash press, plus conveyor) which typically occupies 3-4 times the floor area for equivalent throughput. Utility connections - compressed air at 0.7-1.2 MPa, cooling water at 4 M3/h flow, electrical connection at 55 KW total - are all single-point utilities, reducing installation complexity and ongoing maintenance overhead.
Factory building cost in pharmaceutical-grade cleanroom environments can reach 2,000-5,000 USD per square meter. The compact footprint of the EP80 directly reduces the cleanroom area required to produce a given volume of output - a capital benefit that does not appear in machine comparison tables but materially affects total project economics.
خصائص قوالب سلسلة EP من IBM ومعايير التصميم
- ■تصميم تجويف نشط وكتلة عنق تتميز تجاويف قوالب الحقن وكتل العنق بإمكانية التعديل المستقل، مما يسمح بضبط أبعاد جسم الأنبوب المُشكّل مسبقًا بدقة دون الحاجة إلى استبدال مجموعة القوالب بأكملها. صُممت ممرات الزيت والماء خصيصًا لتوزيع درجة الحرارة بشكل مستقر وسهولة الفك.
- ■أنواع الفولاذ الممتازة تُصنع أجسام قوالب الحقن من الفولاذ المقاوم للصدأ 4Cr13 أو من سبائك الفولاذ S136 عالية القوة المستوردة. يتميز الفولاذ S136 بلمعانه المصقول ومقاومته للتآكل، ويصل صلابته إلى 52 HRC. أما أجسام قوالب النفخ، فيمكن تصنيعها من سبائك المغنيسيوم والألومنيوم لتحقيق توصيل حراري فائق وتقليل كتلة القصور الذاتي في البرج الدوار.
- ■تصميم مُحسَّن للقنوات الساخنة والقوالب الأولية صُممت مشعبة القنوات الساخنة لتقليل تباين الوزن بالجرام عبر جميع التجاويف وتقليل تفاوت سماكة الجدار في جسم القالب الأولي. ويضمن تصميم المندريل توصيلًا موحدًا للهواء من أجل تمدد نفخ متسق وتبريد سريع.
- ■أبعاد دقيقة لخيط العنق والختم - يتم تشكيل الأقطار الداخلية والخارجية لفتحة الزجاجة، وخطوة السن اللولبي، وهندسة الحافة وفقًا لتفاوتات الرسم. معدل إحكام غلق الغطاء هو 100% في جميع عينات الإنتاج.
- ■لا يوجد وميض عند الرقبة والقاعدة - the IBM process geometry eliminates parting-line flash at the bottle mouth and pinch-weld flash at the base. Bottles exit the EP80 with no trimming required at either end.
- ■مقاييس اتساق المنتج - الحجم والوزن وموضع خط الفصل وسمك الجدار متسقة عبر جميع التجاويف وعبر دفعات الإنتاج، مما يتيح لعملاء صناعة الأدوية التحقق من صحة الإنتاج على أساس إحصائي لكل دفعة دون تكاليف فحص إضافية.
Equipment Selection Guide: Is the EP80 Right for Your Production Requirements?
Selecting the correct IBM tonnage requires calculating the intersection of three variables: preform weight, required cavity count, and target output per hour. Use this framework to confirm whether the EP80 is correctly sized for your application, or to understand what production parameters it can support.
الخطوة 1: حساب وزن القالب الأولي
Take the target bottle weight in grams (including the neck, body and base). Add 2-5% for process cushion. The EP80 injection weight of 466 g must be equal to or greater than (target preform weight x number of cavities). For example: a 5g preform at 8 cavities requires 40g shot weight, well within the 466 g capacity.
الخطوة الثانية: حساب عدد التجاويف المطلوبة
Target output (bottles/hour) divided by (3600 seconds / cycle time in seconds) gives required cavities. At a 4 S cycle and 10,000 bottles per hour target: 10,000 / (3600 / 4) = 12 cavities minimum. Cross-check against the cavity table above to confirm the EP80 can deliver this at your bottle volume.
الخطوة 3: التحقق من ملاءمة قالب التشكيل
The injection mould layout (cavity array footprint) must fit within the EP80 max platen size of 800x400 mm. Wide-bottle (diameter greater than 120mm) or tall-bottle (height greater than 220mm) applications exceed the EP80 mould envelope and require a larger model. Confirm your bottle OD and height before specifying cavity count.
الخطوة الرابعة: المادة وضغط الحقن
PP requires higher injection pressure and melt temperature than LDPE. PC and PETG require even higher barrel temperatures and longer residence-time plasticization. The EP80 hydraulic system pressure of 14 MPa and motor of 18.5+18.5 KW supports the injection forces needed for PP and engineering grade materials at the rated injection weight. Confirm your resin specification with the EVER POWER application team before ordering.
EVER POWER application engineers provide free pre-sales technical consultation to validate your container dimensions, material, cavity count and production target against EP80 specifications. Contact us with your bottle drawing and production brief for a written confirmation of suitability.
نظرة عامة على هيكل الآلة وإرشادات الصيانة
The EP80 is built around three core functional modules. Understanding their maintenance requirements is essential for sustaining the machine performance metrics - dry cycle, output rate, and product quality - over the full production life of the equipment.
الوحدة 1 - وحدة الحقن: البرغي، الأسطوانة، قناة التغذية الساخنة
تقوم وحدة الحقن بصهر البلاستيك وتوزيعه في تجويف القالب الأولي. الصيانة اليومية: التحقق من درجات حرارة الأسطوانة مقارنةً بالقيم المحددة، وفحص طرف البرغي وحلقة الفحص بحثًا عن مؤشرات التآكل، والتأكد من أن درجات حرارة منطقة القناة الساخنة لا تتجاوز درجتين مئويتين عن القيم المحددة قبل بدء التشغيل. الصيانة الأسبوعية: فحص حلقات عزل الأسطوانة، وفحص أختام أسطوانة الحقن بحثًا عن تسرب الزيت، وإزالة أي تلوث لوني من الإنتاج السابق. الصيانة الشهرية: فك وتنظيف حلقة الفحص ومجموعة طرف البرغي؛ وفحص شفرات البرغي بحثًا عن التآكل وقياس قطر تجويف الأسطوانة للتأكد من الخلوص. استبدل الأسطوانة إذا تجاوز الخلوص سماحية الشركة المصنعة لمنع تسرب المادة المنصهرة وعدم اتساق وزن الحقن.
إجراء التنظيف: عند تغيير الألوان من الداكنة إلى الفاتحة، أو من الراتنج الهندسي إلى الراتنج التجاري، استخدم مركب تنظيف تجاري عند درجة حرارة أعلى بعشر درجات من درجة حرارة المادة الجديدة. قم بتشغيل 5-10 دورات تنظيف قبل التبديل إلى المادة الجديدة. لا تترك الأسطوانة في وضع الخمول عند درجة حرارة التشغيل لأكثر من 20 دقيقة دون تنظيف، لأن التدهور الحراري أثناء فترات الخمول هو السبب الرئيسي لتلوث المادة ببقع سوداء عند إعادة التشغيل.
الوحدة 2 - وحدة التثبيت والفهرسة الدورانية
يتحمل نظام التثبيت وجهاز الفهرسة الدوار أعلى الأحمال الميكانيكية ويتطلبان دقة عالية في تحديد الموضع. يوميًا: ضع الشحم على أسطح قضبان الربط وقضبان توجيه الطاولة الدوارة وفقًا لجدول التشحيم (تحدد شركة إيفر باور نوع الشحم - لا تستخدم شحمًا متعدد الأغراض، فقد لا يحافظ على لزوجته عند درجة حرارة التشغيل). افحص أسطوانة التثبيت الهيدروليكية للتأكد من عدم وجود تسرب للزيت عند مانع تسرب القضيب. استمع لأي أصوات غير معتادة أثناء دوران الفهرسة - أي طقطقة معدنية أو تردد يشير إلى أن محمل التقسيم الزاوي يحتاج إلى فحص.
شهريًا: تحقق من توازي الألواح باستخدام مؤشر قياس عبر أربعة مواضع لقضيب الربط؛ يتطلب الانحراف الذي يزيد عن 0.05 مم إعادة ضبط الحشوات. تحقق من دقة موضع الفهرسة بوضع مؤشر قياس على سطح مرجعي على البرج والتأكد من تكرار نفس الموضع بدقة تصل إلى 0.02 مم بعد 100 دورة فهرسة متتالية. في حالة ملاحظة أي انحراف، اضبط المصد الميكانيكي أو اتصل بخدمة EVER POWER.
الوحدة 3 - النظام الهيدروليكي ودائرة التبريد
The hydraulic system is the energy backbone of the EP80. System pressure is set at 14 MPa. Daily: check hydraulic oil level in the tank sight glass, check oil temperature display (normal operating range 40-55 degrees Celsius; above 60 degrees indicates a cooling circuit problem or filter blockage), and inspect all visible hydraulic hose fittings for weeping. The oil filter indicator must be checked every 250 hours - a red indicator requires immediate filter element replacement, not deferral.
Cooling circuit: the EP80 requires clean, scale-free cooling water at 0.3-0.4 MPa pressure and 4 M3/h flow. Install a water treatment system upstream of the machine to prevent calcium scale buildup inside mold cooling channels. Scale buildup of just 1mm in a 6mm channel reduces cooling efficiency by over 30%, extending cycle times and reducing output. Flush cooling circuits with a descaling solution annually. Chiller water quality must be neutral pH (6.5-7.5) and contain an anti-corrosion inhibitor compatible with copper and aluminum alloy mold materials.
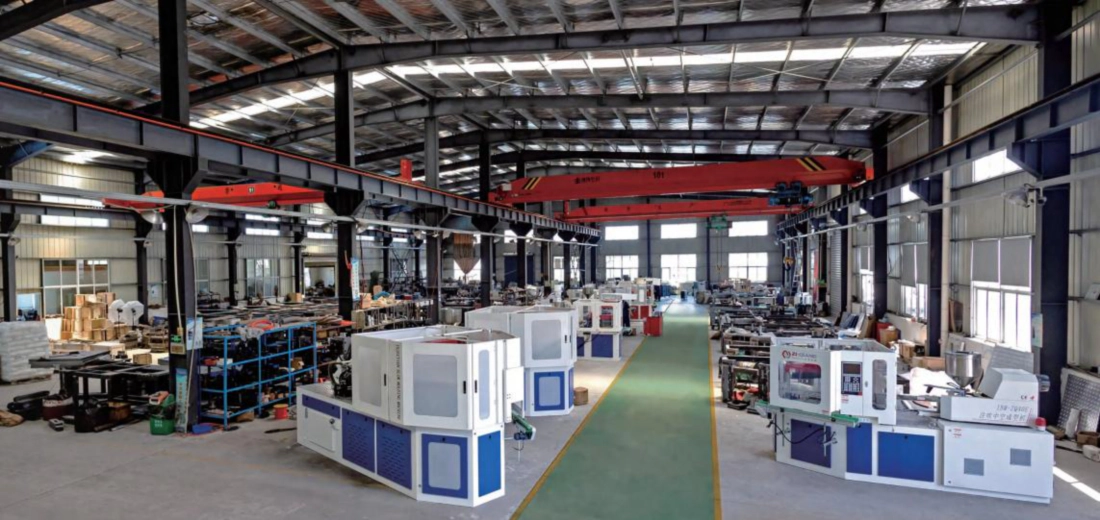
حلول متكاملة وخدمات تخصيص من إيفر باور
EVER POWER supplies the EP80 as either a standalone machine or as the centerpiece of a complete turnkey bottle production line. For customers setting up a new facility or expanding into a new container product line, the turnkey approach eliminates the integration risk that comes from sourcing the IBM machine, molds, auxiliaries, and downstream equipment from separate vendors.
تصميم وتصنيع القوالب
يقوم مهندسو إيفر باور بتطوير مجموعات قوالب الحقن والنفخ بناءً على رسومات زجاجات العملاء أو ملفات ثلاثية الأبعاد. قوالب متعددة التجاويف ذات قنوات ساخنة مصنوعة من فولاذ S136 أو 4Cr13. قوالب نموذجية أحادية التجويف للتحقق من صحة العبوات قبل البدء في تصنيع أدوات الإنتاج ذات التجاويف المتعددة. تُجرى تجارب القوالب من المستوى الأول (T0) في المصنع قبل الشحن.
تكامل المعدات المساعدة
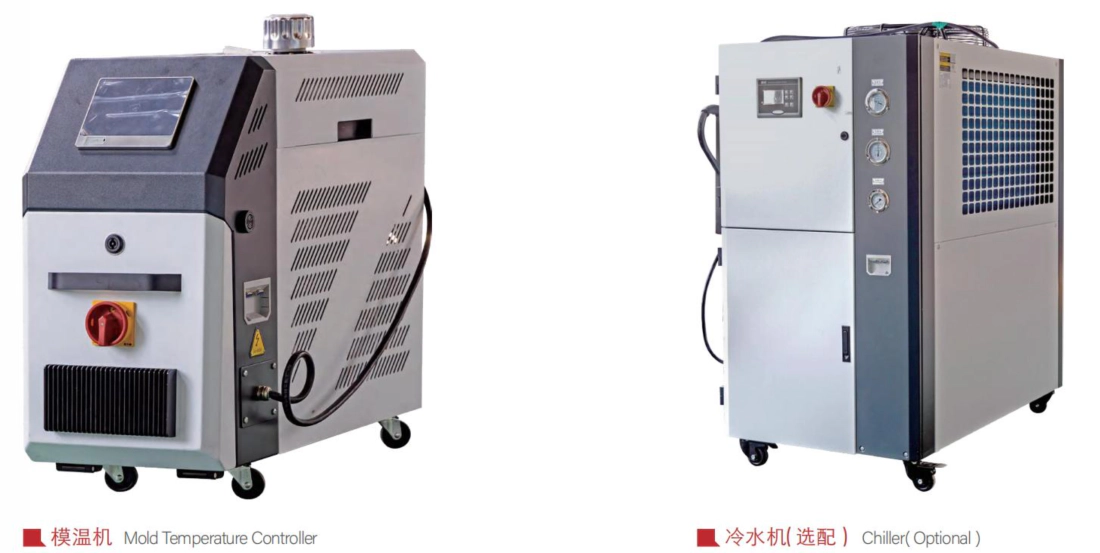
The EVER POWER turnkey line includes: screw air compressor, air tank and air dryer, mold temperature controller, industrial chiller, auto loader, conveyor belt, screen printing and labeling system, washing and drying line, and automatic filling and capping machines. All auxiliary equipment is specified and pre-integrated to match the EP80 output rate.
أنظمة الجودة في المراحل اللاحقة
Optional inline bottle visual inspection machine (machine vision system for flash, deformation and contamination detection), automatic leak tester, automatic packing machine, and carton erector. For pharmaceutical lines, 100% inline leak testing and vision inspection are available as integrated modules matched to the EP80 conveyor output speed.
تكوين غرف التنظيف وفقًا لممارسات التصنيع الجيدة (GMP)
بالنسبة لعملاء صناعة الأدوية الذين يحتاجون إلى إنتاج وفقًا لمعايير GMP، تقدم EVER POWER تخصيصًا للآلات يشمل: نظام تزييت مغلق لمنع تلوث منطقة المنتج، وحاويات أمان من الفولاذ المقاوم للصدأ، وحاوية آلة مزودة بمرشح HEPA للتوافق مع غرف التنظيف من الفئة 100000، ودعم توثيق بروتوكولات تأهيل المعدات (IQ/OQ/PQ).
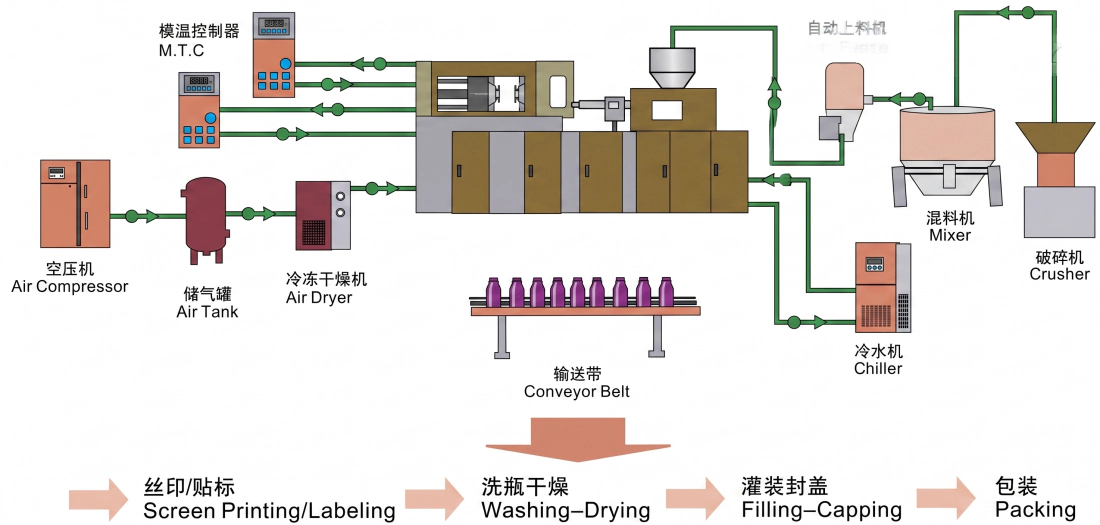
Auxiliary Equipment Available with the EP80
معايير مراقبة الجودة والتصنيع
التصنيع باستخدام الحاسوب للمكونات الحيوية
تُصنّع قاعدة الماكينة، وألواح التثبيت، وجميع الأسطح الدقيقة باستخدام آلات CNC في عملية واحدة لضمان الدقة الهندسية. ويتم التحقق من توازي الألواح بواسطة قياس الليزر بدقة تصل إلى 0.02 مم. كما تُصقل ثقوب قضبان الربط وفقًا لتفاوت H7 لضمان تركيب المحامل دون أي تداخل.
تقوية قضبان الربط بالحث
تخضع قضبان الربط لعملية تقوية بالحث عالي التردد لتصل صلابة سطحها إلى 52-58 HRC، تليها عملية طحن دقيقة. توفر هذه المعالجة السطحية مقاومة للتآكل الناتج عن الاحتكاك الانزلاقي المتكرر لألواح التثبيت على مدى ملايين الدورات دون حدوث احتكاك أو تآكل سطحي.
نظافة الدائرة الهيدروليكية
تُغسل جميع الدوائر الهيدروليكية، وتُختبر تحت الضغط، ويُتحقق من عدد الجسيمات قبل التجميع. ويُحافظ على نظافة الزيت الهيدروليكي وفقًا لمعيار ISO 4406 الفئة 17/15/12 كحد أدنى. تتطلب حساسية صمامات التحكم التناسبي والمؤازر للتلوث هذا المستوى من النظافة لمنع التصاق بكرة الصمام والتحكم في الانحراف.
اختبار تشغيل المصنع لمدة 72 ساعة
Every EP80 undergoes a minimum 72-hour continuous loaded run test at the factory before shipment. During this period, production output samples are measured for weight consistency, wall thickness uniformity, and dimensional accuracy. Any parameter outside specification triggers a hold and corrective action before the machine is cleared for delivery.
الامتثال لمعايير السلامة الأوروبية CE
The EP80 is CE-marked in compliance with EU Machinery Directive requirements. Safety features include: interlocked safety doors with hydraulic circuit interrupt, light curtain protection at the operator access zone, emergency stop at all operator positions, and two-hand operator control for manual mold setting. CE documentation is provided with every machine.
خدمة ما بعد البيع والدعم الفني
التركيب والتشغيل
يتولى كبار مهندسي شركة إيفر باور مسؤولية التركيب والتشغيل واختبارات القبول. ويبقى المهندس في الموقع حتى تصل الآلة إلى حالة إنتاج مستقرة، ويتم تدريب جميع المشغلين على تشغيل الآلة وتغيير القوالب والصيانة الدورية. ويتم الاتفاق على معايير القبول قبل الشحن وتوثيقها في تقرير التشغيل.
برنامج الصيانة الوقائية
تُقدّم شركة إيفر باور خدمة تذكير بالصيانة الدورية لجميع الآلات قيد التشغيل. يشمل جدول الصيانة مهام الصيانة اليومية والأسبوعية والشهرية والسنوية. تمنع الصيانة الاستباقية الأعطال غير المخطط لها وتقلل الحاجة إلى شحنات قطع الغيار الطارئة باهظة الثمن. يُفيد العملاء الذين يلتزمون بجدول الصيانة الوقائية باستمرار بأن جاهزية الآلات تتجاوز 95%.
خط خدمة متاح على مدار الساعة طوال أيام الأسبوع
خط خدمة عملاء إيفر باور متاح على مدار الساعة طوال أيام الأسبوع. في حال حدوث أعطال إنتاجية طارئة، يُرجى الاتصال أو إرسال رسالة إلى خط الخدمة، وسيقوم مهندس مؤهل بالرد خلال ساعتين لتشخيص المشكلة عن بُعد. إذا تطلب الأمر خدمة ميدانية، تُرسل إيفر باور فنيًا بأسرع وقت ممكن لموقعك.
مخزون قطع الغيار
EVER POWER maintains a comprehensive spare parts inventory for all EP80 components including hydraulic seals, proportional valve cartridges, heating bands, temperature sensors, drive belts and electrical components. Parts can be shipped globally within 48 hours for items in stock. Critical fast-wear items are available for customer-held local inventory based on EVER POWER recommendations.
برامج التدريب التقني
إلى جانب التدريب القياسي على التركيب، تقدم إيفر باور وحدات تدريبية متخصصة تشمل: تشغيل الآلات، وتحسين عملية القوالب، وتغيير القوالب وإعدادها، وصيانة النظام الهيدروليكي، واستكشاف أخطاء العمليات وإصلاحها لمواد محددة مثل البولي بروبيلين، والبولي إيثيلين منخفض الكثافة، والبولي كربونات تيريفثالات. ويمكن إجراء التدريب في مصنع إيفر باور أو في موقع العميل.
Frequently Asked Questions - EVER POWER EP80
What materials can the EP80 process?
The EP80 is compatible with HDPE, LDPE, PP, PS (including lactic acid bacteria grade transparent PS), ABS, EVA, bio-based corn material, PCTG, and similar thermoplastics. For engineering resins such as PC, PETG and Tritan, the screw L/D of 22:1 and the 4+N heating zones provide the residence time and temperature profile needed for thorough, degradation-free plasticization. Confirm your resin grade with EVER POWER application engineering before ordering.
Can the EP80 be used for pharmaceutical GMP production?
Yes. The EP80 can be configured for pharmaceutical GMP production environments. Key features supporting GMP include: the one-step process eliminates inter-machine bottle transfer that introduces contamination risk in two-stage systems; the closed lubrication system prevents lubricant contamination of the product zone; and the machine can be specified with a stainless steel safety enclosure suitable for cleanroom installation. EVER POWER can provide equipment documentation to support IQ/OQ/PQ qualification processes for pharmaceutical facility validation.
How long does mould changeover take on the EP80?
A trained two-person team can complete a full mold changeover (injection mold, blow mold, and mandrel set) on the EP80 in approximately 2-4 hours, depending on the mold design and the changeover frequency experience of the team. PLC recipe recall eliminates parameter re-entry time for repeat mold sets. Facilities that invest in quick-release clamping plates for the mold base can reduce changeover to under 2 hours.
What certifications does the EP80 carry?
The EP80 is CE-marked for the European market. The machine design complies with EU Machinery Directive safety requirements including interlocked guards, emergency stop systems, and electrical safety standards. EVER POWER is an ISO-certified manufacturer. Machine documentation is provided in English and can be supplied in other languages upon request for export markets.
What is the lead time for the EP80 and an associated mould set?
Standard machine lead time for the EP80 is 45-75 days from order confirmation and deposit receipt, depending on production schedule at time of order. Mold sets are typically supplied in 60-90 days from final confirmation of bottle drawings and material specification. The machine and mold sets can be scheduled to arrive simultaneously for a coordinated installation. Contact EVER POWER for current lead time at time of inquiry.
Ready to Specify the EVER POWER EP80 for Your Production Line?
أرسل رسم الزجاجة، والحجم المستهدف، ومواصفات المواد، والإنتاج المطلوب في الساعة إلى فريق هندسة التطبيقات لدينا. سنؤكد لك عدد التجاويف الصحيح وتكوين الآلة كتابيًا، وسنقدم لك عرضًا تجاريًا مفصلًا خلال ثلاثة أيام عمل.
معلومات إضافية
| تم التعديل | بواسطة hyw |
|---|
منتجات ذات صلة
-
ماكينة نفخ وحقن القوالب الكهربائية عالية السرعة EP60HE، دورة 2.5 ثانية بدون نظام هيدروليكي
-
ماكينة حقن ونفخ القوالب شديدة التحمل EP135 بقوة 1350 كيلو نيوتن، ذات تجويف عالٍ، لتصنيع عبوات مستحضرات التجميل والأدوية.
-
ماكينة حقن ونفخ القوالب الصناعية EP110 بقوة 1100 كيلو نيوتن، أوتوماتيكية، من إنتاج شركة IBM، لتصنيع الزجاجات ذات الأحجام الكبيرة.
-
ماكينة حقن ونفخ أوتوماتيكية بخطوة واحدة EP60 بقوة 600 كيلو نيوتن، مصنع عبوات مستحضرات التجميل الصيدلانية
-
ماكينة نفخ وحقن أوتوماتيكية بخطوة واحدة EP40 بقوة 400 كيلو نيوتن لزجاجات مستحضرات التجميل والأدوية، حاصلة على شهادتي CE وISO


