
روزانہ کیمیکلز کے لیے دو اسٹیج PET اسٹریچ بلو مولڈنگ مشین - 2000 سے 4600 BPH
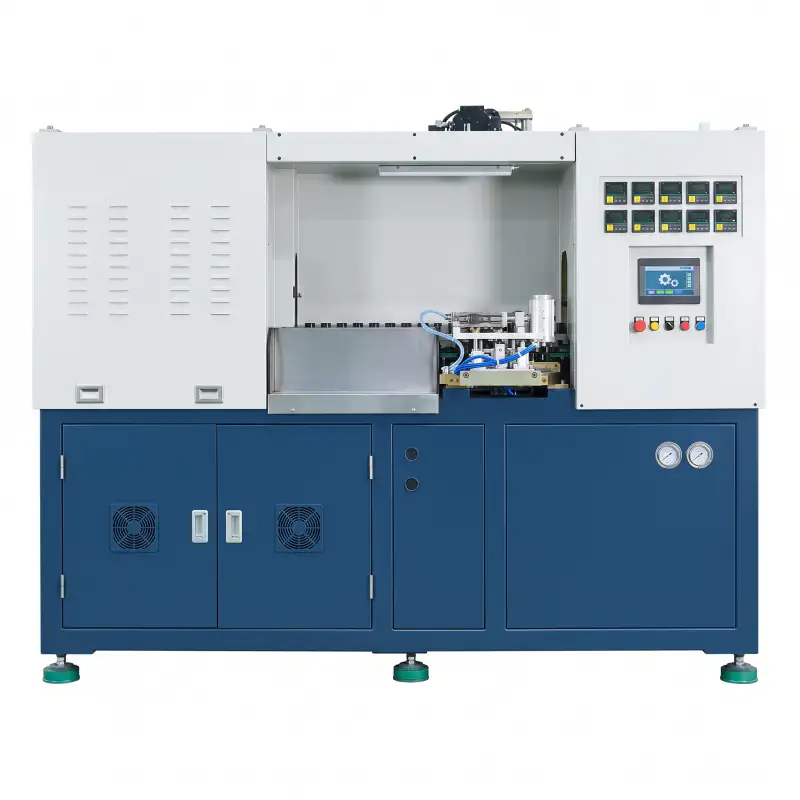
Are you searching for a trusted two stage blow molding machine manufacturer? Our automatic PET bottle blowing machine is engineered for daily chemicals and cosmetics, delivering high-efficiency production from 2000 to 4600 BPH. Featuring servo-driven precision, high-pressure air recovery, and CE-certified safety, this reheat stretch blow molder ensures superior bottle clarity and optimal ROI for your manufacturing line.
Two-Stage Reheat Stretch Blow Molding Machine
EP Daily Chemicals & Cosmetic Bottle Series Blow Molding Machine
Engineered for high-precision PET and PETG cosmetic container production, the EP daily chemicals and cosmetic series two-stage stretch blow molding machine delivers stable multi-cavity output across a wide range of bottle geometries — from 500 ml narrow-neck lotion bottles to 15,000 ml wide-body containers. International brand servo motors, reducers, electrical components and control systems combine to produce reliable, energy-efficient, and consistently dimensioned packaging for daily chemical, personal care, and cosmetic brands.
2 / 3 / 4 Cavities
PET / PETG
Servo Drive System
Neck Dia. Up to 168 mm
پروڈکٹ کا جائزہ
The EP cosmetic bottle series adopts the two-stage reheat stretch blow molding process — the globally dominant method for high-volume PET container manufacturing. By separating preform injection from the blowing station entirely, the process enables full optimization of preform wall distribution independently of blowing speed, resulting in thinner, lighter, and more optically uniform bottles than single-stage processes can achieve at comparable throughput.
This machine is particularly well-suited to cosmetic and daily chemical containers where bottle geometry complexity is high — oval cross-sections, flat-panel surfaces, asymmetric shoulder profiles, and wide-mouth openings up to 168 mm neck diameter. The independent servo-driven stretching rod delivers precise biaxial molecular orientation, imparting the clarity, drop resistance, and barrier performance that cosmetic packaging demands.
The series covers a broad output range, from 900 BPH on large-volume wide-body containers up to 4,800 BPH on compact 4-cavity configurations, giving procurement teams a single qualified supplier for an entire packaging portfolio spanning shampoo, body lotion, household cleaner, skincare, and industrial daily chemical formats.
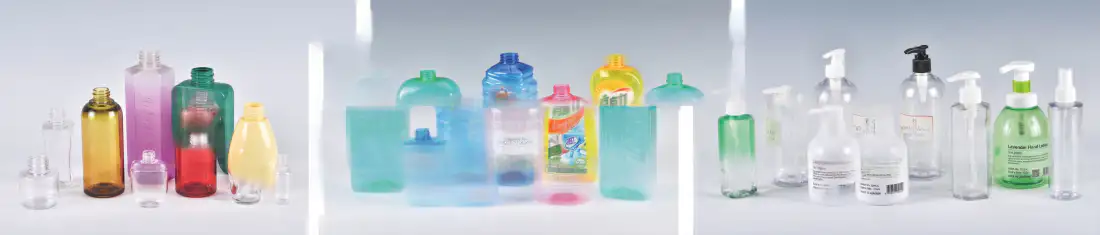
Two-Stage Reheat Blow Process — How It Works
PET/PETG preforms are auto-fed onto rotating mandrel carriers and conveyed into the infrared oven without manual handling.
Multi-zone IR lamps heat preforms to precise orientation temperature. Per-zone tuning enables wall distribution control on asymmetric bottle bodies.
Servo rod extends axially at controlled speed and force, stretching the preform to full container height and initiating biaxial molecular orientation.
Up to 35 kg/cm² blowing pressure expands the preform radially against chilled mold walls, locking in final bottle geometry with high surface gloss.
Finished bottles eject automatically and move downstream for labeling or filling. No operator contact at the blowing station throughout the production cycle.
تکنیکی وضاحتیں
Swipe horizontally on mobile to view all model columns.
| پیرامیٹر | یونٹ | EP.AS-2C114.3 | EP.AS-4C76.2 | EP.ES-2C100 | EP.ES-2C114.3 | EP.ES-2C130 | EP.ES-2C150 | EP.ES-2C200 | EP.ES-2C260 | EP.ES-3C76 | EP.ES-3C114 | EP.ES-4C76 | EP.ES-4C100 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Molding Unit | |||||||||||||
| Clamping Stroke | ملی میٹر | 122 | 100 | 110 | 132 | 160 | 190 | 215 | 275 | 100 | 133 | 100 | 128 |
| Mold-Open Distance | ملی میٹر | 302 | 280 | 280 | 312 | 360 | 440 | 499 | 635 | 300 | 363 | 300 | 328 |
| Mold-Close Distance | ملی میٹر | 180 | 180 | 170 | 180 | 200 | 250 | 284 | 360 | 200 | 230 | 200 | 200 |
| Stretching Stroke | ملی میٹر | 400 | 350 | 350 | 400 | 350 | 450 | 500 | 550 | 240 | 350/450 | 350 | 350 |
| Preform Holder | - | 48 | 96 | 60 | 60 | 60 | 60 | 50 | 42 | 72 | 74 | 96 | 92 |
| cavities | - | 2 | 4 | 2 | 2 | 2 | 2 | 2 | 2 | 3 | 3 | 4 | 4 |
| Container Specifications | |||||||||||||
| Max. Container Volume | ملی لیٹر | 1,000 | 500 | 500 | 1,000 | 1,500 | 2,500 | 5,000 | 15,000 | 700 | 1,500 | 700 | 800 |
| Max. Neck Diameter | ملی میٹر | 88 | 48 | 68 | 88 | 110 | 110 | 138 | 168 | 18–38 | 40 | 48 | 68 |
| Max. Container Diameter | ملی میٹر | 94 | 65 | 80 | 94 | 110 | 130 | 180 | 240 | 68 | 95 | 68 | 80 |
| Max. Container Height | ملی میٹر | 260 | 250 | 200 | 260 | 250 | 250 | 250 | 450 | 240 | 250/330 | 240 | 250 |
| Theoretical Output | BPH | 2,000 | 4,000 | 2,400 | 2,000 | 1,800 | 1,800 | 1,600 | 900 | 3,000 | 2,400 | 4,800 | 4,600 |
| Electrical System | |||||||||||||
| Max. Heating Power | kW | 45 | 33 | 34 | 50 | 42.5 | 42.5 | 85 | 85 | 40 | 40 | 40 | 62.5 |
| Common Heating Power | kW | 20 | 17 | 8–12 | 16 | 8–13 | 18 | 35 | 35 | 18 | 18 | 18 | 21 |
| Air System | |||||||||||||
| Operating Pressure | kg/cm² | 7 | 7 | 7 | 7 | 7 | 7 | 7 | 7 | 7 | 7 | 7 | 7 |
| Low Pressure Air Consumption | ltr/min | 600 | 600 | 600 | 600 | 600 | 600 | 600 | 1,200 | 1,500 | 1,500 | 800 | 800 |
| Blowing Pressure | kg/cm² | 35 | 35 | 26–35 | 35 | 26–35 | 26–35 | 30 | 35 | 35 | 35 | 35 | 35 |
| High Pressure Air Consumption | ltr/min | 1,600 | 4,000 | 1,000–1,400 | 1,000 | 1,000–1,500 | 1,000–1,500 | 6,000 | 16,000 | 2,400 | 3,200 | 3,900 | 4,000 |
| High Pressure Operating | kg/cm² | 6 | 5–6 | 5–6 | 6 | 5–6 | 5–6 | 5–6 | 5–6 | 5–6 | 5–6 | 5–6 | 5–6 |
| Cooling Water | |||||||||||||
| Temperature | °C | 8–12 | 8–10 | 8–10 | 8–12 | 8–10 | 8–10 | 8–12 | 8–10 | 8–12 | 8–12 | 8–12 | 8–12 |
| Flow Rate | ltr/min | 30 | 40 | 30 | 30 | 30 | 30 | 91.4 | 50 | 30 | 30 | 30 | 30 |
| مشین | |||||||||||||
| Size L x W x H | ملی میٹر | 2660x1660x2150 | 3370x1850x2100 | 2900x1525x1930 | 3220x1660x2010 | 3600x1800x1980 | 4290x1800x2220 | 4300x2100x2500 | 5570x2090x2500 | 2850x1850x2180 | 3240x1800x2000 | 3290x1850x2260 | 4170x1930x2340 |
| مشین کا وزن | کلو | 2,600 | 4,000 | 2,000 | 3,000 | 3,000 | 3,500 | 4,500 | 7,500 | 3,500 | 4,000 | 3,500 | 4,000 |
Core Hardware Features
Independent zone temperature control from preform body to neck finish. Critical for asymmetric cosmetic bottle profiles where uneven heating causes wall thinning and visual defects.
Servo motors and reducers on stretching, clamping, and transfer systems deliver precise torque and position control, reducing cycle time variation and unplanned downtime across multi-shift production.
Neck diameters from 18 mm up to 168 mm across the model range. The EP.ES-2C260 handles wide-body containers up to 15,000 ml with 168 mm necks — formats most two-stage machines cannot address.
High-strength aluminum alloy molds machined on 5-axis CNC centers. Dimensional repeatability within ±0.05 mm maintains cosmetic-grade surface quality and weight consistency across full production runs.
Industrial PLC with color HMI stores multiple bottle format recipes. Operators reload a saved parameter set in minutes — significantly reducing format-change downtime on multi-SKU cosmetic production lines.
Full safety door interlocks on all access panels, compliant with CE mechanical safety directives. Emergency stop circuits are hardwired independently of PLC logic for fail-safe shutdown.
rPET and PETG Processing Capability
Global cosmetic and personal care brands increasingly mandate recycled content targets — 25%, 50%, or 100% rPET — in their packaging specifications. The EP daily chemicals series accommodates rPET blends across this full range, subject to upstream preform IV management.
Recycled PET typically carries lower and more variable intrinsic viscosity (IV) than virgin resin, narrowing the orientation temperature window and reducing melt strength during blowing. The EP series addresses this through three engineering provisions:
- Extended oven dwell time programming — independent oven speed and per-lamp intensity adjustment compensates for rPET batch-to-batch IV variation without overheating the neck finish.
- 35 kg/cm² blowing pressure — maximum cavity-fill capability ensures complete bottle formation even when rPET material has reduced melt strength at orientation temperature.
- PETG compatibility without hardware modification — for brands requiring higher chemical resistance or elevated clarity in premium cosmetic containers, PETG runs on the same machine without tooling changes.
rPET processing guideline: recommended IV 0.72–0.84 dL/g, moisture below 50 ppm before blowing. Preform drying at 160°C for 4–6 hours is required prior to production.
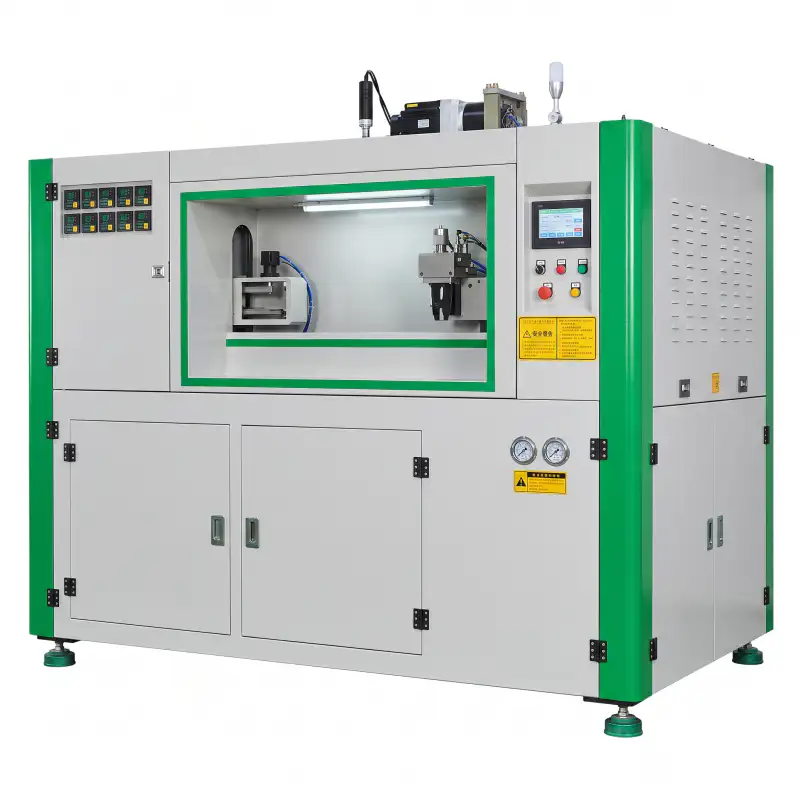
Applicable Container Types
200 ml – 1,000 ml oval and round bottles with varied neck finishes for personal care filling lines.
Asymmetric PETG cosmetic bottles demanding high surface gloss and precise wall thickness for premium brand packaging.
Trigger-pump neck format containers and detergent bottles in PET with ergonomic grip geometry.
Up to 168 mm neck diameter — specialty cosmetic cream jars and wide-body containers unreachable by most two-stage machines.
EP.ES-2C260 handles up to 15,000 ml — large daily chemical storage and industrial-use PET packaging.
Two-Stage vs One-Stage Process Comparison
| Factor | Two-Stage SBM (EP Series) | One-Stage IBM / ISBM |
|---|---|---|
| آؤٹ پٹ کی صلاحیت | Up to 4,800 BPH (4-cavity) | Typically 500 – 2,500 BPH |
| Preform Sourcing | Separate supply — global preform market available | Inline injection only — no external preform flexibility |
| Bottle Shape Flexibility | Oval, asymmetric, flat-panel, wide-mouth supported | Best suited to symmetrical round profiles |
| Mold Investment | Lower — aluminum blow mold only | Higher — injection and blow tooling combined |
| rPET Compatibility | High — IV-managed preforms process well | Limited by inline injection process constraints |
| Best Application | High-volume cosmetic, daily chemical, specialty containers | Medical, pharma, small-batch special-shaped bottles |
Production Efficiency & Cost Analysis
The EP.ES-4C76 at 4,800 BPH theoretical output, running 20 hours per day at 85% efficiency, delivers approximately 81,600 bottles — sufficient to supply a mid-scale cosmetic filling line at minimal incremental labor per unit produced.
Common heating power for 4-cavity models runs 18–21 kW at 4,600–4,800 BPH, placing energy cost below 4 kWh per 1,000 bottles — a benchmark that materially undercuts less efficient single-stage alternatives at equivalent output.
A single EP machine handles a cosmetic brand portfolio spanning 200 ml serum bottles to 1,500 ml shampoo containers. PLC recipe recall and mold changeover are the only reconfigurations needed — reducing total capital investment versus multiple dedicated format lines.
Turnkey Supply Scope & Quality Assurance
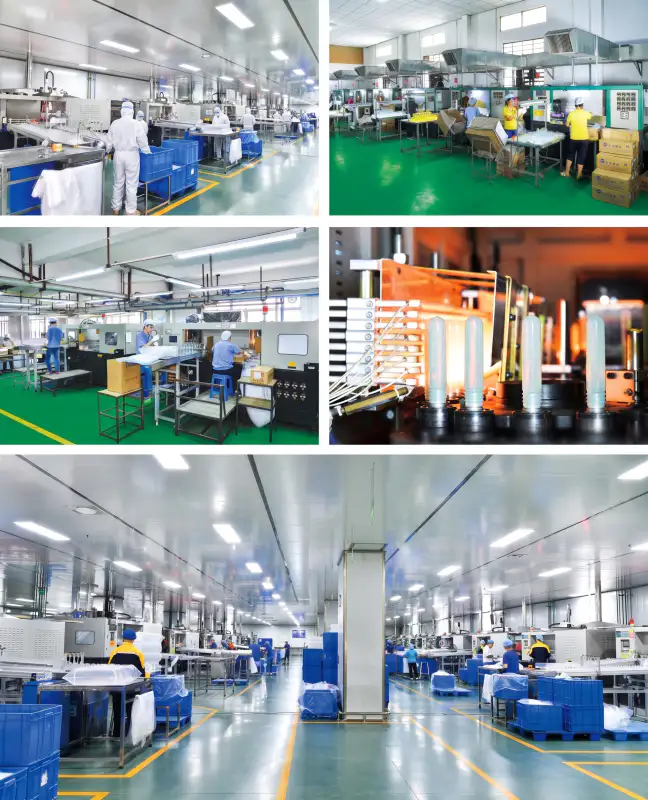
Every EP two-stage blow molding machine undergoes a 72-hour continuous production trial run before shipment. Output rate, heating consistency, blowing pressure stability, and cycle time repeatability are all logged against specification tolerances. Machines that do not meet rated performance are held for engineering rectification before release.
As a full-chain supplier, EVER POWER can deliver the complete production package alongside the blowing machine:
- Custom blow molds in aluminum alloy, 3D-designed to customer bottle drawings
- Matched preform injection molds in imported 2316 tool steel
- High-pressure and low-pressure industrial air compressors
- Industrial chillers sized to machine cooling water demand
- Preform dehumidifying dryers and auto-loaders
- On-site installation, commissioning, and operator training by factory-trained engineers
سامان کے انتخاب کی گائیڈ
Selecting the correct EP model requires matching four variables: target bottle volume, neck diameter, required BPH, and preform stretching height.
Volume and Neck Diameter
Containers under 1,000 ml with neck diameters to 88 mm start with the EP.AS-2C114.3 or EP.ES-2C114.3. Wide-mouth formats above 130 mm neck require the EP.ES-2C200 or larger. Containers to 15,000 ml require the EP.ES-2C260.
Cavities and BPH Target
2-cavity models cover 1,600–2,400 BPH. 3-cavity adds approximately 50% capacity. 4-cavity configurations reach 4,600–4,800 BPH for maximum throughput on standard-size cosmetic bottles.
Preform Weight and Stretching Stroke
Stretching strokes range from 240 mm to 550 mm across the series. Share preform gram weight and target bottle height with our engineering team to validate compatibility before final model selection.
Compressor and Chiller Infrastructure
High-pressure air consumption ranges from 800 ltr/min on compact 2-cavity models to 16,000 ltr/min on the large-format 2C260. Cooling water at 8–12 °C with adequate flow rate is mandatory for mold and machine longevity.
متعلقہ سامان
The EP daily chemicals series integrates with the following upstream and auxiliary equipment available from EVER POWER:
اکثر پوچھے گئے سوالات
Can the EP series produce both round and oval cosmetic bottles on the same machine?
Yes. Round, oval, flat-panel, and limited-asymmetric shapes are all achievable through mold design. The blow mold defines the container shape — switching between profiles requires only a mold changeover, with PLC recipe recall for the new format parameters.
How long does a mold changeover take between bottle formats?
A trained operator completes a standard mold changeover on a 2-cavity machine in approximately 25–45 minutes, including parameter reload. Oven lamp profile fine-tuning for a significantly different preform height may add 10–15 minutes.
What preform sources are compatible with the EP blowing machine?
The EP two-stage machine accepts PET and PETG preforms from any qualified manufacturer, provided neck finish dimensions and IV values fall within the design envelope. EVER POWER can supply matched preform injection molds as part of a full turnkey project.
Is on-site commissioning support available internationally?
Factory-trained engineers are dispatched to all export markets for installation, process parameter setup, and operator training. Remote diagnostic support via video link and PLC data transfer is available as standard throughout the machine service life.
Ready to Specify Your EP Blow Molding Line?
Share your bottle dimensions, target output, and material type — our engineering team responds with a matched model recommendation within 24 hours.
اضافی معلومات
| ترمیم شدہ | hyw کی طرف سے |
|---|
متعلقہ مصنوعات
-
کاسمیٹک بوتل کے لئے دو مرحلے پی ای ٹی اسٹریچ بلو مولڈنگ مشین | 600-7200 BPH
-
نیم خودکار پیئٹی بلو مولڈنگ مشین بنانے والا | EPS سیریز | 150-1100 BPH
-
بچے کی بوتل کے لئے دو مرحلے PP/PET اسٹریچ بلو مولڈنگ مشین | 600-2800 BPH
-
دو مرحلے PET اسٹریچ بلو مولڈنگ مشین برائے میڈیسن بوتل | 1800-7200 BPH
-
خوردنی تیل کی بوتل کے لیے دو اسٹیج پی ای ٹی اسٹریچ بلو مولڈنگ مشین | 700-1800 BPH
-
پانی اور مشروبات کی بوتل کے لیے دو اسٹیج پی ای ٹی اسٹریچ بلو مولڈنگ مشین | 1800-9200 BPH
-
وائڈ ماؤتھ فوڈ جار کے لیے دو اسٹیج پی ای ٹی اسٹریچ بلو مولڈنگ مشین | 600-4500 BPH


