
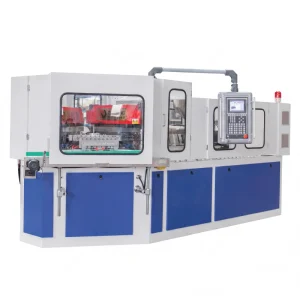
Automatische spuitblaasvormmachine EP40 400KN voor farmaceutische en cosmetische flessen (CE ISO-gecertificeerd)
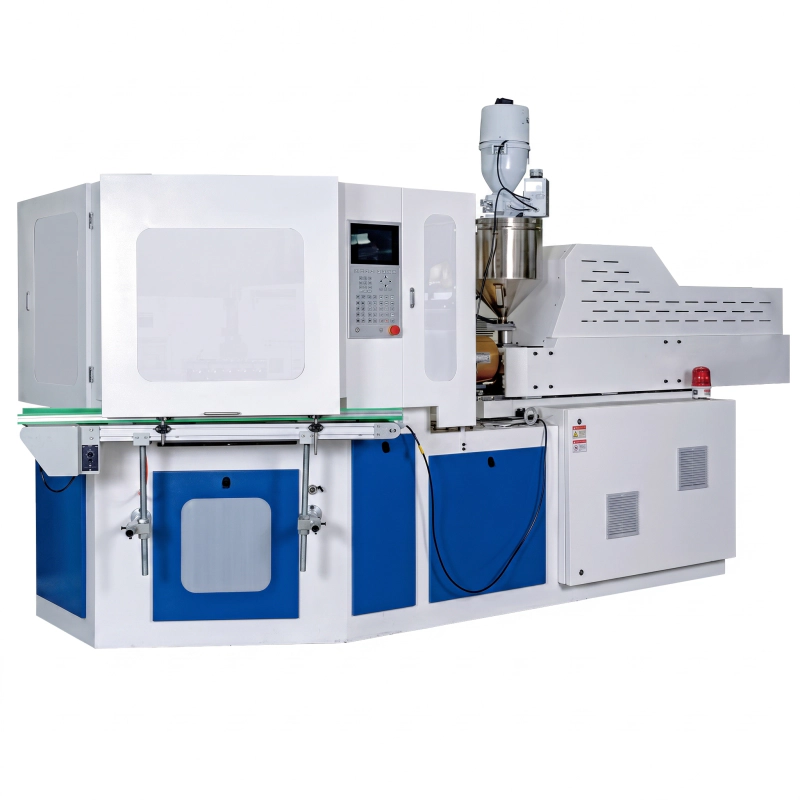
EVER POWER EP40 injection blow molding machine delivers 400KN clamping force, 190-260g injection weight, 3.5s dry cycle and up to 9-cavity output. Three-station one-step IBM process for flash-free pharma, cosmetic and daily chemical bottles from 1ml to 1500ml. CE certified, servo-hydraulic drive, 20% energy saving vs industry average.
What Is the EVER POWER EP40 One-Step Injection Blow Molding Machine?
The EVER POWER EP40 is a fully automatic one-step IBM (Injection Blow Molding) machine engineered for precision hollow container production. As a dedicated fabrikant van spuitblaasvormmachinesEVER POWER heeft tientallen jaren aan expertise op het gebied van gereedschap en processen in dit model geconcentreerd. Het resultaat is een machine waarbij de gehele fles – van preforminjectie tot het uiteindelijke blazen en uitwerpen – in één machinecyclus wordt voltooid, zonder tussenkomst van de operator, zonder materiaaloverdracht tussen machines en zonder de braamvorming en afval bij de scheidingslijn die kenmerkend zijn voor extrusieblaassystemen.
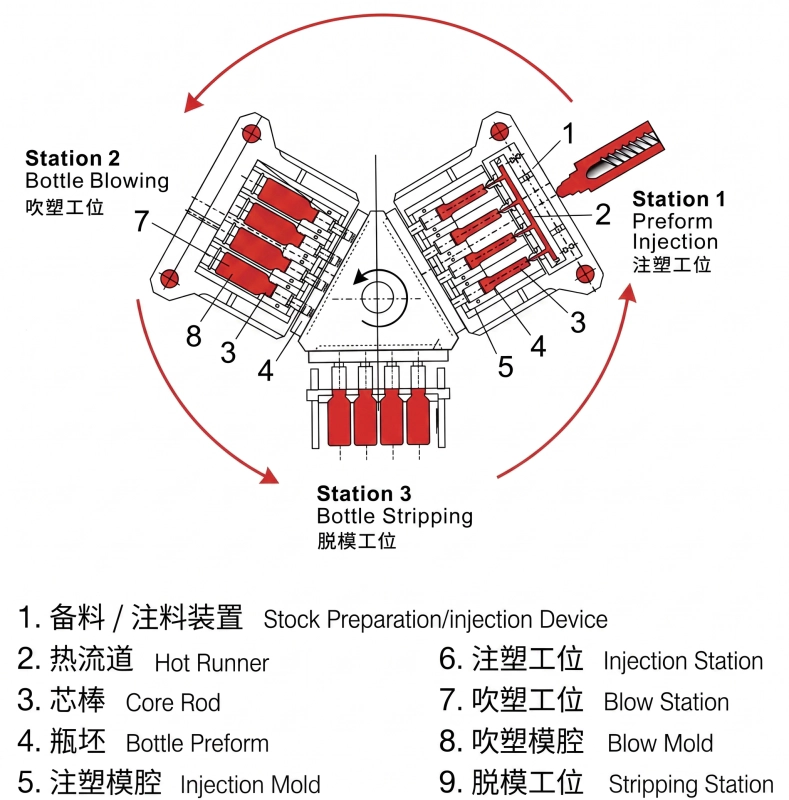
Dit éénstaps IBM-machine is the preferred choice for pharmaceutical bottle blowing and cosmetic container manufacturing where dimensional consistency is non-negotiable. Each cycle on the EP40 runs three simultaneous operations: while new preforms are being injection-molded at Station 1, the previous batch is being blown to final shape at Station 2, and the completed bottles from Station 2 are being stripped and conveyed to the outfeed conveyor at Station 3. This triaxial parallelism means the productive output equals the injection cycle time alone - not the sum of injection plus blowing plus ejection - giving the EP40 a significant throughput advantage over two-stage stretch blow systems for small and medium volume containers.
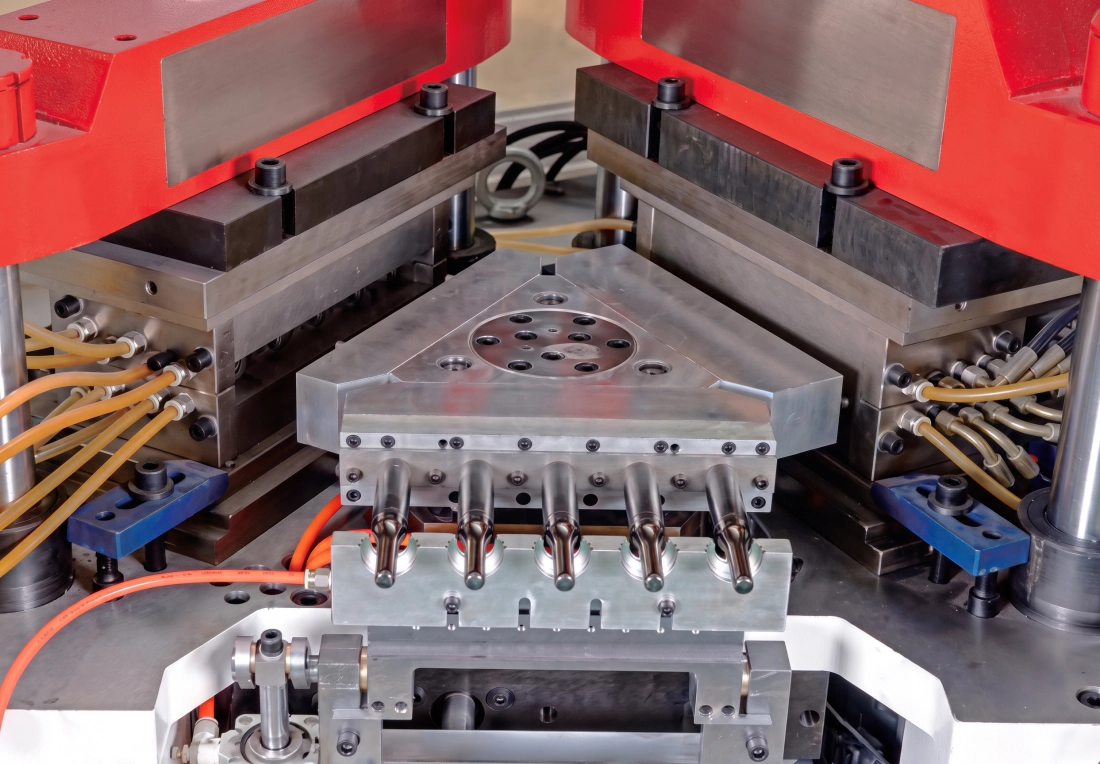
Three-Station Process: How the EP40 Works
Station 1 - Injectie van de voorvorm
Kunststofkorrels worden in de cilinder gesmolten en onder gecontroleerde druk in de injectieholte geïnjecteerd. De flessenhals en schroefdraadgeometrie worden nauwkeurig in de spuitgietmatrijs gevormd. De spuitgietmatrijs opent en de doorn met de hete voorvorm wordt via de draaitoren naar station 2 getransporteerd.
Station 2 - Blaasvormen
De hete voorvorm wordt opgeblazen door perslucht uit de doornkern. De flesvorm wordt volledig bepaald door de matrijsopening. Lucht blaast de voorvorm naar buiten tegen de gekoelde matrijswanden, waardoor de fles zijn uiteindelijke afmetingen aanneemt. De matrijs opent en de revolver beweegt naar station 3.
Station 3 - Uitwerpen en transporteren
De afgewerkte, afgekoelde flessen worden van de mallen verwijderd en op de afvoerband geplaatst. Omdat alle drie de stations gelijktijdig werken, herhaalt de cyclus zich continu. Er is geen secundaire bewerking, geen ontbraampers en geen herverwarming van de flessen nodig - de drie bewerkingen delen één cyclusklok.
Main Technical Parameters - EVER POWER EP40
| Parameter | Artikel (NL) | Eenheid | EP40 |
|---|---|---|---|
| Injectiesysteem | |||
| Schroefdiameter | Schroefdiameter | mm | 40/45 mm |
| Schroef L/D-verhouding | Schroef L/D | - | 22:1 |
| Injectiegewicht | Injectiegewicht | G | 190/260 g |
| Verwarmingsvermogen | Verwarmingsvermogen | KW | 7.5 KW |
| Verwarmingszones van de ton | Aantal vatzones | - | 3+N |
| Injectieberoerte | Injectieberoerte | mm | 120 mm |
| Klemsysteem | |||
| Injectieklemkracht | Klemkracht van de injectie | KN | 400 |
| Injectie openingsslag | Openingsslag voor injectie | mm | 165 mm |
| Blaasklemkracht | Klemkracht van het blazen | KN | 60 |
| Openingsslag van de blaas | Openingsslag voor het blazen | mm | 140 mm |
| Torenlifthoogte | Hefhoogte van de draaitafel | mm | 70 mm |
| Gietvorm | |||
| Maximale afmetingen van de plaat (LxB) | Maximale afmetingen van de plaat (L x B) | mm | 480x340 mm |
| Vormdikte | Vormdikte | mm | 180 mm |
| Maximale flesdiameter | Diameter van de fles | mm | 120 mm |
| Maximale fleshoogte | Fleshoogte | mm | 220 mm |
| Flesvolumebereik | Geschikt flesvolume | ml | 1-1500 |
| Strippende slag | Strippende slag | mm | 220 mm |
| Hydraulisch systeem | |||
| Hydraulische druk | Hydraulische druk | MPa | 14 |
| Motorvermogen | Motorvermogen | KW | 11 KW |
| Droogcyclustijd | Droogcyclus | S | 3.5 |
| Totaal vermogen | Totaal vermogen | KW | 20 |
| Bedrijfsvermogen | Bedrijfsvermogen | % | 52-70 |
| Overige parameters | |||
| Persluchtdruk | Minimale luchtdruk | MPa | 0.7-1.2 |
| Luchtcapaciteit | Persluchtcapaciteit | M3/min | 0.7 |
| Koelwaterstroom | Waterdebiet | M3/h | 3.5 |
| Koelwaterdruk | Koelwaterdruk | MPa | 0.3-0.4 |
| Afmetingen (L x B x H) | Totale afmeting | M | 3.5x1.3x1.7 M |
| Nettogewicht | Nettogewicht | Ton | 3.8 Ton |
Let op: alle parameters zijn slechts ter referentie. EVER POWER behoudt zich het recht voor specificaties te wijzigen als gevolg van verbeteringen aan de apparatuur.
Max Cavity Count per Container Volume (EP40 - For Reference)
| Volume | 10 ml | 30 ml | 60 ml | 100 ml | 250 ml | 500 ml | 1000 ml |
|---|---|---|---|---|---|---|---|
| Max. holtes | 9 | 8 | 6 | 4 | 3 | 2 | 1 |
Core Hardware Architecture of the EP40
Volledig stalen frame in Europese stijl
CNC-machined monolithic machine bed and platen mounts ensure parallelism between injection and blow clamping platens. Tie-bar surfaces are induction-hardened. The EP40 clamping force is 20-30% above equivalent-tonnage competitors due to the boosted pressurized clamping structure.
Bimetalen schroef en cilinder
The plasticizing unit uses a bimetallic-lined barrel and a hardened alloy screw rated for glass-fiber and mineral-filled compounds. The EP40 screw diameter of 40/45 mm at 22:1 L/D delivers thorough homogenization with a 190/260 g shot capacity, covering the full range of bottle weights for this tonnage class.
Proportionele klep hydraulische regeling
Zowel de injectiedruk als de blaasdruk worden geregeld via servoproportionele hydraulische kleppen. Dit maakt meertraps injectieprofilering mogelijk (vulsnelheid, omschakeling, pakdruk) voor dunwandige voorvormen, en nauwkeurige regeling van de blaasdrukverhoging die de radiale webvormingsdefecten elimineert die vaak voorkomen bij systemen met eentraps blaaskleppen.
PLC-touchscreenbesturingssysteem
The EP40 control panel runs a full-color PLC touch-screen with parameter recipe storage. All process variables - temperatures, pressures, velocities, timings - are set and monitored from a single screen. Alarm history, production counters and fault codes are logged and displayed in real time.
Geoptimaliseerd hotrunner-systeem
Het hotrunner-verdeelstuk van de spuitgietmatrijs is ontworpen voor een stroming zonder dode zones, waardoor de gewichtsafwijking in grammen over alle holtes tot een minimum wordt beperkt. De temperatuurregeling met een nauwkeurigheid van plus of minus 1 graad voorkomt degradatie van warmtegevoelige materialen en is essentieel voor een consistente helderheid in transparante verpakkingen.
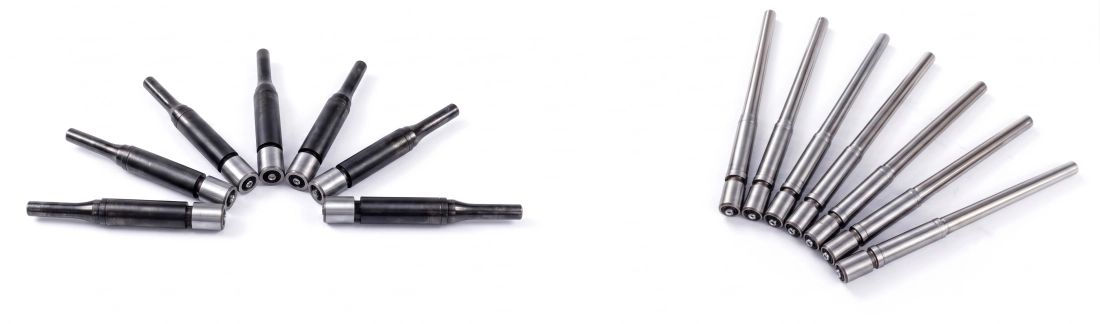
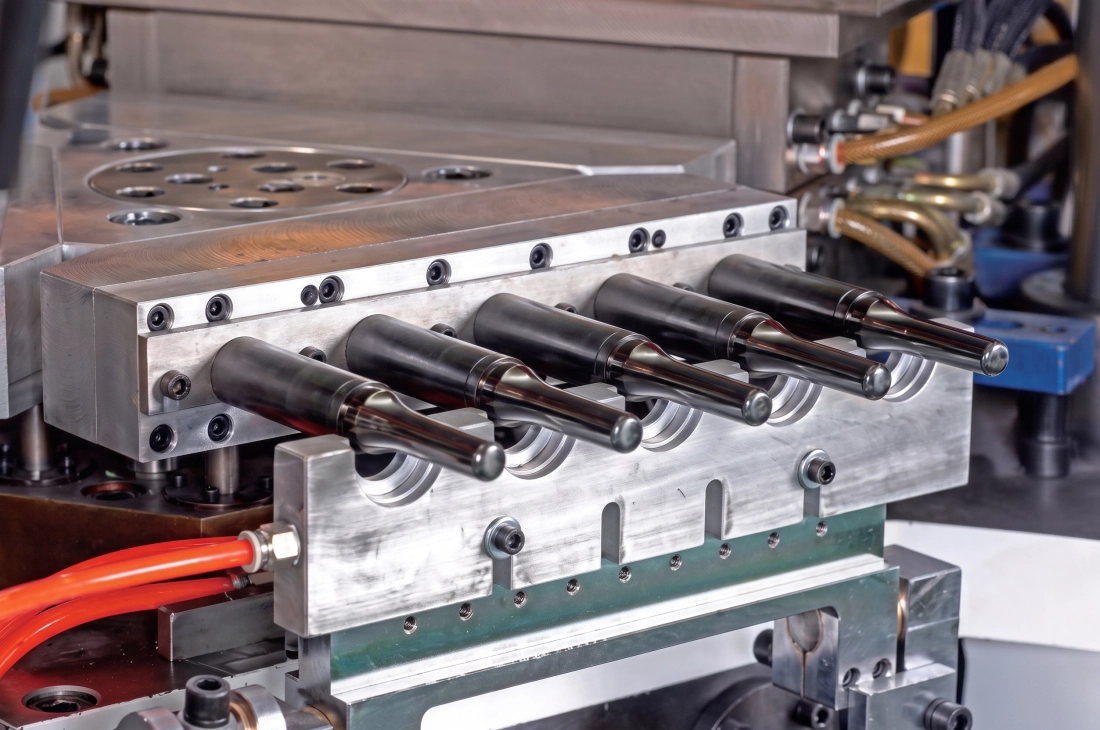
Speciaal ontwerp voor de kernstang
The mandrels (core rods) feature internal cooling channels that reduce core temperature between the injection and blow stations, accelerating the cooling phase. Fast-cycle mandrels enable the EP40 to achieve a 3.5 S dry cycle without sacrificing preform cooling uniformity or dimensional stability.
Spuitblaasvormen versus extrusieblaasvormen: waarom IBM wint bij precisieverpakkingen
Buyers evaluating hollow container equipment often compare IBM and EBM on capital cost alone. The EP40 is more than a machine choice - it is a process choice that determines your long-term production economics and the quality ceiling your facility can achieve. The comparison below reflects real production differences that directly affect your cost per thousand bottles and your ability to win pharmaceutical and cosmetic supply contracts.
| Nee. | Vergelijkingsitem | Injectieblazen (IBM) | Extrusieblazen (EBM) |
|---|---|---|---|
| 1 | Consistentie van het flesgewicht | Gewichtsvariatie circa 1% | Gewichtsvariatie circa 3% |
| 2 | Uniformiteit van de wanddikte | Gelijkmatige wanddikte overal | Wanddikte varieert 10-20% |
| 3 | Fleshals / Schroefdraad | Geen flits, geen scheiding in de nek | Afsnijding, verzwakte basis en hals |
| 4 | Basisconvexiteit | Sterke positieve convexiteit, stabiele basis | Zwakke convexiteit als gevolg van een knijplas |
| 5 | Materiaalafval | Geen afval - geen restmateriaal of afval | 20-40% schroot van pinch flash |
| 6 | Mogelijkheid tot ultradunne wanden | Minder geschikt voor zeer dunne wanden | Wanddikte instelbaar via controller |
| 7 | Milieugevoeligheid | Niet gevoelig voor omgevingsveranderingen | Regelmatige aanpassing vereist |
| 8 | Aantal caviteiten en output | Hoge cavitatie, hoog rendement, vlakke mond | Minder holtes, lagere output, ongelijkmatige hals |
| 9 | Levensduur en kosten van de mal | Lange levensduur van de mal, geschikt voor langdurige, grootschalige productie. | Kortere levensduur van de mal, lagere aanschafkosten |
| 10 | Voetafdruk | Compact geïntegreerd systeem, kleine afmetingen | Meer hulpapparatuur, groter vloeroppervlak |
| 11 | Ovale containervorming | Het is lastiger om ovale vormen te maken. | Het is gemakkelijker om ovale profielen te vormen. |
Application Fields and Container Types for the EP40
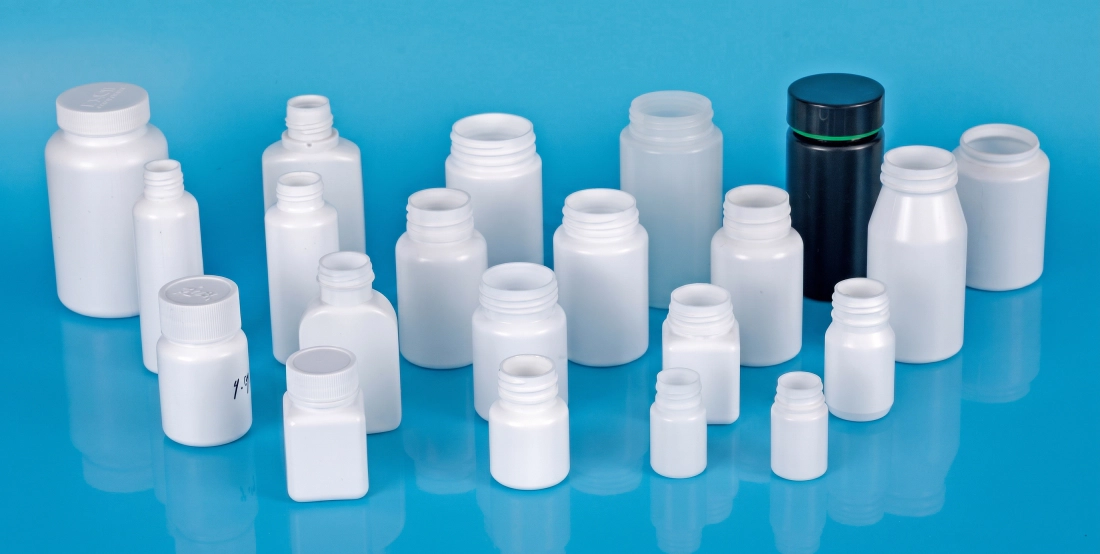
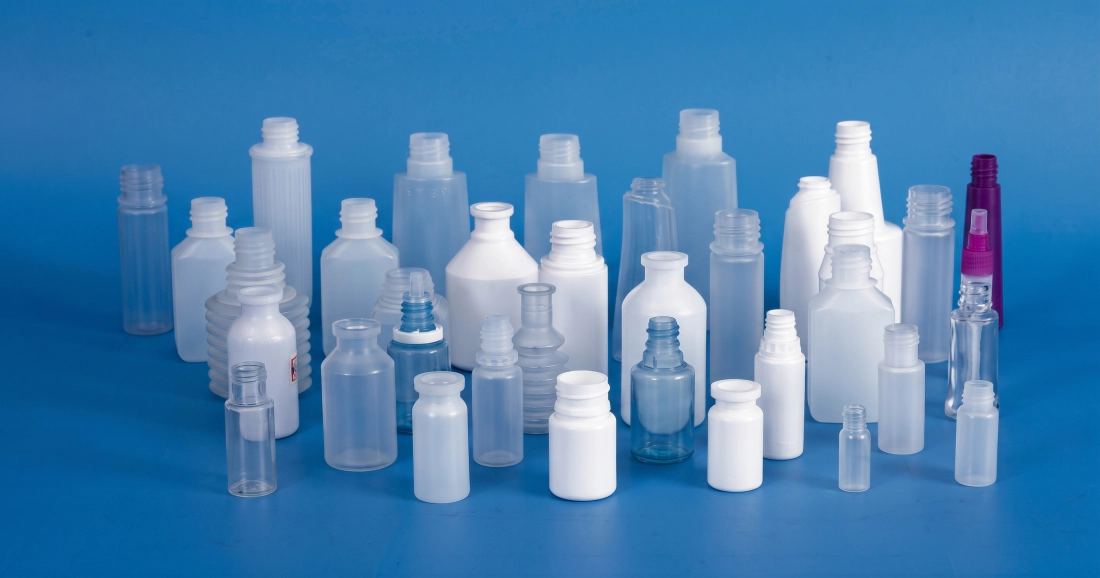
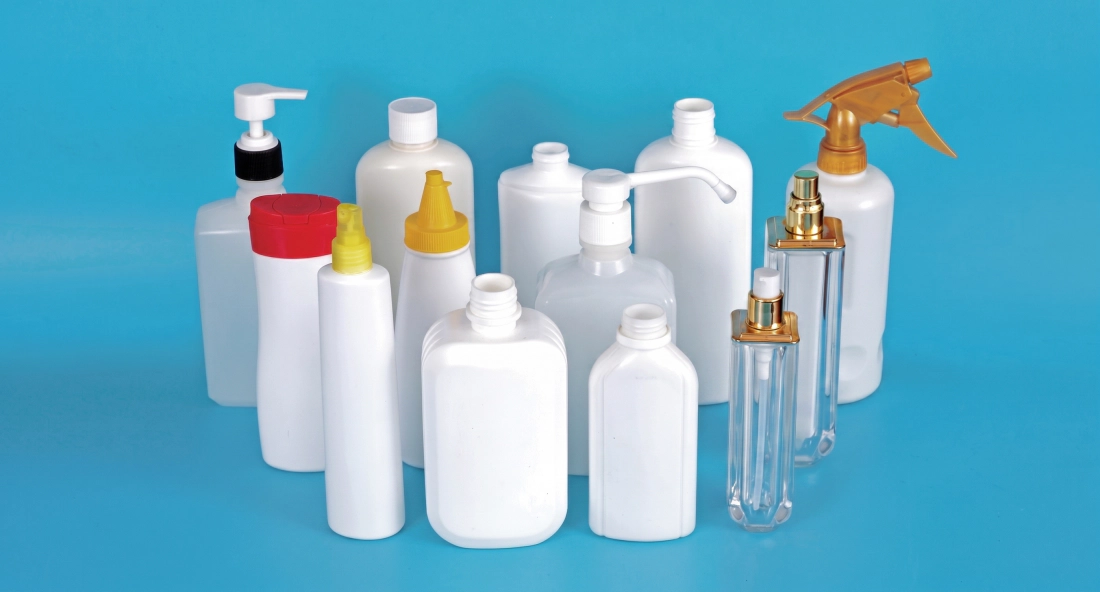
The EP40 is designed to produce bottles and containers from 1ml to the maximum volume for this model, covering the full range of primary packaging needs across four major market verticals. The table below shows the container types and industry segments where this automatische spuitblaasvormapparatuur levert het hoogste commerciële rendement op.
Farmaceutische industrie
- Oogdruppelflesjes (LDPE, 5-30 ml)
- Flesjes voor orale tabletten en capsules (HDPE, 30-500 ml)
- Neusspray en pompflessen (PP)
- Flesjes voor vloeibare medicijnen met kindveilige doppen
- Vaccin- en reagensflacons (LDPE, 1-20 ml)
- GMP-gecertificeerde amberkleurige en witte HDPE-pillenflessen
cosmetica-industrie
- Roll-on deodorant applicatorflesjes (PE, 50-100 ml)
- Mascaratubes en -staafjesflesjes (PP, 5-20 ml)
- Nagellakflesjes (PS, 10-30 ml)
- Pompflacons voor lotions en serums (PCTG, 30-200 ml)
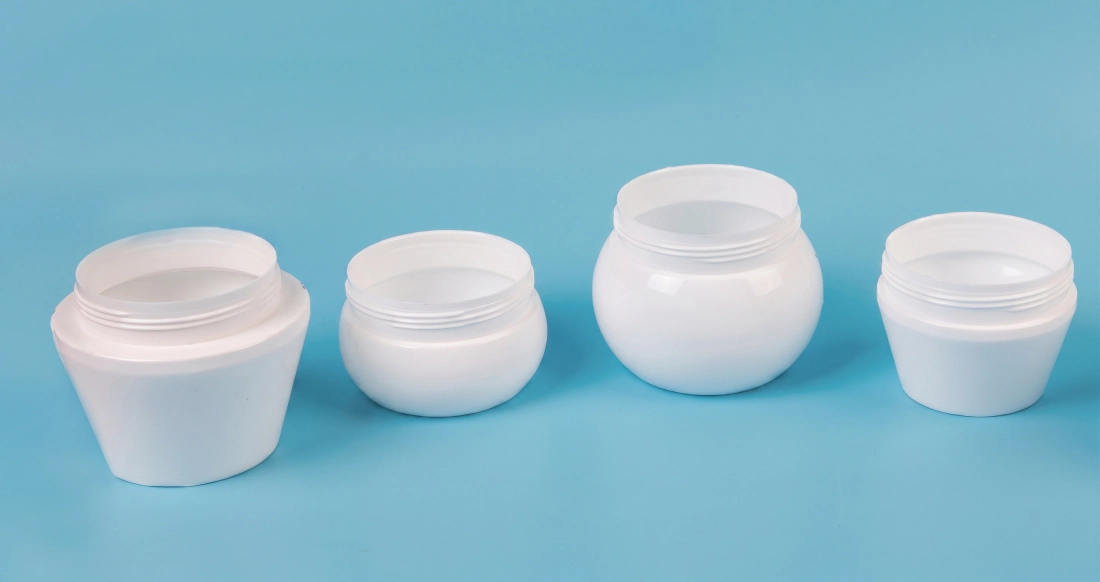
- Crèmepotten met brede opening (PP/PS)
- Flesjes foundation en toner
Babyproducten en -voeding
- Babyvoedingsflessen (PP, PPSU, 150-300 ml)
- Babyvoeding schepjes flesjes
- Honing- en siroopverpakkingen (LDPE)
- Speciale drankverpakkingen voor kleine volumes
- Flesjes met proefmonsters van eetbare olie
- Yoghurt- en zuivelverpakkingen
Dagelijkse chemische en industriële
- Shampoo- en conditionerflessen (HDPE/PP)
- Handdesinfectie- en lotiondispensers
- Monsterflessen voor autovloeistoffen
- Flessen met concentraat van landbouwchemicaliën
- Verpakkingen van schoonmaakproducten
- Industriële reagensflessen met nauwkeurige hals.
Servo-Hydraulic System vs. Conventional Hydraulic: A Technical Breakdown
The EP40 incorporates a high-response servo-hydraulic drive system that fundamentally changes how energy is consumed during the molding cycle. In a conventional fixed-displacement hydraulic pump, the motor runs at full speed regardless of demand - wasting energy as heat during low-load phases such as dwell, cooling and ejection. The servo motor on the EP40 constantly matches pump displacement to actual demand, reducing motor speed to near-zero during the cooling and hold phase.
The practical result: operating power consumption sits at just 52-70% of total installed power, compared to 80-90% for conventional systems. Oil temperature rise is dramatically suppressed - typically 5-8 degrees Celsius per hour vs. 15-20 degrees for fixed-pump systems - which extends hydraulic seal life and reduces the frequency of oil changes and filter replacements. Noise at the hydraulic station drops below 70 dB(A) during cooling phases, improving the working environment.
During the high-pressure injection and clamping phase, the servo system delivers instant peak torque response for precise pressure and speed profiling. This fine control reduces flash formation at the parting line and ensures consistent preform weight shot-to-shot. For pharmaceutical and cosmetic packaging where every milligram of wall thickness matters, this repeatability directly translates to fewer rejections and lower material cost per thousand bottles.
Investment Return and Production Efficiency Analysis: Why Choose the EP40?
The acquisition cost of the EP40 must be evaluated against five measurable efficiency drivers that determine cost per thousand bottles and payback period. Purchasing engineers who evaluate only machine price - without these five factors - systematically undervalue the IBM platform and overestimate EBM economics for their target application.
1. Nul Flash-schroot
IBM produceert geen braamvorming en geen afval door knijpen. EBM genereert 20-401 TP3T aan flesgewicht aan afval per cyclus. Bij 200 ton PP per jaar bespaart IBM, zonder afval, 40-80 ton hars per jaar. Bij een prijs van 1.500 USD per ton betekent dat een besparing van 60.000-120.000 USD aan grondstoffen per jaar, alleen al door één machine.
2. Geen ontbraamwerkzaamheden
EBM requires a secondary deflashing operation - either inline mechanical or manual - adding labor cost, a second machine footprint, and an additional quality failure point. IBM bottles from the EP40 come off the conveyor with zero post-processing required before filling or labeling, saving 1-3 operators per shift.
3. Doorvoer bij korte droogcycli
The EP40 achieves a 3.5 S dry cycle. With 6 cavities at 60ml, annual output at 6,000 hours run time exceeds 37.0 million bottles. This throughput concentration into a single compact machine reduces total asset investment per unit of capacity versus multi-machine EBM lines at equivalent output.
4. Snelle matrijswissel
The injection mold and blow mold on the EP40 can be changed in 2-4 hours by a trained two-person team. Recipe recall from the PLC removes setup time entirely for repeat jobs. Facilities running 8-15 SKUs on a single EP40 achieve mold changeover frequency of 2-4 per week with total changeover downtime below 10% of available production hours.
Voetafdruk en energie-efficiëntie
The EP40 footprint of 3.5x1.3x1.7 M consolidates injection, blow and ejection into a single machine envelope. Compare this to a two-machine EBM line (extruder plus blow machine, plus deflash press, plus conveyor) which typically occupies 3-4 times the floor area for equivalent throughput. Utility connections - compressed air at 0.7-1.2 MPa, cooling water at 3.5 M3/h flow, electrical connection at 20 KW total - are all single-point utilities, reducing installation complexity and ongoing maintenance overhead.
Factory building cost in pharmaceutical-grade cleanroom environments can reach 2,000-5,000 USD per square meter. The compact footprint of the EP40 directly reduces the cleanroom area required to produce a given volume of output - a capital benefit that does not appear in machine comparison tables but materially affects total project economics.
EP-serie IBM matrijskenmerken en ontwerpnormen
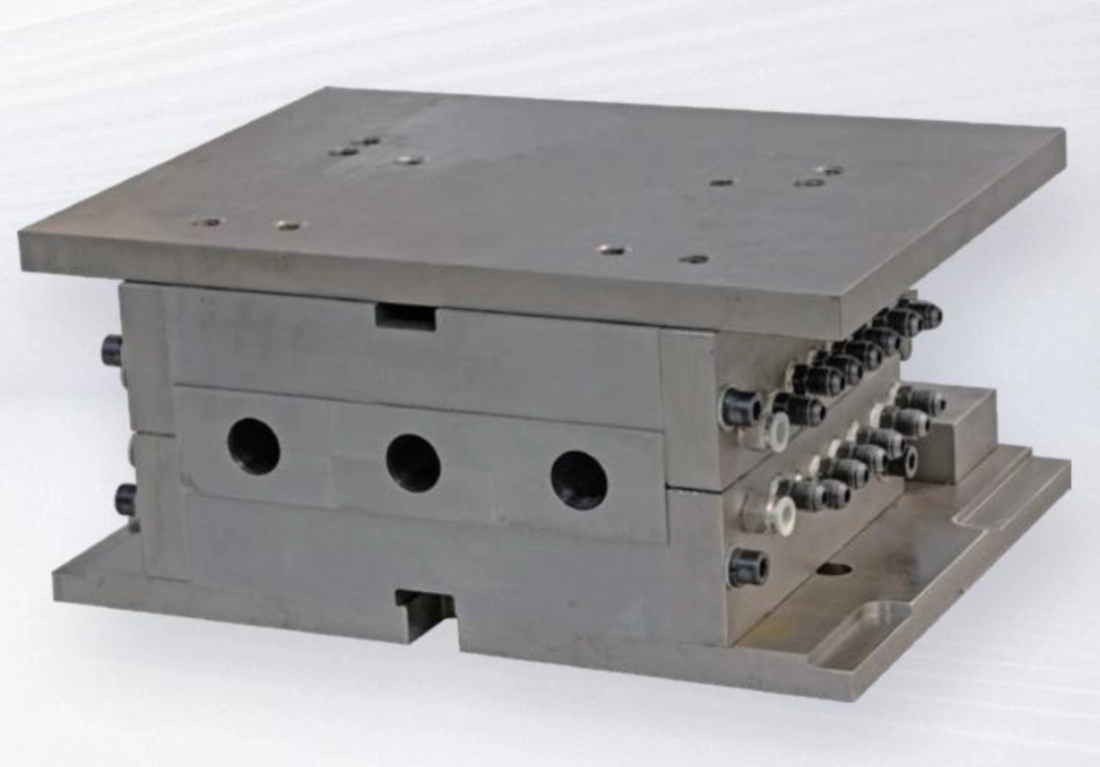
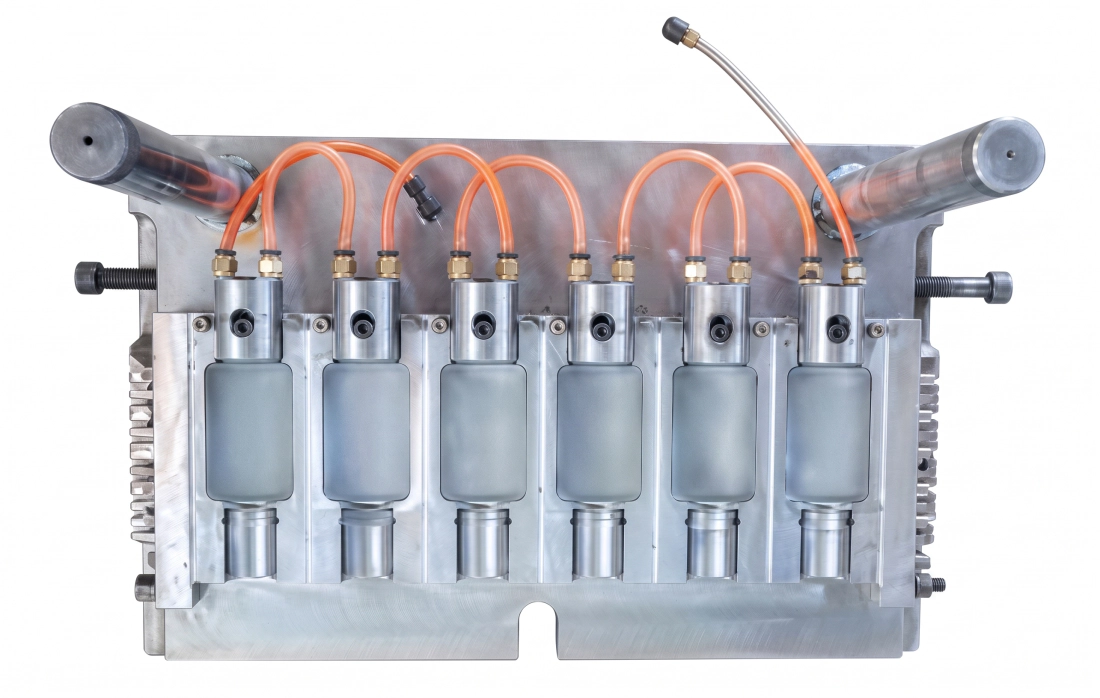
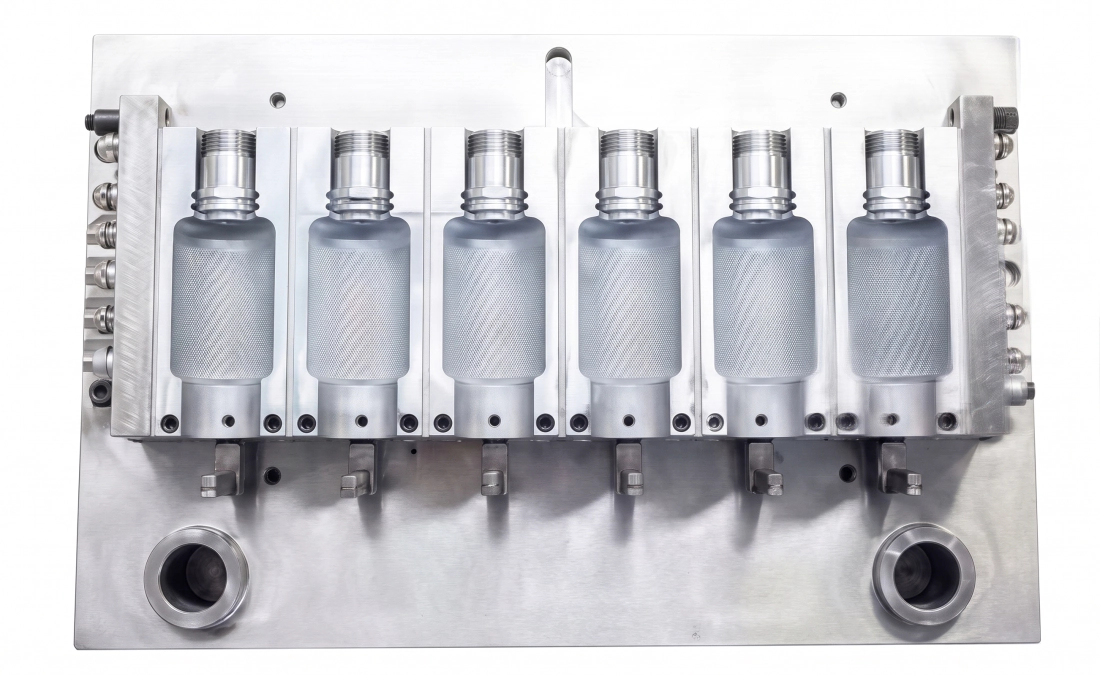
- ■Actief caviteit- en halsblokontwerp - De spuitgietmatrijzen en halsblokken zijn onafhankelijk van elkaar verstelbaar, waardoor de afmetingen van de voorvormbuis nauwkeurig kunnen worden afgesteld zonder de gehele matrijs te hoeven vervangen. De olie- en waterkanalen zijn speciaal ontworpen voor een stabiele temperatuurverdeling en eenvoudige demontage.
- ■Hoogwaardige staalsoorten - De behuizingen van de spuitgietmatrijzen zijn gemaakt van 4Cr13 roestvrij staal of geïmporteerd hoogwaardig S136 gelegeerd staal. S136 is een spiegelglad, corrosiebestendig staal met een doorharding tot 52 HRC. De behuizingen van de blaasvormmatrijzen kunnen worden vervaardigd van een magnesium-aluminiumlegering voor een superieure warmtegeleiding en een lagere inertiemassa op de draaitoren.
- ■Geoptimaliseerd ontwerp van het heteluchtkanaal en de voorvorm. - Het hot runner-verdeelstuk is ontworpen om de gewichtsafwijking in grammen over alle holtes te minimaliseren en de variatie in wanddikte van het voorvormlichaam te verminderen. Het ontwerp van de doorn zorgt voor een uniforme luchttoevoer voor een consistente blaasexpansie en snelle koeling.
- ■Nauwkeurige afmetingen van de halsdraad en afdichting - De binnen- en buitendiameter van de flessenhals, de schroefdraadspoed en de flensgeometrie worden machinaal vervaardigd volgens de toleranties van de tekening. De afdichtingsgraad van de dop bedraagt 100% bij alle productiemonsters.
- ■Geen flits bij de nek en de basis. - the IBM process geometry eliminates parting-line flash at the bottle mouth and pinch-weld flash at the base. Bottles exit the EP40 with no trimming required at either end.
- ■Productconsistentiemetrieken - De afmetingen, het gewicht, de positie van de scheidingslijn en de wanddikte zijn consistent in alle holtes en in alle productiebatches, waardoor farmaceutische klanten de productie per batch op statistische basis kunnen valideren zonder de overheadkosten van 100%-inspecties.
Equipment Selection Guide: Is the EP40 Right for Your Production Requirements?
Selecting the correct IBM tonnage requires calculating the intersection of three variables: preform weight, required cavity count, and target output per hour. Use this framework to confirm whether the EP40 is correctly sized for your application, or to understand what production parameters it can support.
Stap 1: Bereken het gewicht van de voorvorm
Take the target bottle weight in grams (including the neck, body and base). Add 2-5% for process cushion. The EP40 injection weight of 190/260 g must be equal to or greater than (target preform weight x number of cavities). For example: a 5g preform at 8 cavities requires 40g shot weight, well within the 190/260 g capacity.
Stap 2: Bereken het benodigde aantal caviteiten
Target output (bottles/hour) divided by (3600 seconds / cycle time in seconds) gives required cavities. At a 3.5 S cycle and 10,000 bottles per hour target: 10,000 / (3600 / 3.5) = 10 cavities minimum. Cross-check against the cavity table above to confirm the EP40 can deliver this at your bottle volume.
Stap 3: Controleer of de vormplaat goed past.
The injection mould layout (cavity array footprint) must fit within the EP40 max platen size of 480x340 mm. Wide-bottle (diameter greater than 120mm) or tall-bottle (height greater than 220mm) applications exceed the EP40 mould envelope and require a larger model. Confirm your bottle OD and height before specifying cavity count.
Stap 4: Materiaal en injectiedruk
PP requires higher injection pressure and melt temperature than LDPE. PC and PETG require even higher barrel temperatures and longer residence-time plasticization. The EP40 hydraulic system pressure of 14 MPa and motor of 11 KW supports the injection forces needed for PP and engineering grade materials at the rated injection weight. Confirm your resin specification with the EVER POWER application team before ordering.
EVER POWER application engineers provide free pre-sales technical consultation to validate your container dimensions, material, cavity count and production target against EP40 specifications. Contact us with your bottle drawing and production brief for a written confirmation of suitability.
Overzicht van de machinestructuur en onderhoudsrichtlijnen
The EP40 is built around three core functional modules. Understanding their maintenance requirements is essential for sustaining the machine performance metrics - dry cycle, output rate, and product quality - over the full production life of the equipment.
Module 1 - Injectie-eenheid: Schroef, Cilinder, Hotrunner
De injectie-eenheid smelt en doseert plastic in de matrijs van de voorvorm. Dagelijks onderhoud: controleer de temperatuurprofielen van de cilinder aan de hand van de ingestelde waarden, inspecteer de schroefpunt en de terugslagklep op slijtage en controleer of de temperatuur in de hotrunnerzone binnen 2 graden van de ingestelde waarden ligt vóór de opstart. Wekelijks: inspecteer de isolatiebanden van de cilinder, controleer de afdichtingen van de injectiecilinder op olielekkage en verwijder eventuele kleurverontreiniging van eerdere productie. Maandelijks: verwijder en reinig de terugslagklep en de schroefpunt; inspecteer de schroefbladen op slijtage en meet de diameter van de cilinderboring op speling. Vervang de cilinder als de speling de tolerantie van de fabrikant overschrijdt om smeltomleiding en inconsistentie in het spuitgewicht te voorkomen.
Reinigingsprocedure: bij het wisselen van donkere naar lichte kleuren of van technische hars naar standaardhars, gebruik een commercieel reinigingsmiddel bij een cilindertemperatuur die 10 graden hoger is dan de ingestelde temperatuur voor het nieuwe materiaal. Voer 5-10 reinigingscycli uit voordat u overschakelt naar het nieuwe materiaal. Laat de cilinder nooit langer dan 20 minuten ongebruikt op verwerkingstemperatuur staan zonder te reinigen - thermische degradatie tijdens stilstand is de belangrijkste oorzaak van zwarte vlekjes bij het opnieuw opstarten.
Module 2 - Klem- en draai-indexeereenheid
Het klemsysteem en de roterende indexeerder dragen de hoogste mechanische belastingen en stellen de hoogste eisen aan de positionering. Dagelijks: smeer de oppervlakken van de trekstangen en de geleiderails van de draaitafel in met vet volgens het smeerschema (EVER POWER specificeert de vetsoort - gebruik geen universeel vet, aangezien dit de viscositeit bij bedrijfstemperatuur mogelijk niet behoudt). Controleer de hydraulische klemcilinder op olielekkage bij de stangafdichting. Luister naar ongebruikelijke geluiden tijdens de indexeerrotatie - een metalen klik of hapering duidt op een hoeklager van de verdeelinrichting dat gecontroleerd moet worden.
Maandelijks: controleer de paralleliteit van de plaat met een meetklok op vier posities van de trekstang; een afwijking groter dan 0,05 mm vereist opnieuw afstellen. Controleer de nauwkeurigheid van de indexeerpositie door een meetklok tegen een referentieoppervlak op de revolverkop te plaatsen en te controleren of dezelfde positie binnen 0,02 mm nauwkeurig wordt herhaald na 100 opeenvolgende indexeercycli. Als er afwijking wordt geconstateerd, stel dan de mechanische aanslag af of neem contact op met de EVER POWER-service.
Module 3 - Hydraulisch systeem en koelcircuit
The hydraulic system is the energy backbone of the EP40. System pressure is set at 14 MPa. Daily: check hydraulic oil level in the tank sight glass, check oil temperature display (normal operating range 40-55 degrees Celsius; above 60 degrees indicates a cooling circuit problem or filter blockage), and inspect all visible hydraulic hose fittings for weeping. The oil filter indicator must be checked every 250 hours - a red indicator requires immediate filter element replacement, not deferral.
Cooling circuit: the EP40 requires clean, scale-free cooling water at 0.3-0.4 MPa pressure and 3.5 M3/h flow. Install a water treatment system upstream of the machine to prevent calcium scale buildup inside mold cooling channels. Scale buildup of just 1mm in a 6mm channel reduces cooling efficiency by over 30%, extending cycle times and reducing output. Flush cooling circuits with a descaling solution annually. Chiller water quality must be neutral pH (6.5-7.5) and contain an anti-corrosion inhibitor compatible with copper and aluminum alloy mold materials.
Kant-en-klare oplossingen en maatwerkdiensten van EVER POWER
EVER POWER supplies the EP40 as either a standalone machine or as the centerpiece of a complete turnkey bottle production line. For customers setting up a new facility or expanding into a new container product line, the turnkey approach eliminates the integration risk that comes from sourcing the IBM machine, molds, auxiliaries, and downstream equipment from separate vendors.
Ontwerp en fabricage van mallen
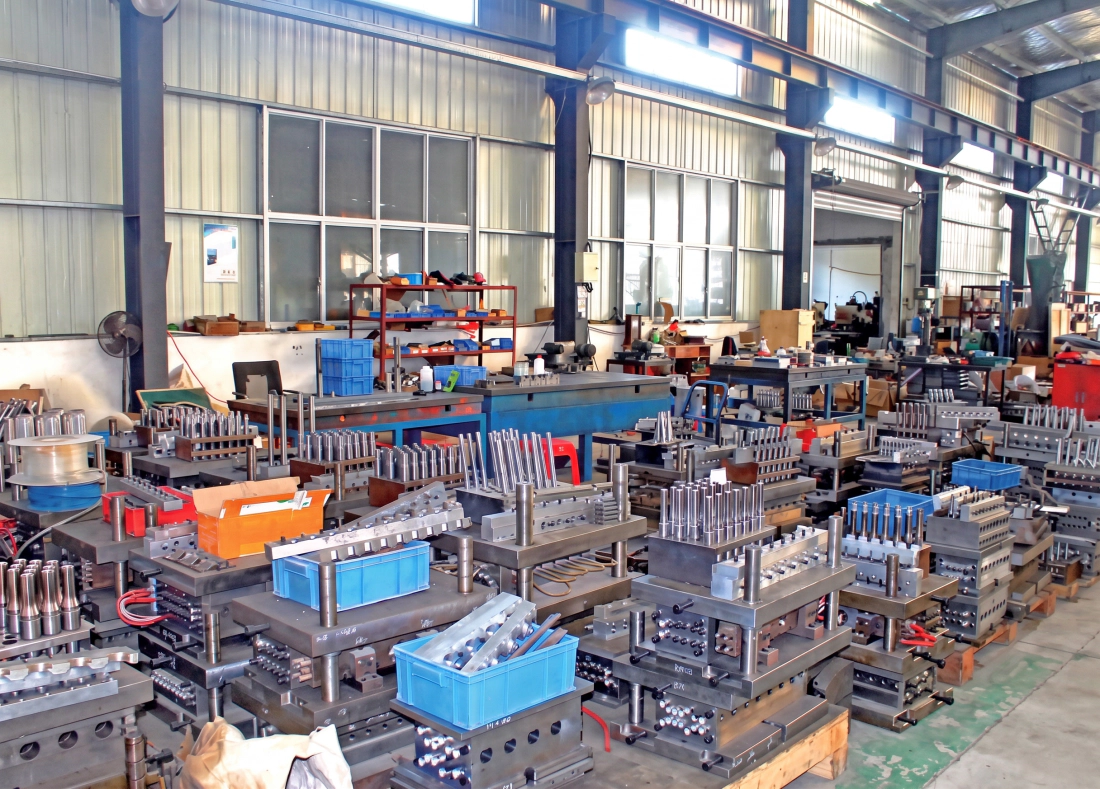
De ingenieurs van EVER POWER ontwikkelen spuitgiet- en blaasvormsets op basis van klanttekeningen van flessen of 3D-bestanden. Meervoudige hotrunner-matrijzen worden vervaardigd van S136- of 4Cr13-staal. Prototype-matrijzen met één caviteit worden gebruikt voor de validatie van de verpakking voordat er matrijzen met een groter aantal caviteiten worden ingezet. T0-matrijsproeven worden in de fabriek uitgevoerd vóór verzending.
Integratie van hulpapparatuur
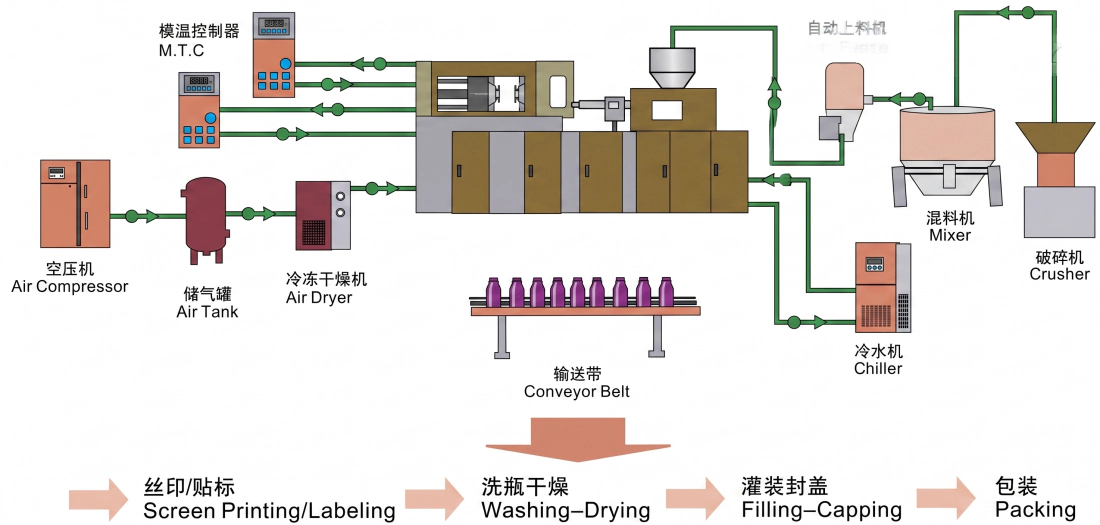
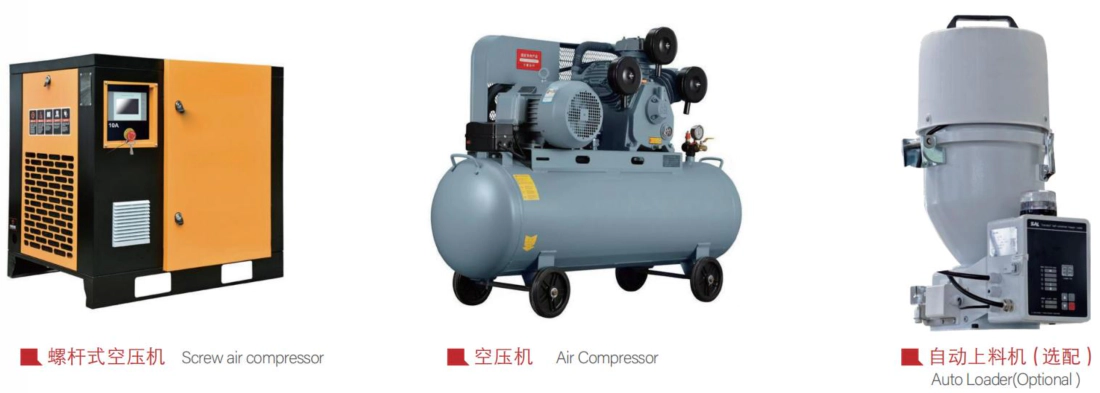
The EVER POWER turnkey line includes: screw air compressor, air tank and air dryer, mold temperature controller, industrial chiller, auto loader, conveyor belt, screen printing and labeling system, washing and drying line, and automatic filling and capping machines. All auxiliary equipment is specified and pre-integrated to match the EP40 output rate.
Kwaliteitssystemen stroomafwaarts
Optional inline bottle visual inspection machine (machine vision system for flash, deformation and contamination detection), automatic leak tester, automatic packing machine, and carton erector. For pharmaceutical lines, 100% inline leak testing and vision inspection are available as integrated modules matched to the EP40 conveyor output speed.
GMP- en cleanroomconfiguratie
Voor farmaceutische klanten die GMP-gecertificeerde productie vereisen, biedt EVER POWER machineaanpassingen aan, waaronder: smering in een gesloten systeem om besmetting van de productzone te voorkomen, roestvrijstalen veiligheidsbehuizingen, een machinebehuizing met HEPA-filter voor compatibiliteit met cleanrooms van klasse 100.000 en documentatieondersteuning voor apparatuurkwalificatieprotocollen (IQ/OQ/PQ).
Auxiliary Equipment Available with the EP40
Kwaliteitscontrole en productienormen
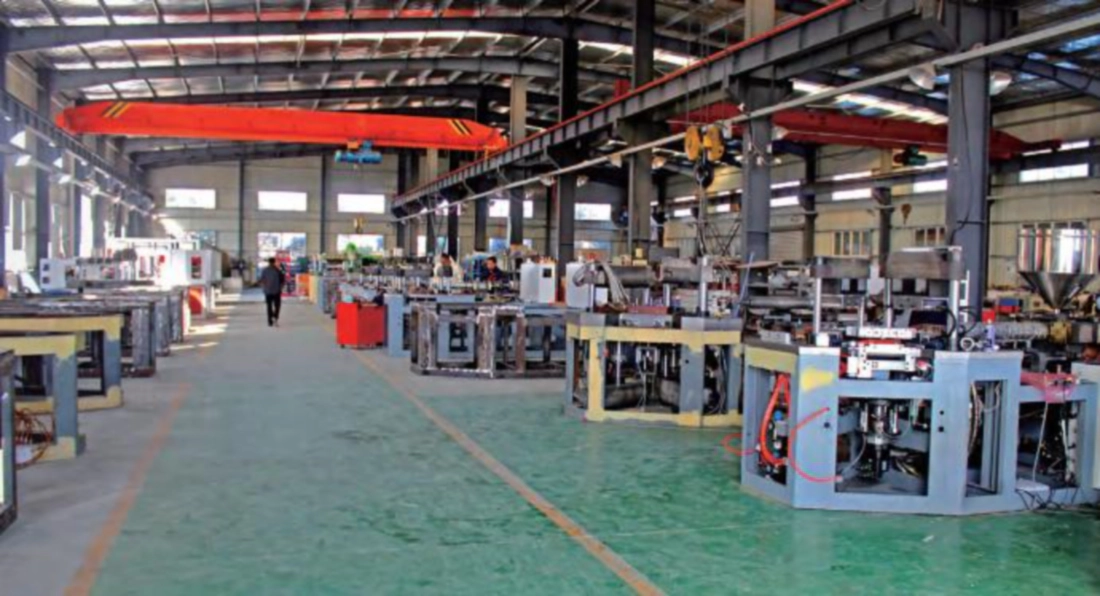
CNC-bewerking van kritische componenten
Het machinebed, de klemplaten en alle precisieoppervlakken worden in één bewerking CNC-gefreesd om geometrische nauwkeurigheid te garanderen. De paralleliteit van de platen wordt met lasermeting tot op 0,02 mm nauwkeurig gecontroleerd. De boringen voor de trekstangen worden gehoond tot H7-tolerantie voor een wrijvingsloze lagerpassing.
Inductieharding van trekstangen
De trekstangen ondergaan een hoogfrequente inductieharding tot een oppervlaktehardheid van 52-58 HRC, gevolgd door precisieslijpen. Deze oppervlaktebehandeling zorgt voor slijtvastheid tegen het herhaalde glijdende contact van de klemplaten gedurende miljoenen cycli, zonder dat er vreten of wrijving optreedt.
Reinheid van het hydraulische circuit
Alle hydraulische circuits worden vóór montage gespoeld, onder druk getest en op deeltjesgehalte gecontroleerd. De reinheid van de hydraulische olie wordt minimaal gehandhaafd volgens ISO 4406 Klasse 17/15/12. De gevoeligheid van proportionele en servokleppen voor vervuiling vereist dit reinheidsniveau om vastlopen van de klepspoelen en afwijkingen in de regeling te voorkomen.
72-uur durende fabriekstest
Every EP40 undergoes a minimum 72-hour continuous loaded run test at the factory before shipment. During this period, production output samples are measured for weight consistency, wall thickness uniformity, and dimensional accuracy. Any parameter outside specification triggers a hold and corrective action before the machine is cleared for delivery.
CE-veiligheidsconformiteit
The EP40 is CE-marked in compliance with EU Machinery Directive requirements. Safety features include: interlocked safety doors with hydraulic circuit interrupt, light curtain protection at the operator access zone, emergency stop at all operator positions, and two-hand operator control for manual mold setting. CE documentation is provided with every machine.
Klantenservice en technische ondersteuning
Installatie en inbedrijfstelling
De senior engineers van EVER POWER zijn verantwoordelijk voor de installatie, inbedrijfstelling en acceptatietests. De engineer blijft ter plaatse totdat de machine een stabiele productiestatus bereikt en alle operators zijn getraind in de bediening van de machine, het wisselen van matrijzen en het routineonderhoud. De acceptatiecriteria worden vóór verzending vastgesteld en gedocumenteerd in het inbedrijfstellingsrapport.
Preventief onderhoudsprogramma
EVER POWER biedt een service voor het herinneren aan gepland onderhoud voor alle machines die in gebruik zijn. De onderhoudskalender omvat dagelijkse, wekelijkse, maandelijkse en jaarlijkse taken. Proactief onderhoud voorkomt ongeplande storingen en vermindert de noodzaak voor dure noodleveringen van onderdelen. Klanten die het preventieve onderhoudsschema volgen, melden consequent een machinebeschikbaarheid van meer dan 95%.
24/7 servicehotline
De EVER POWER-servicehotline is 24 uur per dag, 7 dagen per week bereikbaar. Bij dringende productiestoringen kunt u de servicelijn bellen of een bericht sturen. Een gekwalificeerde technicus zal binnen 2 uur reageren om het probleem op afstand te diagnosticeren. Indien service op locatie vereist is, stuurt EVER POWER een technicus met de kortst mogelijke responstijd voor uw locatie.
Voorraad reserveonderdelen
EVER POWER maintains a comprehensive spare parts inventory for all EP40 components including hydraulic seals, proportional valve cartridges, heating bands, temperature sensors, drive belts and electrical components. Parts can be shipped globally within 48 hours for items in stock. Critical fast-wear items are available for customer-held local inventory based on EVER POWER recommendations.
Technische opleidingsprogramma's
Naast de standaard installatietraining biedt EVER POWER speciale trainingsmodules aan: machinebediening, optimalisatie van het matrijsproces, matrijswissel en -instelling, onderhoud van het hydraulisch systeem en probleemoplossing voor specifieke materialen zoals PP, LDPE en PCTG. De training kan plaatsvinden in de EVER POWER-fabriek of op locatie bij de klant.
Frequently Asked Questions - EVER POWER EP40
What materials can the EP40 process?
The EP40 is compatible with HDPE, LDPE, PP, PS (including lactic acid bacteria grade transparent PS), ABS, EVA, bio-based corn material, PCTG, and similar thermoplastics. For engineering resins such as PC, PETG and Tritan, the screw L/D of 22:1 and the 3+N heating zones provide the residence time and temperature profile needed for thorough, degradation-free plasticization. Confirm your resin grade with EVER POWER application engineering before ordering.
Can the EP40 be used for pharmaceutical GMP production?
Yes. The EP40 can be configured for pharmaceutical GMP production environments. Key features supporting GMP include: the one-step process eliminates inter-machine bottle transfer that introduces contamination risk in two-stage systems; the closed lubrication system prevents lubricant contamination of the product zone; and the machine can be specified with a stainless steel safety enclosure suitable for cleanroom installation. EVER POWER can provide equipment documentation to support IQ/OQ/PQ qualification processes for pharmaceutical facility validation.
How long does mould changeover take on the EP40?
A trained two-person team can complete a full mold changeover (injection mold, blow mold, and mandrel set) on the EP40 in approximately 2-4 hours, depending on the mold design and the changeover frequency experience of the team. PLC recipe recall eliminates parameter re-entry time for repeat mold sets. Facilities that invest in quick-release clamping plates for the mold base can reduce changeover to under 2 hours.
What certifications does the EP40 carry?
The EP40 is CE-marked for the European market. The machine design complies with EU Machinery Directive safety requirements including interlocked guards, emergency stop systems, and electrical safety standards. EVER POWER is an ISO-certified manufacturer. Machine documentation is provided in English and can be supplied in other languages upon request for export markets.
What is the lead time for the EP40 and an associated mould set?
Standard machine lead time for the EP40 is 45-75 days from order confirmation and deposit receipt, depending on production schedule at time of order. Mold sets are typically supplied in 60-90 days from final confirmation of bottle drawings and material specification. The machine and mold sets can be scheduled to arrive simultaneously for a coordinated installation. Contact EVER POWER for current lead time at time of inquiry.
Ready to Specify the EVER POWER EP40 for Your Production Line?
Stuur uw flesontwerp, het gewenste volume, de materiaalspecificaties en de vereiste productie per uur naar ons applicatieteam. Wij bevestigen schriftelijk het juiste aantal matrijsvormen en de machineconfiguratie en sturen u binnen 3 werkdagen een gedetailleerde offerte.
Aanvullende informatie
| bewerkt | door hyw |
|---|
Gerelateerde producten
-
EP60HE Hogesnelheids volledig elektrische spuitblaasvormmachine, hydraulische nulcyclus, 2,5s cyclus
-
Zware spuitblaasvormmachine EP135 1350KN IBM met hoge caviteit voor cosmetische en farmaceutische flessen
-
Industriële spuitblaasvormmachine EP110 1100KN Automatische IBM-apparatuur voor grote volumes flessen
-
Hoogvermogen spuitblaasvormmachine EP80 800KN braamvrije flessenvormmachine
-
Automatische spuitblaasvormmachine EP60 600KN voor farmaceutische en cosmetische flessen


