
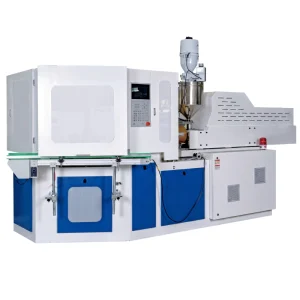
دستگاه قالب گیری بادی تزریقی تک مرحله ای اتوماتیک EP60 600KN تولیدکننده بطری آرایشی دارویی

EVER POWER EP60 IBM machine features 600KN injection clamping force, 260-383g injection weight, 4s dry cycle and up to 14-cavity output. Ideal for pharmaceutical pill bottles, eye drops, cosmetic containers 1-2000ml. European-style structure, servo-hydraulic system, 52-70% operating efficiency. CE ISO certified. Request a quote.
What Is the EVER POWER EP60 One-Step Injection Blow Molding Machine?
The EVER POWER EP60 is a fully automatic one-step IBM (Injection Blow Molding) machine engineered for precision hollow container production. As a dedicated تولید کننده دستگاه قالب گیری بادی تزریقیشرکت اِوِر پاور (EVER POWER) دههها تخصص در ابزارسازی و فرآیند را در این مدل متمرکز کرده و دستگاهی را ارائه میدهد که در آن کل فرآیند بطری - از تزریق پیشفرم گرفته تا دمیدن نهایی و خروج آن - در یک چرخه واحد ماشین و بدون دخالت اپراتور، بدون انتقال مواد بین ماشینها و بدون ضایعات خط برش و جدایش که از ویژگیهای سیستمهای دمشی اکستروژن است، انجام میشود.
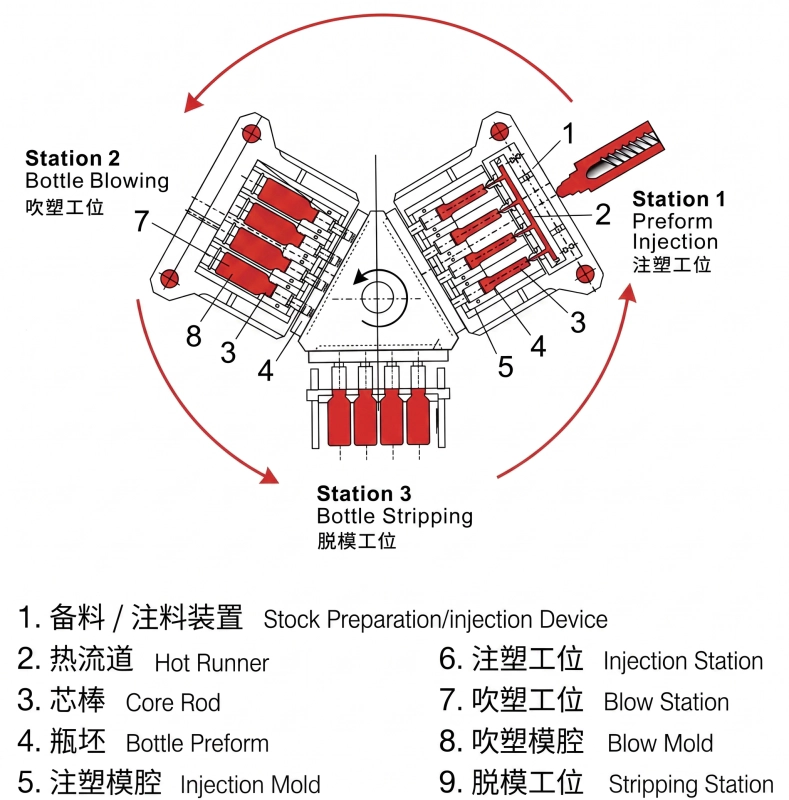
این دستگاه IBM تک مرحلهای is the preferred choice for pharmaceutical bottle blowing and cosmetic container manufacturing where dimensional consistency is non-negotiable. Each cycle on the EP60 runs three simultaneous operations: while new preforms are being injection-molded at Station 1, the previous batch is being blown to final shape at Station 2, and the completed bottles from Station 2 are being stripped and conveyed to the outfeed conveyor at Station 3. This triaxial parallelism means the productive output equals the injection cycle time alone - not the sum of injection plus blowing plus ejection - giving the EP60 a significant throughput advantage over two-stage stretch blow systems for small and medium volume containers.
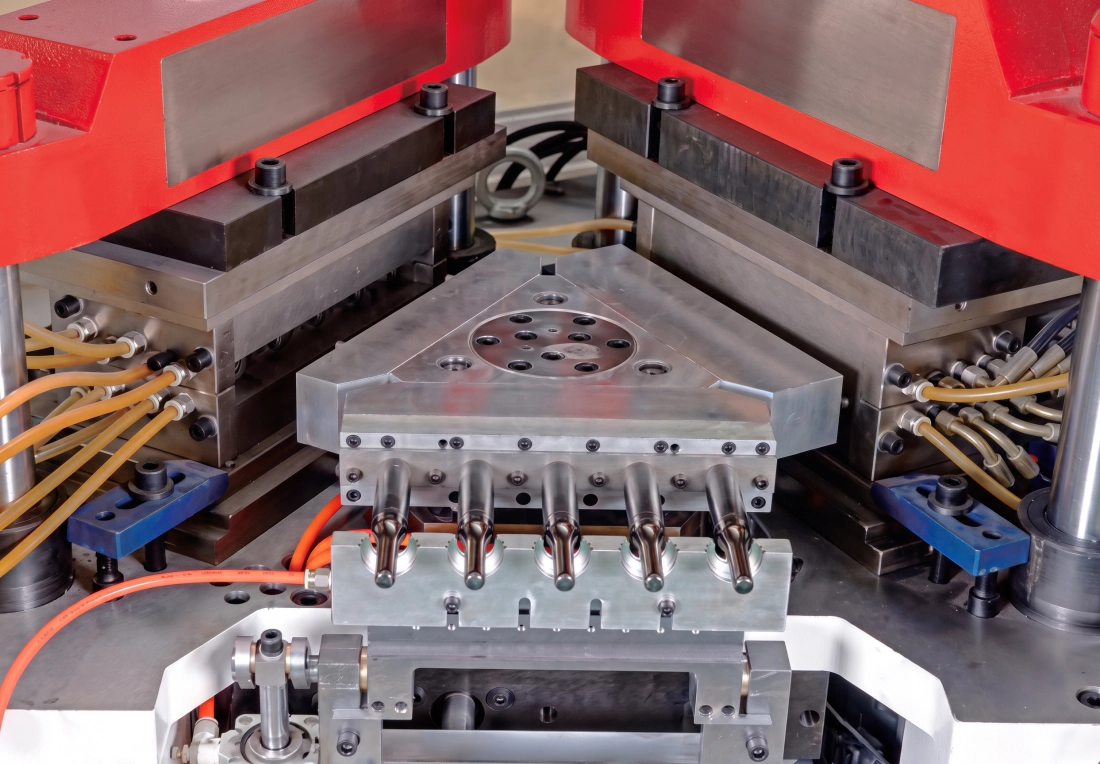
Three-Station Process: How the EP60 Works
ایستگاه ۱ - تزریق پریفرم
گرانولهای پلاستیکی در سیلندر ذوب شده و تحت فشار کنترلشده به داخل حفره تزریق تزریق میشوند. شکل دهانه بطری و هندسه رزوهها دقیقاً در قالب تزریق شکل داده میشوند. قالب تزریق باز میشود و مندرل که پیش فرم داغ را حمل میکند از طریق برجک دوار به ایستگاه ۲ منتقل میشود.
ایستگاه ۲ - قالبگیری بادی
پیش فرم داغ توسط هوای فشرده از هسته مندرل باد میشود. شکل بطری کاملاً توسط حفره قالب بادی تعیین میشود. هوا، پیش فرم را به سمت بیرون و در مقابل دیوارههای قالب خنک شده باد میکند و بطری ابعاد نهایی خود را به خود میگیرد. قالب باز میشود و برجک به سمت ایستگاه ۳ پیشروی میکند.
ایستگاه ۳ - تخلیه و انتقال
بطریهای نهایی و خنکشده از مندرلها جدا شده و روی نوار نقاله خروجی تخلیه میشوند. از آنجایی که هر سه ایستگاه به طور همزمان کار میکنند، این چرخه به طور مداوم تکرار میشود. هیچ عملیات ثانویه، پرس تخلیه و گرم کردن مجدد بطری مورد نیاز نیست - این سه عملیات یک چرخه زمانی مشترک دارند.
Main Technical Parameters - EVER POWER EP60
| پارامتر | مورد (EN) | واحد | ایپی۶۰ |
|---|---|---|---|
| سیستم تزریق | |||
| قطر پیچ | قطر پیچ | میلیمتر | ۴۵/۵۰ میلیمتر |
| نسبت طول به عمق (L/D) پیچ | پیچ L/D | - | 22:1 |
| وزن تزریق | وزن تزریق | گرم | 260/383 g |
| قدرت گرمایش | قدرت گرمایش | کیلو وات | 14 KW |
| مناطق گرمایش بشکه | تعداد مناطق بشکه | - | 3+N |
| سکته مغزی تزریق | سکته مغزی تزریق | میلیمتر | 160 mm |
| سیستم گیره | |||
| نیروی گیره تزریق | نیروی بستن تزریق | KN | 600 |
| سکته مغزی باز شدن تزریق | سکته مغزی برای تزریق | میلیمتر | ۱۴۰ میلیمتر |
| نیروی گیره ضربه | نیروی بستن دمیدن | KN | 100 |
| سکته مغزی باز شدن ضربه | سکته مغزی برای دمیدن | میلیمتر | ۱۴۰ میلیمتر |
| ارتفاع بالابر برج | ارتفاع بالابری میز دوار | میلیمتر | ۷۰ میلیمتر |
| قالب | |||
| حداکثر اندازه قالب (طول × عرض) | حداکثر اندازه صفحه (طول x عرض) | میلیمتر | 600x390 mm |
| ضخامت قالب | ضخامت قالب | میلیمتر | 240 mm |
| قطر حداکثر بطری | قطر بطری | میلیمتر | ۱۲۰ میلیمتر |
| حداکثر ارتفاع بطری | ارتفاع بطری | میلیمتر | ۲۲۰ میلیمتر |
| محدوده حجم بطری | حجم بطری مناسب | میلیلیتر | 1-2000 |
| سکته مغزی | سکته مغزی | میلیمتر | 230 mm |
| سیستم هیدرولیک | |||
| فشار هیدرولیک | فشار هیدرولیک | مگاپاسکال | 14 |
| قدرت موتور | قدرت موتور | کیلو وات | 18.5/22 KW |
| زمان چرخه خشک شدن | چرخه خشک | س | 4 |
| قدرت کل | قدرت کل | کیلو وات | 37 |
| قدرت عملیاتی | قدرت عملیاتی | % | 52-70 |
| پارامترهای دیگر | |||
| فشار هوای فشرده | حداقل فشار هوا | مگاپاسکال | 0.7-1.2 |
| ظرفیت هوا | ظرفیت هوای فشرده | متر مکعب در دقیقه | 0.7 |
| جریان آب خنک کننده | جریان آب | متر مکعب در ساعت | 4 |
| فشار آب خنک کننده | فشار آب خنک کننده | مگاپاسکال | 0.3-0.4 |
| ابعاد (طول x عرض x ارتفاع) | ابعاد کلی | م | 3.8x1.4x1.8 M |
| وزن خالص | وزن خالص | تن | 5 Ton |
توجه: همه پارامترها فقط برای مرجع هستند. شرکت EVER POWER حق تغییر مشخصات را به دلیل بهبود تجهیزات برای خود محفوظ میدارد.
Max Cavity Count per Container Volume (EP60 - For Reference)
| حجم | 10 میلی لیتر | 30 میلی لیتر | ۶۰ میلیلیتر | ۱۰۰ میلیلیتر | ۲۵۰ میلیلیتر | ۵۰۰ میلیلیتر | ۱۰۰۰ میلیلیتر |
|---|---|---|---|---|---|---|---|
| حفرههای حداکثری | 14 | 12 | 10 | 8 | 5 | 3 | 2 |
Core Hardware Architecture of the EP60
قاب فولادی کاملاً به سبک اروپایی
CNC-machined monolithic machine bed and platen mounts ensure parallelism between injection and blow clamping platens. Tie-bar surfaces are induction-hardened. The EP60 clamping force is 20-30% above equivalent-tonnage competitors due to the boosted pressurized clamping structure.
پیچ و بشکه دو فلزی
The plasticizing unit uses a bimetallic-lined barrel and a hardened alloy screw rated for glass-fiber and mineral-filled compounds. The EP60 screw diameter of 45/50 mm at 22:1 L/D delivers thorough homogenization with a 260/383 g shot capacity, covering the full range of bottle weights for this tonnage class.
کنترل هیدرولیک شیر تناسبی
فشار تزریق و فشار دمش هر دو از طریق شیرهای هیدرولیکی سروو-پروپورشنال تنظیم میشوند. این امر امکان پروفایل تزریق چند مرحلهای (سرعت پر شدن، تغییر حالت، فشار بستهبندی) را برای پریفرمهای دیواره نازک و کنترل دقیق شیب فشار دمش را فراهم میکند که نقصهای نوار شعاعی رایج در سیستمهای شیر دمش تک مرحلهای را از بین میبرد.
سیستم کنترل لمسی PLC
The EP60 control panel runs a full-color PLC touch-screen with parameter recipe storage. All process variables - temperatures, pressures, velocities, timings - are set and monitored from a single screen. Alarm history, production counters and fault codes are logged and displayed in real time.
سیستم راهگاه گرم بهینه شده
منیفولد راهگاه گرم قالب تزریق برای جریان صفر در منطقه مرده طراحی شده است و انحراف وزن گرم را در تمام حفرهها به حداقل میرساند. دقت کنترل دما تا مثبت یا منفی ۱ درجه از تخریب مواد حساس به گرما جلوگیری میکند و برای شفافیت مداوم در ظروف شفاف ضروری است.
طراحی ویژه میله هسته
The mandrels (core rods) feature internal cooling channels that reduce core temperature between the injection and blow stations, accelerating the cooling phase. Fast-cycle mandrels enable the EP60 to achieve a 4 S dry cycle without sacrificing preform cooling uniformity or dimensional stability.
قالبگیری بادی تزریقی در مقابل قالبگیری بادی اکستروژن: چرا IBM در زمینه ظروف دقیق برنده است؟
Buyers evaluating hollow container equipment often compare IBM and EBM on capital cost alone. The EP60 is more than a machine choice - it is a process choice that determines your long-term production economics and the quality ceiling your facility can achieve. The comparison below reflects real production differences that directly affect your cost per thousand bottles and your ability to win pharmaceutical and cosmetic supply contracts.
| خیر. | مورد مقایسه | دمش تزریقی (IBM) | دمش اکستروژن (EBM) |
|---|---|---|---|
| 1 | ثبات وزن بطری | تغییر وزن تقریباً 1% | تغییر وزن تقریباً ۳۱TP3T |
| 2 | یکنواختی ضخامت دیواره | ضخامت دیواره یکنواخت در سراسر | ضخامت دیواره متغیر است 10-20% |
| 3 | دهانه بطری / رزوه | بدون برق، بدون خط جدایش روی یقه | علامت برش، پایه و گردن ضعیف شده |
| 4 | تحدب پایه | تحدب مثبت قوی، پایه پایدار | تحدب ضعیف به دلیل جوش پینچ |
| 5 | ضایعات مواد | بدون ضایعات - بدون ضایعات و ضایعات | ضایعات 20-40% از پینچ فلش |
| 6 | قابلیت دیواره فوق نازک | برای دیوارهای بسیار نازک مناسب نیست | ضخامت دیواره از طریق کنترل کننده قابل تنظیم است |
| 7 | حساسیت محیطی | نسبت به تغییرات محیطی حساس نیست | نیاز به تنظیم مکرر |
| 8 | تعداد حفره و خروجی | کاویتاسیون بالا، بازده بالا، دهانه صاف | حفرههای کمتر، خروجی کمتر، گردن ناهموار |
| 9 | عمر و هزینه قالب | عمر طولانی قالب، مناسب برای تولید مداوم با تیراژ بالا | عمر کوتاهتر قالب، هزینه اولیه کمتر |
| 10 | ردپا | سیستم یکپارچه فشرده، فضای کم اشغال شده | تجهیزات کمکی بیشتر، مساحت کف بزرگتر |
| 11 | شکلدهی ظروف بیضیشکل | شکل دادن به شکلهای بیضی دشوارتر است | شکلدهی آسانتر به پروفیلهای بیضیشکل |
Application Fields and Container Types for the EP60
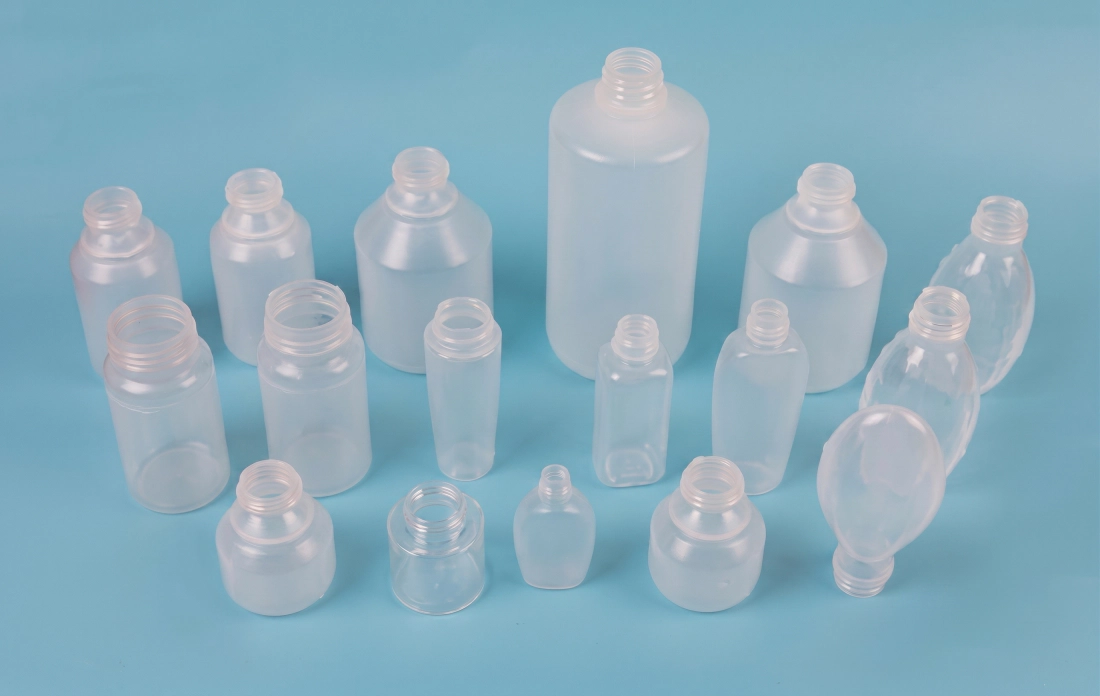
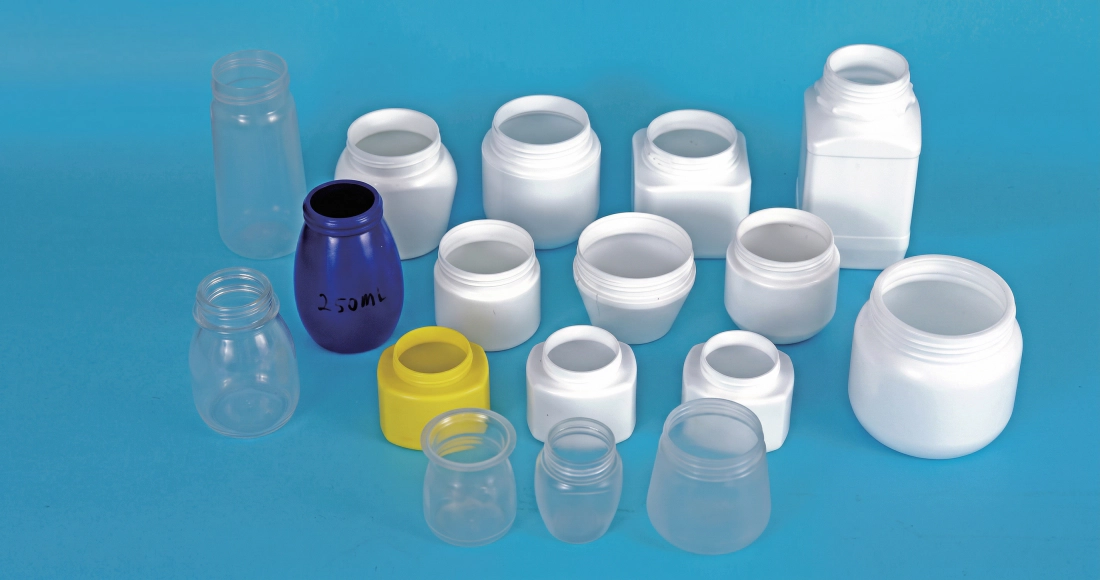
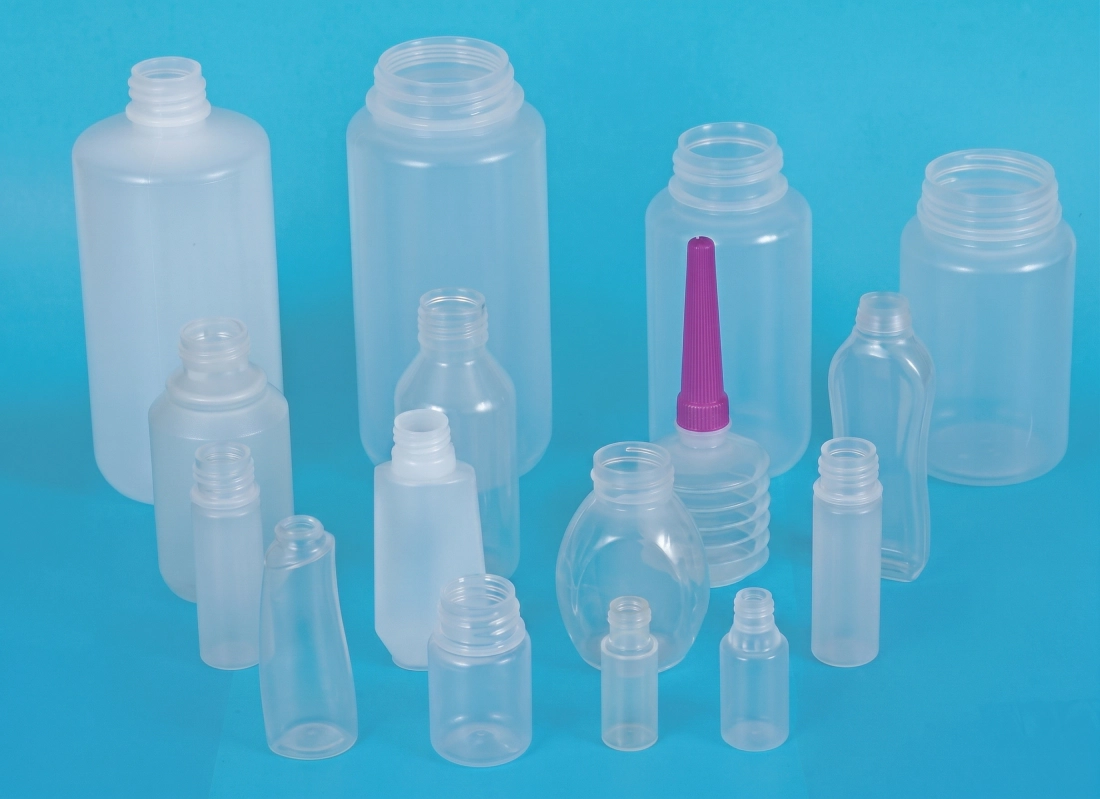
The EP60 is designed to produce bottles and containers from 1ml to the maximum volume for this model, covering the full range of primary packaging needs across four major market verticals. The table below shows the container types and industry segments where this تجهیزات قالب گیری بادی تزریقی اتوماتیک بالاترین بازده تجاری خود را ارائه میدهد.
صنعت داروسازی
- بطریهای قطره چشم (LDPE، ۵-۳۰ میلیلیتر)
- بطریهای قرص و کپسول خوراکی (HDPE، 30-500 میلیلیتر)
- اسپری بینی و بطریهای پمپی (PP)
- بطریهای دارویی مایع با دربهای مقاوم در برابر کودک
- ویالهای واکسن و معرف (LDPE، ۱-۲۰ میلیلیتر)
- بطریهای قرص HDPE سفید و کهربایی درجه GMP
صنعت لوازم آرایشی
- بطریهای رولی دئودورانت (PE، ۵۰-۱۰۰ میلیلیتر)
- تیوبها و بطریهای ریمل (PP، 5-20 میلیلیتر)
- بطریهای لاک ناخن (PS، 10-30 میلیلیتر)
- بطریهای پمپ لوسیون و سرم (PCTG، 30-200 میلیلیتر)
- شیشههای خامه دهان گشاد (PP/PS)
- بطریهای کرم پودر و تونر
محصولات و غذای کودک
- شیشه شیر کودک (PP، PPSU، ۱۵۰-۳۰۰ میلیلیتر)
- بطریهای مخصوص شیر خشک نوزاد
- ظروف عسل و شربت (LDPE)
- ظروف مخصوص نوشیدنی با حجم کم
- بطریهای نمونه روغن خوراکی
- بسته بندی ماست و لبنیات
مواد شیمیایی و صنعتی روزانه
- بطریهای شامپو و نرمکننده (HDPE/PP)
- دستگاه پخش کننده ضدعفونی کننده دست و لوسیون
- بطریهای نمونه سیال خودرو
- بطریهای کنسانتره مواد شیمیایی کشاورزی
- ظروف مواد شوینده
- بطریهای معرف صنعتی با دهانههای دقیق

Bottle Neck Tolerance and Sealing Integrity: Why IBM Precision Matters
The defining commercial advantage of one-step injection blow molding over extrusion blow is dimensional control at the bottle neck and thread finish. On the EP60, the neck and thread geometry is formed in the injection station under controlled cavity pressure - never stretched, never trimmed. The result is that inner and outer neck diameter tolerances can be held within 0.1mm across an entire production run of millions of units.
This matters profoundly for pharmaceutical packaging. Eye drop bottles, for example, must accept a calibrated dropper tip that delivers precisely 0.05ml per drop. A neck bore that varies by even 0.3mm causes the dropper to seat inconsistently, changing drop volume and potentially altering dosage. For aluminum foil induction-sealed pill bottles, the sealing flange must be flat and square to within tolerance for the foil to bond without micro-gaps - a condition the IBM process achieves consistently and EBM cannot guarantee without secondary trimming.
In premium cosmetics, roll-on deodorant applicators, mascara tubes and nail polish bottles all require thread-to-cap engagement that prevents both leakage and cross-threading. The EP60 produces a thread finish so accurate that 100% cap-seal integrity can be achieved at the filling line without leak-testing overhead. This is why leading cosmetic contract manufacturers specify IBM when they cannot afford the shrinkage and callback cost of even 0.1% leakage in a high-end fragrance or serum container.
Investment Return and Production Efficiency Analysis: Why Choose the EP60?
The acquisition cost of the EP60 must be evaluated against five measurable efficiency drivers that determine cost per thousand bottles and payback period. Purchasing engineers who evaluate only machine price - without these five factors - systematically undervalue the IBM platform and overestimate EBM economics for their target application.
۱. ضایعات فلش صفر
IBM هیچ ضایعات فلش و خط تولید اضافی تولید نمیکند. EBM در هر چرخه 20 تا 40% وزن بطری را به عنوان ضایعات تولید میکند. با 200 تن PP در سال، IBM بدون ضایعات، سالانه 40 تا 80 تن رزین صرفهجویی میکند. با 1500 دلار آمریکا در هر تن، یعنی 60 تا 120 هزار دلار آمریکا در سال در مواد اولیه صرفهجویی میشود، آن هم فقط از طریق یک دستگاه.
2. بدون نیاز به نیروی کار برای برق انداختن
EBM requires a secondary deflashing operation - either inline mechanical or manual - adding labor cost, a second machine footprint, and an additional quality failure point. IBM bottles from the EP60 come off the conveyor with zero post-processing required before filling or labeling, saving 1-3 operators per shift.
۳. توان عملیاتی کوتاه چرخه خشک
The EP60 achieves a 4 S dry cycle. With 10 cavities at 60ml, annual output at 6,000 hours run time exceeds 54.0 million bottles. This throughput concentration into a single compact machine reduces total asset investment per unit of capacity versus multi-machine EBM lines at equivalent output.
۴. تغییر سریع قالب
The injection mold and blow mold on the EP60 can be changed in 2-4 hours by a trained two-person team. Recipe recall from the PLC removes setup time entirely for repeat jobs. Facilities running 8-15 SKUs on a single EP60 achieve mold changeover frequency of 2-4 per week with total changeover downtime below 10% of available production hours.
ردپای مصرف و بهرهوری خدمات شهری
The EP60 footprint of 3.8x1.4x1.8 M consolidates injection, blow and ejection into a single machine envelope. Compare this to a two-machine EBM line (extruder plus blow machine, plus deflash press, plus conveyor) which typically occupies 3-4 times the floor area for equivalent throughput. Utility connections - compressed air at 0.7-1.2 MPa, cooling water at 4 M3/h flow, electrical connection at 37 KW total - are all single-point utilities, reducing installation complexity and ongoing maintenance overhead.
Factory building cost in pharmaceutical-grade cleanroom environments can reach 2,000-5,000 USD per square meter. The compact footprint of the EP60 directly reduces the cleanroom area required to produce a given volume of output - a capital benefit that does not appear in machine comparison tables but materially affects total project economics.
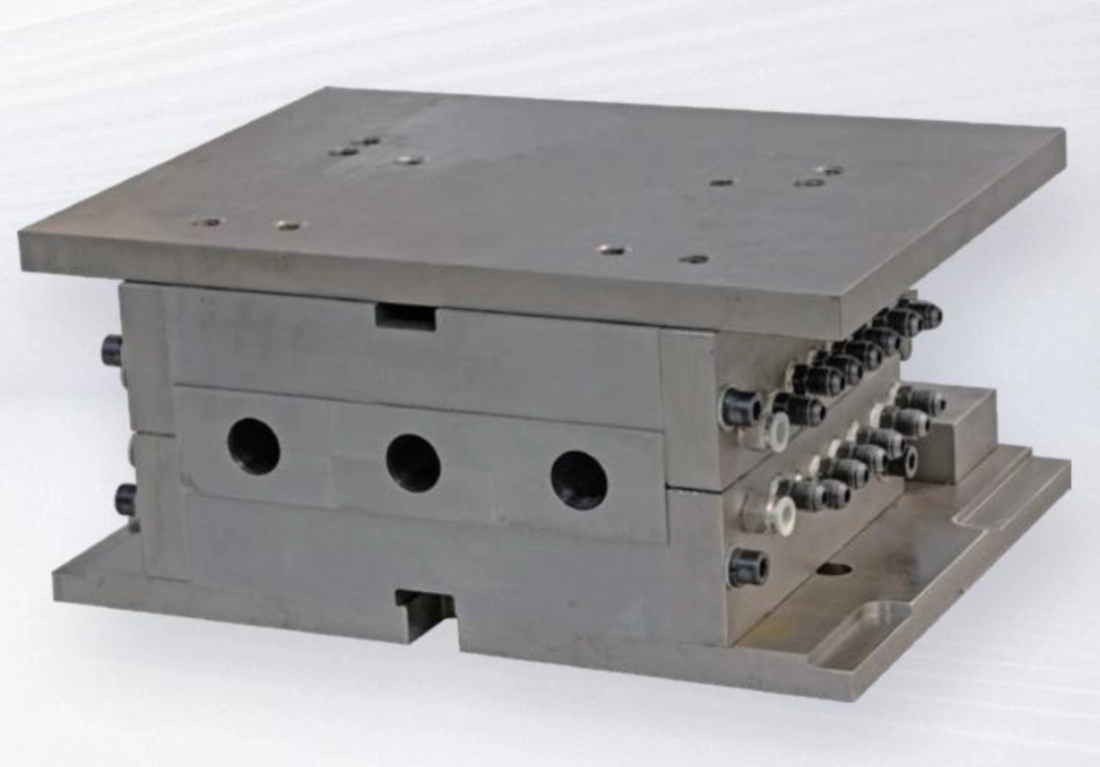
ویژگیهای قالب IBM سری EP و استانداردهای طراحی
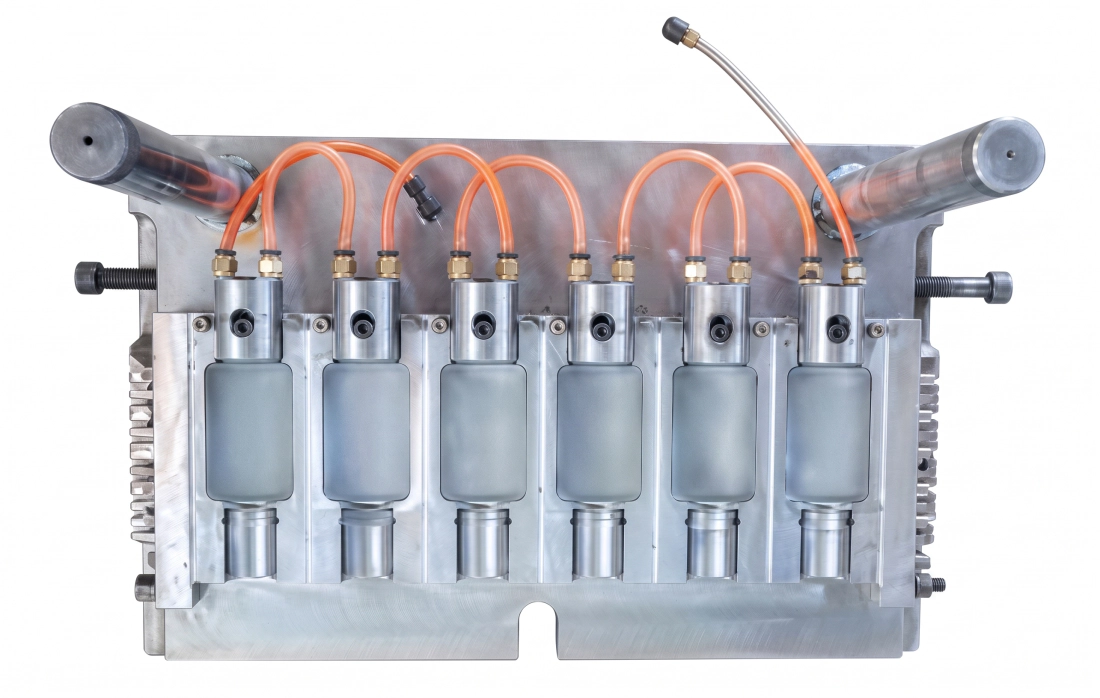
- ■طراحی حفره فعال و بلوک گردنی - حفرههای قالب تزریق و بلوکهای گردن به طور مستقل قابل تنظیم هستند و امکان تنظیم دقیق ابعاد بدنه لوله پیشفرم را بدون تعویض کل مجموعه قالب فراهم میکنند. مجاری روغن و آب به طور خاص برای توزیع پایدار دما و جداسازی آسان طراحی شدهاند.
- ■گریدهای فولادی ممتاز - بدنههای قالب تزریق از فولاد ضد زنگ 4Cr13 یا فولاد آلیاژی S136 با استحکام بالای وارداتی استفاده میکنند. S136 فولادی با جلای آینهای و مقاوم در برابر خوردگی با سختی 52 HRC است. بدنههای قالب دمشی را میتوان از آلیاژ منیزیم-آلومینیوم برای رسانایی حرارتی برتر و کاهش جرم اینرسی روی برجک چرخشی تولید کرد.
- ■طراحی بهینه راهگاه گرم و پیش فرم - منیفولد راهگاه گرم به گونهای مهندسی شده است که انحراف وزن گرم را در تمام حفرهها به حداقل برساند و تغییر ضخامت دیواره را در بدنه پیشساز کاهش دهد. طراحی مندرل، تحویل یکنواخت هوا را برای انبساط مداوم ضربه و خنکسازی سریع تضمین میکند.
- ■ابعاد دقیق رزوه گردن و آببند - قطر داخلی و خارجی دهانه بطری، گام رزوه و هندسه فلنج با توجه به تلرانس کششی ماشینکاری میشوند. نرخ آببندی درب در نمونههای تولیدی 100% است.
- ■بدون فلش در گردن و پایه - the IBM process geometry eliminates parting-line flash at the bottle mouth and pinch-weld flash at the base. Bottles exit the EP60 with no trimming required at either end.
- ■معیارهای سازگاری محصول - اندازه، وزن، موقعیت خط جدایش و ضخامت دیواره در تمام حفرهها و در بین دستههای تولیدی ثابت است، که مشتریان دارویی را قادر میسازد تا تولید را بر اساس آمار در هر دسته بدون سربار بازرسی 100% اعتبارسنجی کنند.
Equipment Selection Guide: Is the EP60 Right for Your Production Requirements?
Selecting the correct IBM tonnage requires calculating the intersection of three variables: preform weight, required cavity count, and target output per hour. Use this framework to confirm whether the EP60 is correctly sized for your application, or to understand what production parameters it can support.
مرحله 1: محاسبه وزن پیش فرم
Take the target bottle weight in grams (including the neck, body and base). Add 2-5% for process cushion. The EP60 injection weight of 260/383 g must be equal to or greater than (target preform weight x number of cavities). For example: a 5g preform at 8 cavities requires 40g shot weight, well within the 260/383 g capacity.
مرحله 2: محاسبه تعداد حفره مورد نیاز
Target output (bottles/hour) divided by (3600 seconds / cycle time in seconds) gives required cavities. At a 4 S cycle and 10,000 bottles per hour target: 10,000 / (3600 / 4) = 12 cavities minimum. Cross-check against the cavity table above to confirm the EP60 can deliver this at your bottle volume.
مرحله 3: بررسی تناسب صفحات قالب
The injection mould layout (cavity array footprint) must fit within the EP60 max platen size of 600x390 mm. Wide-bottle (diameter greater than 120mm) or tall-bottle (height greater than 220mm) applications exceed the EP60 mould envelope and require a larger model. Confirm your bottle OD and height before specifying cavity count.
مرحله ۴: مواد و فشار تزریق
PP requires higher injection pressure and melt temperature than LDPE. PC and PETG require even higher barrel temperatures and longer residence-time plasticization. The EP60 hydraulic system pressure of 14 MPa and motor of 18.5/22 KW supports the injection forces needed for PP and engineering grade materials at the rated injection weight. Confirm your resin specification with the EVER POWER application team before ordering.
EVER POWER application engineers provide free pre-sales technical consultation to validate your container dimensions, material, cavity count and production target against EP60 specifications. Contact us with your bottle drawing and production brief for a written confirmation of suitability.
بررسی اجمالی ساختار ماشین و دستورالعملهای نگهداری
The EP60 is built around three core functional modules. Understanding their maintenance requirements is essential for sustaining the machine performance metrics - dry cycle, output rate, and product quality - over the full production life of the equipment.
ماژول ۱ - واحد تزریق: مارپیچ، سیلندر، راهگاه گرم
واحد تزریق، پلاستیک را ذوب کرده و به داخل حفره پیشفرم هدایت میکند. نگهداری روزانه: پروفیلهای دمای سیلندر را در مقایسه با نقاط تنظیم شده بررسی کنید، نوک پیچ و حلقه را از نظر شاخصهای سایش بررسی کنید و قبل از شروع به کار، مطمئن شوید که دمای ناحیه راهگاه گرم در محدوده ۲ درجه از نقاط تنظیم شده باشد. هفتگی: نوارهای عایق سیلندر را بررسی کنید، آببندیهای سیلندر تزریق را از نظر نشت روغن بررسی کنید و هرگونه آلودگی رنگی از تولید قبلی را پاک کنید. ماهانه: حلقه بررسی و مجموعه نوک پیچ را بکشید و تمیز کنید؛ پرههای پیچ را از نظر سایش بررسی کنید و قطر سوراخ سیلندر را برای میزان فضای خالی اندازهگیری کنید. اگر فضای خالی بیش از حد مجاز سازنده باشد، سیلندر را تعویض کنید تا از عبور مذاب و ناهماهنگی وزن تزریق جلوگیری شود.
روش پاکسازی: هنگام تغییر رنگ از تیره به روشن یا از رزین مهندسی به رزین معمولی، از یک ترکیب پاکسازی تجاری در دمای بشکه 10 درجه بالاتر از نقطه تنظیم ماده جدید استفاده کنید. قبل از تغییر به ماده جدید، 5 تا 10 شات پاکسازی انجام دهید. هرگز بشکه را بیش از 20 دقیقه بدون پاکسازی در دمای فرآیند رها نکنید - تخریب حرارتی در طول دورههای بیکاری علت اصلی آلودگی لکههای سیاه هنگام راهاندازی مجدد است.
ماژول ۲ - واحد گیره و نمایهسازی چرخشی
سیستم گیره و ایندکسر چرخشی بیشترین بارهای مکانیکی را تحمل میکنند و دقیقترین الزامات موقعیتی را دارند. روزانه: سطوح میله اتصال و ریلهای راهنمای میز چرخشی را طبق برنامه روانکاری گریس بزنید (EVER POWER درجه گریس را مشخص میکند - با گریس عمومی جایگزین نکنید، زیرا ممکن است ویسکوزیته را در دمای عملیاتی حفظ نکند). سیلندر گیره هیدرولیکی را از نظر نشت روغن در آببندی میله بررسی کنید. در طول چرخش ایندکسر به صداهای غیرمعمول گوش دهید - هرگونه صدای کلیک یا مکث فلزی نشان دهنده یاتاقان جداکننده زاویهای است که نیاز به بازرسی دارد.
ماهانه: موازی بودن صفحه را با یک نشانگر عقربهای در چهار موقعیت میله اتصال بررسی کنید؛ انحراف بیش از 0.05 میلیمتر نیاز به شیمگذاری مجدد دارد. دقت موقعیت شاخصگذاری را با قرار دادن یک نشانگر عقربهای در مقابل یک سطح مرجع روی برجک بررسی کنید و تأیید کنید که همان موقعیت پس از 100 چرخه شاخصگذاری متوالی با دقت 0.02 میلیمتر تکرار میشود. در صورت مشاهده رانش، توقف مکانیکی را تنظیم کنید یا با خدمات EVER POWER تماس بگیرید.
ماژول ۳ - سیستم هیدرولیک و مدار خنککننده
The hydraulic system is the energy backbone of the EP60. System pressure is set at 14 MPa. Daily: check hydraulic oil level in the tank sight glass, check oil temperature display (normal operating range 40-55 degrees Celsius; above 60 degrees indicates a cooling circuit problem or filter blockage), and inspect all visible hydraulic hose fittings for weeping. The oil filter indicator must be checked every 250 hours - a red indicator requires immediate filter element replacement, not deferral.
Cooling circuit: the EP60 requires clean, scale-free cooling water at 0.3-0.4 MPa pressure and 4 M3/h flow. Install a water treatment system upstream of the machine to prevent calcium scale buildup inside mold cooling channels. Scale buildup of just 1mm in a 6mm channel reduces cooling efficiency by over 30%, extending cycle times and reducing output. Flush cooling circuits with a descaling solution annually. Chiller water quality must be neutral pH (6.5-7.5) and contain an anti-corrosion inhibitor compatible with copper and aluminum alloy mold materials.
راهکارهای آماده تحویل و خدمات سفارشیسازی از EVER POWER
EVER POWER supplies the EP60 as either a standalone machine or as the centerpiece of a complete turnkey bottle production line. For customers setting up a new facility or expanding into a new container product line, the turnkey approach eliminates the integration risk that comes from sourcing the IBM machine, molds, auxiliaries, and downstream equipment from separate vendors.
طراحی و ساخت قالب
مهندسان EVER POWER مجموعه قالبهای تزریق و دمشی را از روی نقشههای بطری مشتری یا فایلهای سهبعدی توسعه میدهند. قالبهای راهگاه گرم چند حفرهای از جنس فولاد S136 یا 4Cr13. نمونه اولیه قالبهای تک حفرهای برای اعتبارسنجی کانتینر قبل از اقدام به تولید با حفره بالا. آزمایشهای قالب T0 قبل از ارسال در کارخانه انجام میشود.
ادغام تجهیزات کمکی
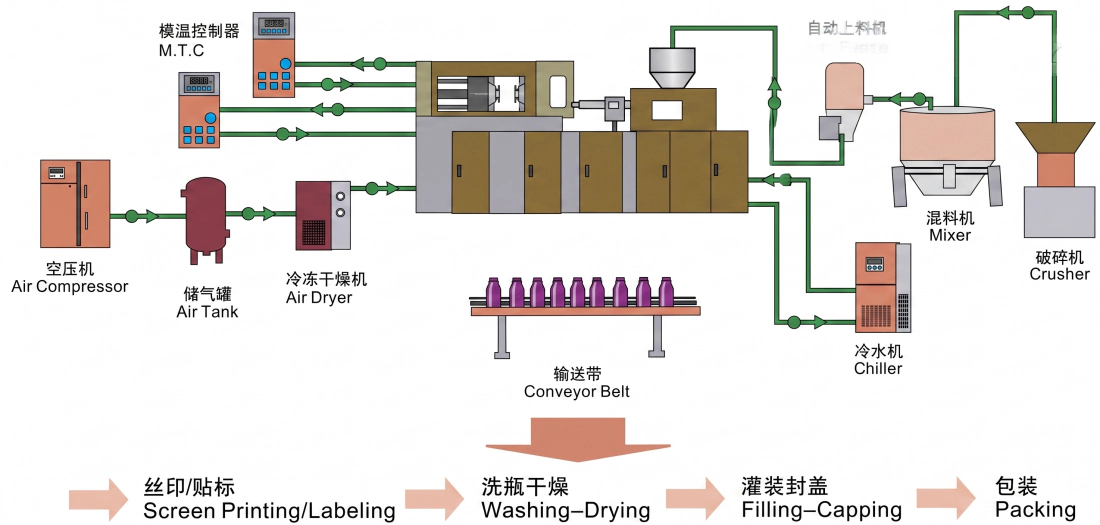
The EVER POWER turnkey line includes: screw air compressor, air tank and air dryer, mold temperature controller, industrial chiller, auto loader, conveyor belt, screen printing and labeling system, washing and drying line, and automatic filling and capping machines. All auxiliary equipment is specified and pre-integrated to match the EP60 output rate.
سیستمهای کیفیت پاییندستی
Optional inline bottle visual inspection machine (machine vision system for flash, deformation and contamination detection), automatic leak tester, automatic packing machine, and carton erector. For pharmaceutical lines, 100% inline leak testing and vision inspection are available as integrated modules matched to the EP60 conveyor output speed.
پیکربندی GMP و اتاق تمیز
برای مشتریان دارویی که به تولید در سطح GMP نیاز دارند، EVER POWER سفارشیسازی دستگاه را ارائه میدهد، از جمله: روانکاری سیستم بسته برای جلوگیری از آلودگی ناحیه محصول، محفظههای ایمنی از جنس استیل ضد زنگ، محفظه دستگاه با فیلتر HEPA برای سازگاری با اتاق تمیز کلاس ۱۰۰۰۰۰ و پشتیبانی اسناد برای پروتکلهای صلاحیت تجهیزات (IQ/OQ/PQ).
Auxiliary Equipment Available with the EP60

استانداردهای کنترل کیفیت و تولید
ماشینکاری CNC قطعات بحرانی
بستر ماشین، صفحات گیره و تمام سطوح دقیق با استفاده از دستگاه CNC در تنظیمات تکی ساخته میشوند تا دقت هندسی تضمین شود. موازی بودن صفحات با اندازهگیری لیزری تا 0.02 میلیمتر تأیید میشود. سوراخهای میله اتصال برای انطباق بدون تداخل با یاتاقان، تا تلرانس H7 صیقل داده شدهاند.
سختکاری القایی میلگرد مهاری
میلگردهای مهاری تحت سختکاری القایی با فرکانس بالا قرار میگیرند تا به سختی سطحی ۵۲-۵۸ HRC برسند و سپس سنگزنی دقیقی روی آنها انجام میشود. این عملیات سطحی، مقاومت در برابر سایش را در برابر تماس لغزشی مکرر صفحات گیره در طول میلیونها چرخه بدون ایجاد ساییدگی یا فرخوردگی فراهم میکند.
تمیزی مدار هیدرولیک
تمام مدارهای هیدرولیک قبل از مونتاژ، شستشو، آزمایش فشار و شمارش ذرات انجام میشوند. حداقل میزان تمیزی روغن هیدرولیک در استاندارد ISO 4406 کلاس 17/15/12 حفظ میشود. حساسیت به آلودگی شیرهای پروپرشنال و سروو به این سطح از تمیزی نیاز دارد تا از چسبندگی قرقره شیر و رانش کنترل جلوگیری شود.
آزمایش ۷۲ ساعته کارکرد در کارخانه
Every EP60 undergoes a minimum 72-hour continuous loaded run test at the factory before shipment. During this period, production output samples are measured for weight consistency, wall thickness uniformity, and dimensional accuracy. Any parameter outside specification triggers a hold and corrective action before the machine is cleared for delivery.
انطباق با ایمنی CE
The EP60 is CE-marked in compliance with EU Machinery Directive requirements. Safety features include: interlocked safety doors with hydraulic circuit interrupt, light curtain protection at the operator access zone, emergency stop at all operator positions, and two-hand operator control for manual mold setting. CE documentation is provided with every machine.
خدمات پس از فروش و پشتیبانی فنی
نصب و راه اندازی
مهندسان ارشد EVER POWER مسئول نصب، راهاندازی و آزمایشهای پذیرش هستند. مهندس تا زمانی که دستگاه به حالت تولید پایدار برسد، در محل باقی میماند و همه اپراتورها در مورد نحوه کار با دستگاه، تعویض قالب و نگهداری معمول آموزش میبینند. معیارهای پذیرش قبل از ارسال توافق شده و در گزارش راهاندازی مستند میشوند.
برنامه نگهداری پیشگیرانه
شرکت EVER POWER یک سرویس یادآوری تعمیر و نگهداری برنامهریزیشده برای تمام دستگاههای در حال کار ارائه میدهد. تقویم تعمیر و نگهداری، وظایف روزانه، هفتگی، ماهانه و سالانه را پوشش میدهد. تعمیر و نگهداری پیشگیرانه از خرابیهای برنامهریزی نشده جلوگیری میکند و نیاز به ارسال قطعات یدکی اضطراری و گرانقیمت را کاهش میدهد. مشتریانی که برنامه تعمیر و نگهداری پیشگیرانه را دنبال میکنند، به طور مداوم در دسترس بودن دستگاه را بالاتر از 95% گزارش میدهند.
خط تلفن خدمات 24x7
خط تلفن خدمات EVER POWER به صورت 24 ساعته و 7 روز هفته در دسترس است. برای رفع مشکلات فوری تولید، با خط خدمات تماس بگیرید یا پیام دهید تا یک مهندس واجد شرایط ظرف 2 ساعت برای تشخیص مشکل از راه دور پاسخ دهد. در صورت نیاز به خدمات در محل، EVER POWER یک تکنسین را با حداقل زمان پاسخگویی موجود برای محل شما اعزام میکند.
موجودی قطعات یدکی
EVER POWER maintains a comprehensive spare parts inventory for all EP60 components including hydraulic seals, proportional valve cartridges, heating bands, temperature sensors, drive belts and electrical components. Parts can be shipped globally within 48 hours for items in stock. Critical fast-wear items are available for customer-held local inventory based on EVER POWER recommendations.
برنامههای آموزش فنی
فراتر از آموزش نصب استاندارد، EVER POWER ماژولهای آموزشی اختصاصی ارائه میدهد: عملیات دستگاه، بهینهسازی فرآیند قالب، تعویض و راهاندازی قالب، نگهداری سیستم هیدرولیک و عیبیابی فرآیند برای مواد خاص مانند PP، LDPE و PCTG. آموزش میتواند در کارخانه EVER POWER یا در محل مشتری انجام شود.
Frequently Asked Questions - EVER POWER EP60
What materials can the EP60 process?
The EP60 is compatible with HDPE, LDPE, PP, PS (including lactic acid bacteria grade transparent PS), ABS, EVA, bio-based corn material, PCTG, and similar thermoplastics. For engineering resins such as PC, PETG and Tritan, the screw L/D of 22:1 and the 3+N heating zones provide the residence time and temperature profile needed for thorough, degradation-free plasticization. Confirm your resin grade with EVER POWER application engineering before ordering.
Can the EP60 be used for pharmaceutical GMP production?
Yes. The EP60 can be configured for pharmaceutical GMP production environments. Key features supporting GMP include: the one-step process eliminates inter-machine bottle transfer that introduces contamination risk in two-stage systems; the closed lubrication system prevents lubricant contamination of the product zone; and the machine can be specified with a stainless steel safety enclosure suitable for cleanroom installation. EVER POWER can provide equipment documentation to support IQ/OQ/PQ qualification processes for pharmaceutical facility validation.
How long does mould changeover take on the EP60?
A trained two-person team can complete a full mold changeover (injection mold, blow mold, and mandrel set) on the EP60 in approximately 2-4 hours, depending on the mold design and the changeover frequency experience of the team. PLC recipe recall eliminates parameter re-entry time for repeat mold sets. Facilities that invest in quick-release clamping plates for the mold base can reduce changeover to under 2 hours.
What certifications does the EP60 carry?
The EP60 is CE-marked for the European market. The machine design complies with EU Machinery Directive safety requirements including interlocked guards, emergency stop systems, and electrical safety standards. EVER POWER is an ISO-certified manufacturer. Machine documentation is provided in English and can be supplied in other languages upon request for export markets.
What is the lead time for the EP60 and an associated mould set?
Standard machine lead time for the EP60 is 45-75 days from order confirmation and deposit receipt, depending on production schedule at time of order. Mold sets are typically supplied in 60-90 days from final confirmation of bottle drawings and material specification. The machine and mold sets can be scheduled to arrive simultaneously for a coordinated installation. Contact EVER POWER for current lead time at time of inquiry.
Ready to Specify the EVER POWER EP60 for Your Production Line?
نقشه بطری، حجم مورد نظر، مشخصات مواد و میزان خروجی مورد نیاز در ساعت را برای تیم مهندسی کاربردی ما ارسال کنید. ما تعداد حفرههای صحیح و پیکربندی دستگاه را کتباً تأیید کرده و ظرف 3 روز کاری یک پیشنهاد تجاری دقیق ارائه خواهیم داد.
توضیحات تکمیلی
| ویرایش شده | توسط hamishe |
|---|
محصولات مرتبط
-
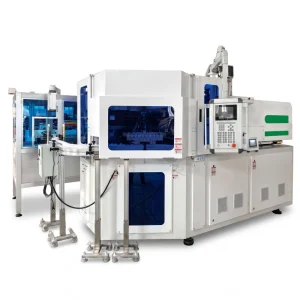
ماشین قالبگیری بادی تزریقی تمام برقی پرسرعت EP60HE، سیکل هیدرولیک صفر، 2.5 ثانیه
-
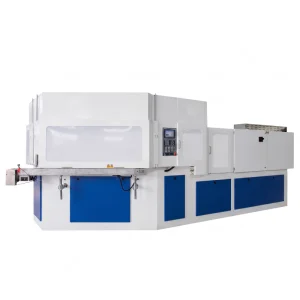
دستگاه قالبگیری بادی تزریقی سنگین EP135 1350KN IBM با حفره بالا برای بطریهای دارویی آرایشی
-
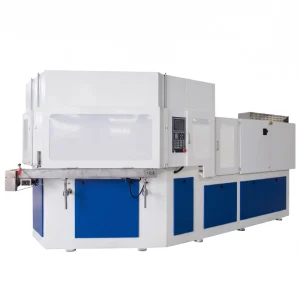
دستگاه قالب گیری تزریقی صنعتی EP110 1100KN تجهیزات IBM اتوماتیک برای بطری های با حجم زیاد
-
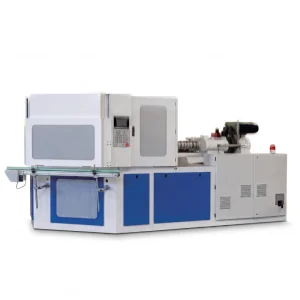
دستگاه قالبگیری بادی تزریقی با خروجی بالا، تجهیزات قالبگیری بطری بدون فلش EP80 800KN
-
دستگاه قالب گیری بادی تزریقی تک مرحله ای اتوماتیک EP40 400KN برای بطری های آرایشی دارویی CE ISO


