
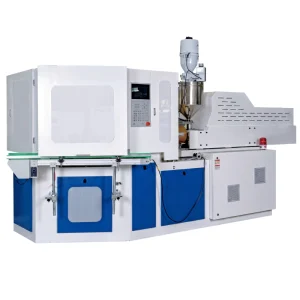
அழகுசாதனப் பொருட்கள் மற்றும் மருந்துப் புட்டிகளுக்கான கனரக ஊசி ஊது அச்சு இயந்திரம் EP135 1350KN உயர்-குழி IBM

EVER POWER EP135 injection blow molding machine offers 1350KN clamping force, 650g injection weight, up to 30 cavities at 10ml – the highest output in the EP series. Dual servo hydraulic system, high-precision angle divider, 200KN blow clamping force. Produces 1-2000ml bottles for pharma, cosmetics and chemical packaging. 18 Ton, 95KW total power. CE ISO.
What Is the EVER POWER EP135 One-Step Injection Blow Molding Machine?
The EVER POWER EP135 is a fully automatic one-step IBM (Injection Blow Molding) machine engineered for precision hollow container production. As a dedicated injection blow molding machine manufacturerஎவர் பவர், தனது பல பத்தாண்டுகால கருவியமைப்பு மற்றும் செயல்முறை நிபுணத்துவத்தை இந்த மாடலில் ஒருமுகப்படுத்தியுள்ளது. இதன் மூலம், இயக்குபவரின் தலையீடு இன்றியும், இயந்திரங்களுக்கு இடையில் மூலப்பொருள் பரிமாற்றம் இன்றியும், மற்றும் எக்ஸ்ட்ரூஷன் ப்ளோ அமைப்புகளில் காணப்படும் பிளாஷ் மற்றும் ப்ரிட்டிங்-லைன் விரயம் இன்றியும், ப்ரீஃபார்ம் உட்செலுத்துதல் முதல் இறுதி ஊதுதல் மற்றும் வெளியேற்றுதல் வரையிலான முழு பாட்டில் உருவாக்கமும் ஒரே இயந்திர சுழற்சியில் நிறைவடையும் ஒரு இயந்திரத்தை வழங்கியுள்ளது.
இது ஒரு படி ஐபிஎம் இயந்திரம் is the preferred choice for pharmaceutical bottle blowing and cosmetic container manufacturing where dimensional consistency is non-negotiable. Each cycle on the EP135 runs three simultaneous operations: while new preforms are being injection-molded at Station 1, the previous batch is being blown to final shape at Station 2, and the completed bottles from Station 2 are being stripped and conveyed to the outfeed conveyor at Station 3. This triaxial parallelism means the productive output equals the injection cycle time alone - not the sum of injection plus blowing plus ejection - giving the EP135 a significant throughput advantage over two-stage stretch blow systems for small and medium volume containers.
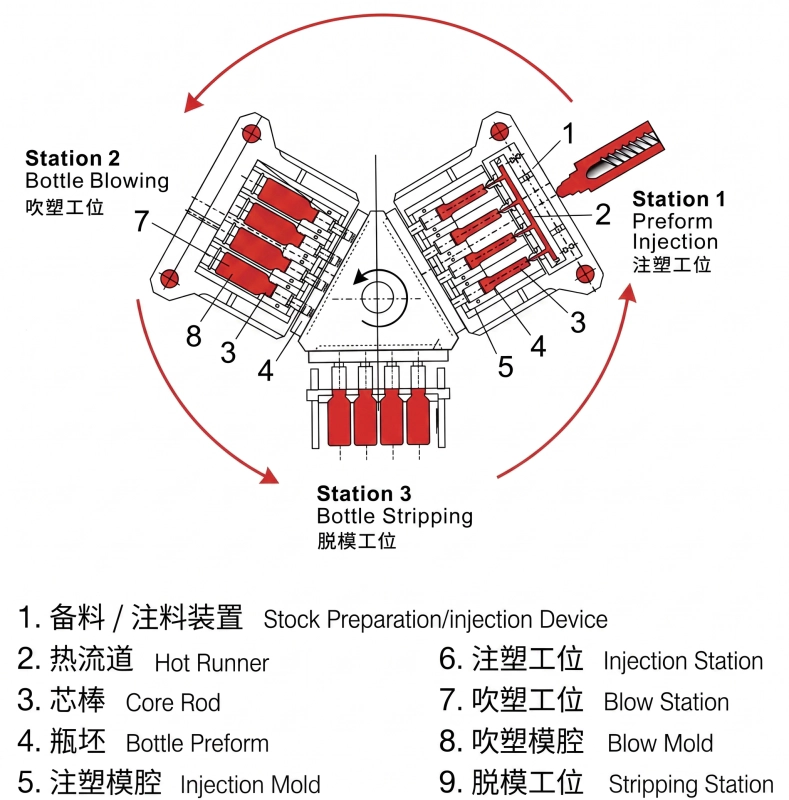
Three-Station Process: How the EP135 Works
நிலையம் 1 - முன்வடிவ ஊசி
பிளாஸ்டிக் துகள்கள் பீப்பாயில் உருக்கப்பட்டு, கட்டுப்படுத்தப்பட்ட அழுத்தத்தில் உட்செலுத்துக் குழிக்குள் செலுத்தப்படுகின்றன. புட்டியின் கழுத்து மற்றும் திருகு வடிவவியல் ஆகியவை உட்செலுத்து அச்சில் துல்லியமாக உருவாக்கப்படுகின்றன. உட்செலுத்து அச்சு திறக்க, சூடான முன்வடிவத்தைத் தாங்கிய அச்சு, சுழலும் கோபுரத்தின் வழியாக நிலையம் 2-க்கு மாற்றப்படுகிறது.
நிலையம் 2 - ஊது அச்சு
அச்சுக் கோளத்திலிருந்து வரும் அழுத்தப்பட்ட காற்றால் சூடான முன்வடிவம் ஊதப்படுகிறது. புட்டியின் வடிவம் முழுவதுமாக ஊது அச்சுக் குழியால் தீர்மானிக்கப்படுகிறது. காற்றானது, குளிர்விக்கப்பட்ட அச்சுச் சுவர்களுக்கு எதிராக முன்வடிவத்தை வெளிப்புறமாக ஊதுகிறது, மேலும் புட்டி அதன் இறுதிப் பரிமாணங்களை அடைகிறது. அச்சு திறக்கிறது, மேலும் சுழல் கோபுரம் நிலையம் 3-ஐ நோக்கி முன்னேறுகிறது.
நிலையம் 3 - வெளியேற்றுதல் மற்றும் கடத்துதல்
தயாரிக்கப்பட்டு, குளிர்விக்கப்பட்ட புட்டிகள் அச்சுகளிலிருந்து பிரிக்கப்பட்டு, வெளிச்செல்லும் கன்வேயரில் வெளியேற்றப்படுகின்றன. மூன்று நிலையங்களும் ஒரே நேரத்தில் செயல்படுவதால், இந்தச் சுழற்சி தொடர்ச்சியாக மீண்டும் மீண்டும் நிகழ்கிறது. இரண்டாம் நிலைச் செயல்பாடோ, ஃப்ளாஷ் நீக்கும் இயந்திரமோ, அல்லது புட்டிகளை மீண்டும் சூடாக்குவதோ தேவையில்லை - இந்த மூன்று செயல்பாடுகளும் ஒரே சுழற்சி நேரத்தைப் பகிர்ந்து கொள்கின்றன.
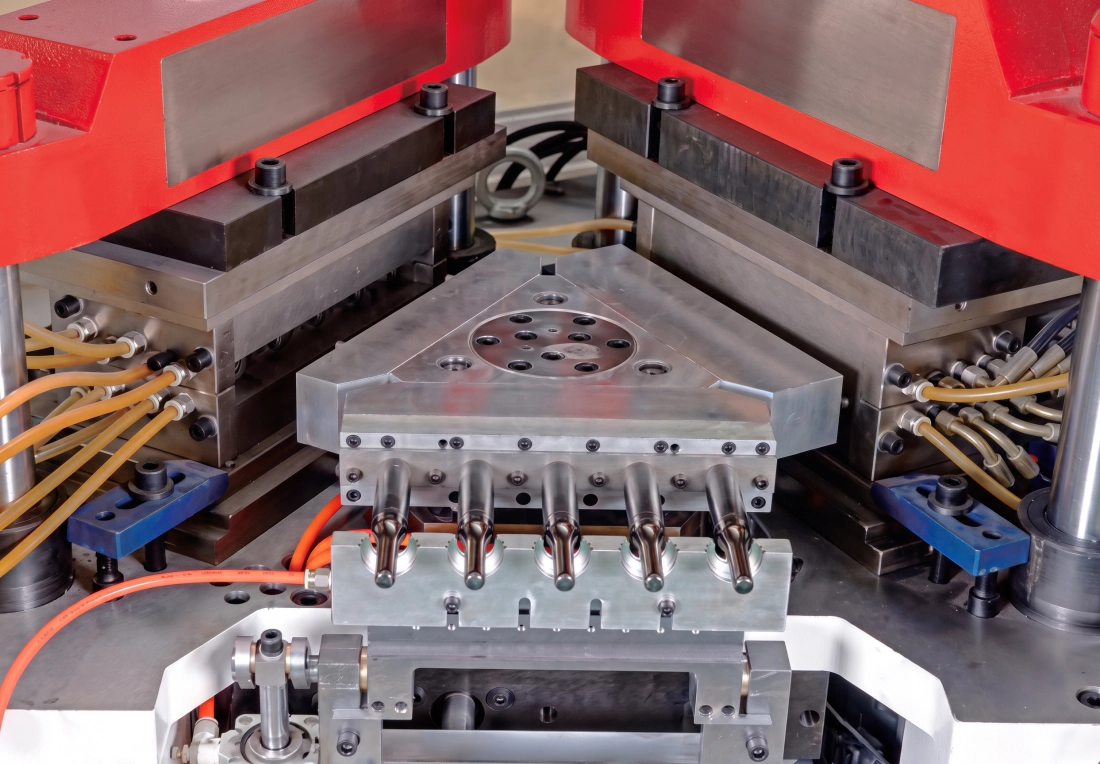
Main Technical Parameters - EVER POWER EP135
| அளவுரு | பொருள் (ஆங்கிலம்) | அலகு | EP135 |
|---|---|---|---|
| ஊசி அமைப்பு | |||
| திருகு விட்டம் | திருகு விட்டம் | மிமீ | 70 மிமீ |
| திருகு L/D விகிதம் | திருகு L/D | - | 22:1 |
| ஊசி எடை | ஊசி எடை | ஜி | 650 g |
| வெப்பமூட்டும் சக்தி | வெப்பமூட்டும் சக்தி | கே.டபிள்யூ. | 30 KW |
| பீப்பாய் வெப்பமூட்டும் மண்டலங்கள் | பீப்பாய் மண்டலங்களின் எண்ணிக்கை | - | 6+N |
| ஊசி போடும் அடி | ஊசி போடும் அடி | மிமீ | 200 mm |
| இறுக்கும் அமைப்பு | |||
| ஊசி இறுக்க விசை | ஊசி செலுத்துதலின் இறுக்கும் விசை | கே.என். | 1350 |
| ஊசி திறப்பு வீச்சு | ஊசி போடுவதற்கான தொடக்க அசைவு | மிமீ | 140 மிமீ |
| ஊது இறுக்க விசை | ஊதுதலின் இறுக்கும் விசை | கே.என். | 200 |
| அடி திறப்பு வீச்சு | ஊதுவதற்கான தொடக்க அசைவு | மிமீ | 140 மிமீ |
| கோபுரத்தின் உயரம் | சுழலும் மேசையின் தூக்கும் உயரம் | மிமீ | 70 மிமீ |
| அச்சு | |||
| அதிகபட்ச பிளேட்டன் அளவு (நீளம் x அகலம்) | அதிகபட்ச பிளேட்டன் அளவு (நீளம் x அகலம்) | மிமீ | 1300x500 mm |
| அச்சு தடிமன் | அச்சு தடிமன் | மிமீ | 280 மிமீ |
| அதிகபட்ச பாட்டில் விட்டம் | பாட்டிலின் விட்டம் | மிமீ | 120 மிமீ |
| மேக்ஸ்பாட்டில் உயரம் | பாட்டில் உயரம் | மிமீ | 220 மிமீ |
| பாட்டில் கொள்ளளவு வரம்பு | பொருத்தமான பாட்டில் அளவு | எம்.எல். | 1-2000 |
| ஸ்ட்ரிப்பிங் ஸ்ட்ரோக் | ஸ்ட்ரிப்பிங் ஸ்ட்ரோக் | மிமீ | 280 மிமீ |
| ஹைட்ராலிக் அமைப்பு | |||
| ஹைட்ராலிக் அழுத்தம் | ஹைட்ராலிக் அழுத்தம் | எம்.பி.ஏ. | 14 |
| மோட்டார் சக்தி | மோட்டார் சக்தி | கே.டபிள்யூ. | 37+37 KW |
| உலர்த்தும் சுழற்சி நேரம் | உலர் சுழற்சி | எஸ் | 4 |
| மொத்த சக்தி | மொத்த சக்தி | கே.டபிள்யூ. | 95 |
| இயக்க சக்தி | இயக்க சக்தி | % | 52-70 |
| பிற அளவுருக்கள் | |||
| அழுத்தப்பட்ட காற்று அழுத்தம் | குறைந்தபட்ச காற்று அழுத்தம் | எம்.பி.ஏ. | 0.7-1.2 |
| காற்று கொள்ளளவு | அழுத்தப்பட்ட காற்று கொள்ளளவு | M3/நிமிடம் | 0.7 |
| குளிரூட்டும் நீர் ஓட்டம் | நீர் ஓட்டம் | M3/h | 4 |
| குளிரூட்டும் நீர் அழுத்தம் | குளிரூட்டும் நீர் அழுத்தம் | எம்.பி.ஏ. | 0.3-0.4 |
| பரிமாணம் (நீளம் x அகலம் x உயரம்) | ஒட்டுமொத்த பரிமாணம் | எம் | 5.5x2x2.4 M |
| நிகர எடை | நிகர எடை | டன் | 18 Ton |
குறிப்பு: அனைத்து அளவுருக்களும் குறிப்புக்காக மட்டுமே. உபகரண மேம்பாடுகள் காரணமாக விவரக்குறிப்புகளை மாற்றியமைக்கும் உரிமை எவர் பவருக்கு உண்டு.
Max Cavity Count per Container Volume (EP135 - For Reference)
| தொகுதி | 10மிலி | 30மிலி | 60மிலி | 100மிலி | 250மிலி | 500மிலி | 1000மிலி |
|---|---|---|---|---|---|---|---|
| அதிகபட்ச குழிகள் | 30 | 26 | 22 | 18 | 14 | 10 | 8 |
Core Hardware Architecture of the EP135
முழு ஐரோப்பிய பாணி எஃகு சட்டகம்
CNC-machined monolithic machine bed and platen mounts ensure parallelism between injection and blow clamping platens. Tie-bar surfaces are induction-hardened. The EP135 clamping force is 20-30% above equivalent-tonnage competitors due to the boosted pressurized clamping structure.
பைமெட்டாலிக் திருகு மற்றும் பீப்பாய்
The plasticizing unit uses a bimetallic-lined barrel and a hardened alloy screw rated for glass-fiber and mineral-filled compounds. The EP135 screw diameter of 70 mm at 22:1 L/D delivers thorough homogenization with a 650 g shot capacity, covering the full range of bottle weights for this tonnage class.
விகிதாசார வால்வு ஹைட்ராலிக் கட்டுப்பாடு
உட்செலுத்தல் அழுத்தம் மற்றும் ஊதுதல் அழுத்தம் ஆகிய இரண்டும் செர்வோ-விகிதாசார ஹைட்ராலிக் வால்வுகள் மூலம் ஒழுங்குபடுத்தப்படுகின்றன. இது, மெல்லிய சுவர்களுடைய முன்வடிவங்களுக்குப் பல-நிலை உட்செலுத்தல் விவரக்குறிப்பை (நிரப்பு வேகம், நிலைமாற்றம், பொதி அழுத்தம்) சாத்தியமாக்குகிறது. மேலும், ஒற்றை-நிலை ஊதுதல் வால்வு அமைப்புகளில் பொதுவாகக் காணப்படும் ஆர வலைப்பின்னல் குறைபாடுகளை நீக்கும் துல்லியமான ஊதுதல் அழுத்த சரிவுக் கட்டுப்பாட்டையும் இது வழங்குகிறது.
பிஎல்சி தொடுதிரை கட்டுப்பாட்டு அமைப்பு
The EP135 control panel runs a full-color PLC touch-screen with parameter recipe storage. All process variables - temperatures, pressures, velocities, timings - are set and monitored from a single screen. Alarm history, production counters and fault codes are logged and displayed in real time.
மேம்படுத்தப்பட்ட ஹாட் ரன்னர் அமைப்பு
இன்ஜெக்ஷன் மோல்டின் ஹாட் ரன்னர் மேனிஃபோல்டானது, பூஜ்ஜிய டெட்-ஸோன் ஓட்டத்திற்காக வடிவமைக்கப்பட்டுள்ளது. இது அனைத்து குழிகளிலும் கிராம் எடை விலகல் குறைக்கப்படுவதை உறுதி செய்கிறது. பிளஸ் அல்லது மைனஸ் 1 டிகிரி வரையிலான வெப்பநிலை கட்டுப்பாட்டுத் துல்லியம், வெப்பத்தால் எளிதில் பாதிப்படையக்கூடிய பொருட்கள் சிதைவடைவதைத் தடுக்கிறது. மேலும், ஒளிபுகும் கொள்கலன்களில் சீரான தெளிவுக்கு இது இன்றியமையாததாகும்.
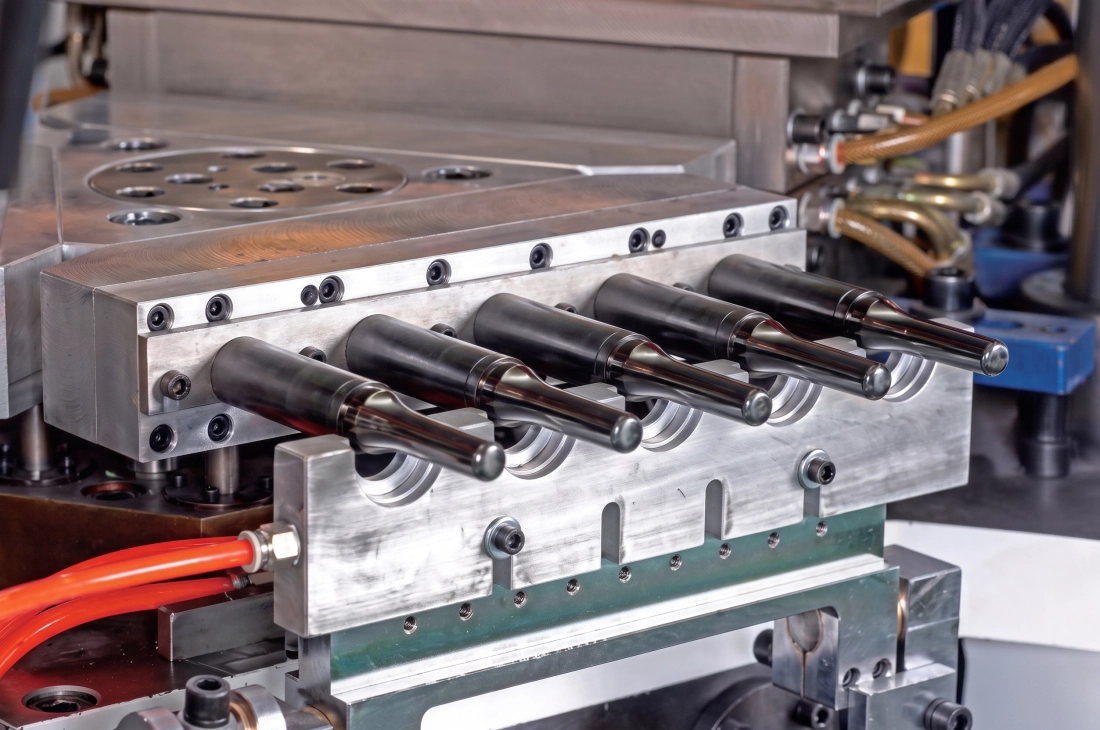
சிறப்பு மையத் தண்டு வடிவமைப்பு
The mandrels (core rods) feature internal cooling channels that reduce core temperature between the injection and blow stations, accelerating the cooling phase. Fast-cycle mandrels enable the EP135 to achieve a 4 S dry cycle without sacrificing preform cooling uniformity or dimensional stability.
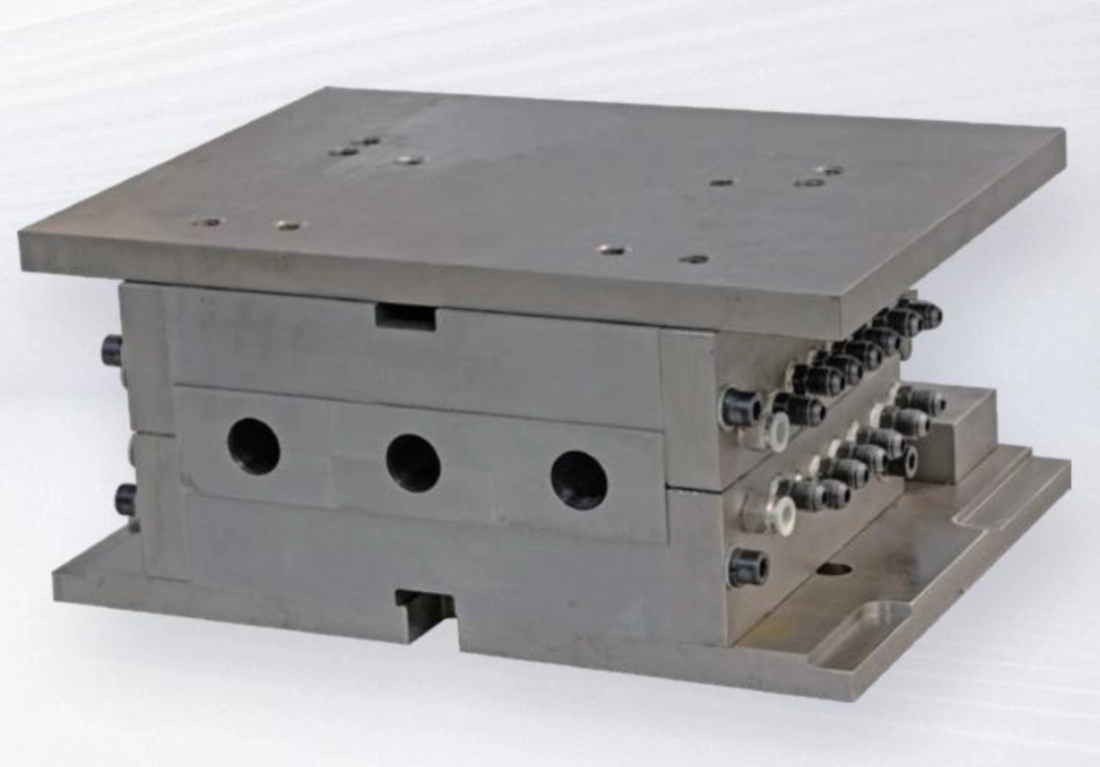
ஊசி ஊது வார்ப்பகம் மற்றும் பிதுக்கு ஊது வார்ப்பகம்: துல்லியமான கொள்கலன்களில் ஐபிஎம் ஏன் வெற்றி பெறுகிறது?
Buyers evaluating hollow container equipment often compare IBM and EBM on capital cost alone. The EP135 is more than a machine choice - it is a process choice that determines your long-term production economics and the quality ceiling your facility can achieve. The comparison below reflects real production differences that directly affect your cost per thousand bottles and your ability to win pharmaceutical and cosmetic supply contracts.
| இல்லை. | ஒப்பீட்டுப் பொருள் | ஊசி ஊதுதல் (IBM) | வெளியேற்ற ஊதுதல் (EBM) |
|---|---|---|---|
| 1 | பாட்டில் எடை நிலைத்தன்மை | எடை மாறுபாடு தோராயமாக 1% | எடை மாறுபாடு தோராயமாக 3% |
| 2 | சுவர் தடிமன் சீரான தன்மை | சுவர் தடிமன் முழுவதும் சீராக உள்ளது | சுவர் தடிமன் 10-20% வரை மாறுபடும் |
| 3 | பாட்டில் கழுத்து / நூல் | பிளாஷ் இல்லை, கழுத்தில் பிரிப்புக் கோடு இல்லை. | வெட்டுத் தடம், பலவீனமான அடித்தளம் மற்றும் கழுத்து |
| 4 | அடிப்படை குவிவு | வலுவான நேர்மறை குவிவு, நிலையான அடித்தளம் | பிஞ்ச் வெல்டிங் காரணமாக பலவீனமான குவிவு |
| 5 | பொருள் கழிவுகள் | கழிவுகள் அற்றது - பிசிறுகளோ கழிவுகளோ இல்லை | பிஞ்ச் ஃப்ளாஷிலிருந்து கிடைத்த 20-40% ஸ்கிராப் |
| 6 | மிகவும் மெல்லிய சுவர் திறன் | மிகவும் மெல்லிய சுவர்களுக்கு அவ்வளவு பொருத்தமானதல்ல. | கட்டுப்படுத்தி மூலம் சுவரின் தடிமனை சரிசெய்யலாம். |
| 7 | சுற்றுச்சூழல் உணர்திறன் | சுற்றுப்புற மாற்றங்களுக்கு உணர்திறன் அற்றது | அடிக்கடி சரிசெய்தல் தேவைப்படுகிறது |
| 8 | குழி எண்ணிக்கை மற்றும் வெளியீடு | அதிக குழிவுறுதல், அதிக மகசூல், தட்டையான வாய் | குறைவான துளைகள், குறைந்த வெளியீடு, சீரற்ற கழுத்து |
| 9 | அச்சு ஆயுட்காலம் மற்றும் செலவு | அச்சின் நீண்ட ஆயுள், தொடர்ச்சியான அதிக உற்பத்திக்கு ஏற்றது. | குறைந்த அச்சு ஆயுட்காலம், குறைந்த ஆரம்பச் செலவு |
| 10 | கால்தடம் | கச்சிதமான ஒருங்கிணைந்த அமைப்பு, குறைந்த இடவசதி | கூடுதல் துணை உபகரணங்கள், பெரிய தரைப்பரப்பு |
| 11 | ஓவல் கொள்கலன் உருவாக்கம் | நீள்வட்ட வடிவங்களை உருவாக்குவது மிகவும் சவாலானது | நீள்வட்ட வடிவங்களை உருவாக்குவது எளிது |
Application Fields and Container Types for the EP135
The EP135 is designed to produce bottles and containers from 1ml to the maximum volume for this model, covering the full range of primary packaging needs across four major market verticals. The table below shows the container types and industry segments where this தானியங்கி ஊசி ஊது அச்சு உபகரணங்கள் அதன் மிக உயர்ந்த வணிக வருவாயை வழங்குகிறது.
மருந்துத் தொழில்
- கண் சொட்டு மருந்து புட்டிகள் (LDPE, 5-30மிலி)
- வாய்வழி மாத்திரை மற்றும் காப்ஸ்யூல் புட்டிகள் (HDPE, 30-500மிலி)
- மூக்குத் தெளிப்பான் மற்றும் பம்ப் புட்டிகள் (PP)
- குழந்தைகள் திறக்க முடியாத மூடிகளுடன் கூடிய திரவ மருந்து பாட்டில்கள்
- தடுப்பூசி மற்றும் வினைப்பொருள் குப்பிகள் (LDPE, 1-20மிலி)
- GMP-தரமான அம்பர் மற்றும் வெள்ளை நிற HDPE மாத்திரை பாட்டில்கள்
அழகுசாதனப் பொருட்கள் தொழில்
- ரோல்-ஆன் டியோடரண்ட் அப்ளிகேட்டர் பாட்டில்கள் (PE, 50-100மிலி)
- மஸ்காரா குழாய்கள் மற்றும் குச்சி வடிவ பாட்டில்கள் (PP, 5-20மிலி)
- நகப்பூச்சு பாட்டில்கள் (PS, 10-30மிலி)
- லோஷன் மற்றும் சீரம் பம்ப் பாட்டில்கள் (PCTG, 30-200 மிலி)
- அகன்ற வாய் கொண்ட கிரீம் ஜாடிகள் (PP/PS)
- ஃபவுண்டேஷன் மற்றும் டோனர் பாட்டில்கள்
குழந்தை பொருட்கள் மற்றும் உணவு
- குழந்தை பால் புட்டிகள் (PP, PPSU, 150-300மிலி)
- குழந்தை ஃபார்முலா அள்ளும் பாட்டில்கள்
- தேன் மற்றும் பாகு கொள்கலன்கள் (LDPE)
- குறைந்த அளவு சிறப்பு பான கொள்கலன்கள்
- உண்ணக்கூடிய எண்ணெய் மாதிரி பாட்டில்கள்
- தயிர் மற்றும் பால் பொருட்கள் பேக்கேஜிங்
தினசரி இரசாயன மற்றும் தொழில்துறை
- ஷாம்பு மற்றும் கண்டிஷனர் பாட்டில்கள் (HDPE/PP)
- கை சுத்திகரிப்பான் மற்றும் லோஷன் வழங்கும் கருவிகள்
- வாகன திரவ மாதிரி பாட்டில்கள்
- விவசாய இரசாயன செறிவூட்டல் பாட்டில்கள்
- துப்புரவுப் பொருள் கொள்கலன்கள்
- துல்லியமான கழுத்துகளைக் கொண்ட தொழில்துறை வினைப்பொருள் பாட்டில்கள்
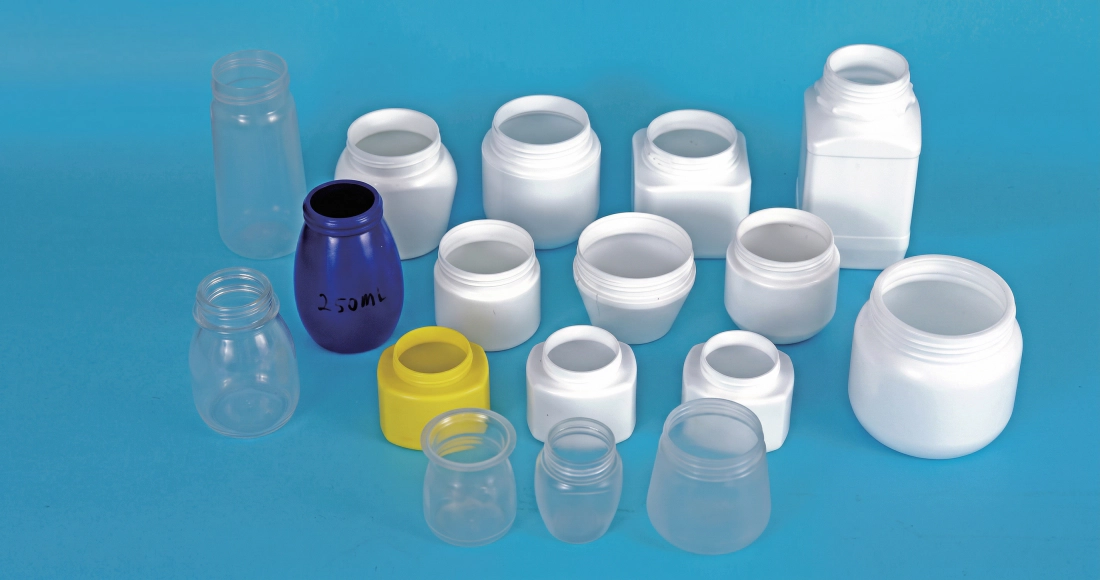
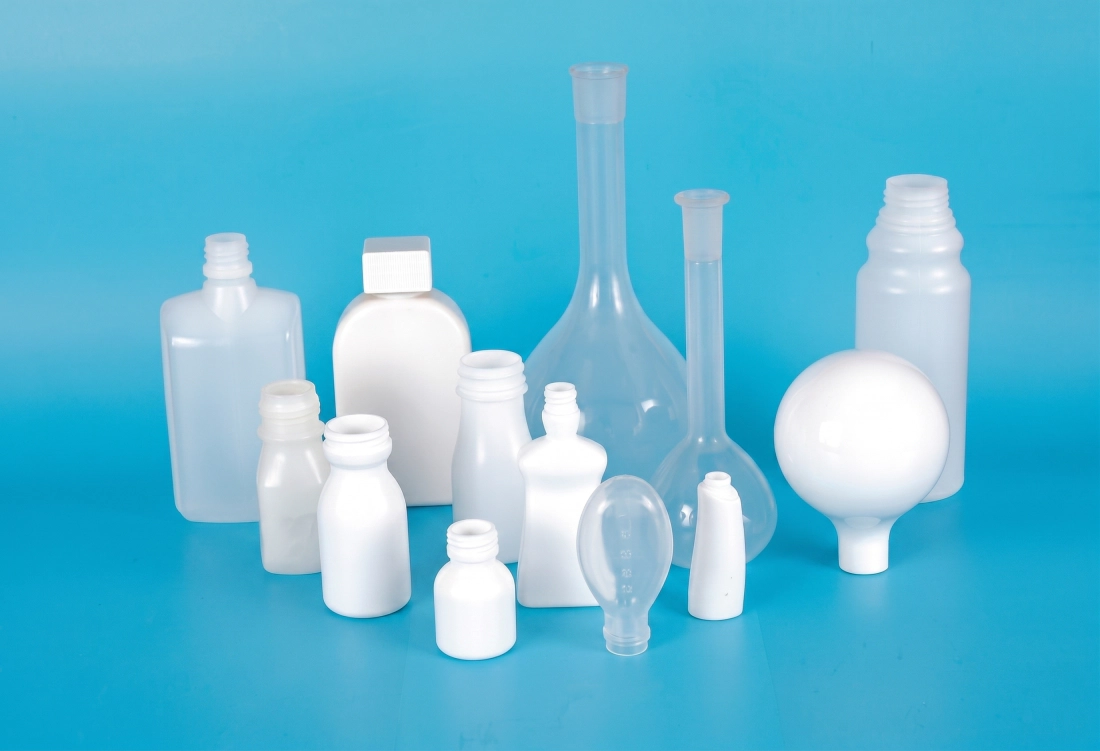

Processing Engineering Plastics on the EP135: PC, PETG and Tritan Capability
While the majority of IBM applications use polyethylene (HDPE/LDPE), polypropylene and standard PS, premium packaging sectors - particularly high-end cosmetics and reusable baby products - increasingly specify engineering-grade materials: polycarbonate (PC), PETG copolyester, or Tritan copolyester. These materials demand processing conditions that standard IBM machines cannot reliably deliver. The EP135 is engineered to handle them.
The screw and barrel of the EP135 feature a 22:1 L/D ratio with a barrier-geometry screw profile optimized for high-viscosity, shear-sensitive melts. PC, which must be processed at barrel temperatures of 270-310 degrees Celsius with a melt viscosity 5 to 10 times higher than PP, requires both higher plasticizing torque and a gentle, controlled shear profile to avoid molecular weight degradation that causes yellowing and brittle fracture. The bimetallic barrel construction withstands the abrasive compounds often blended into these engineering resins and extends service life substantially beyond standard nitride-hardened barrels.
Hot runner temperature control on the EP135 operates with zone accuracy to plus or minus 1 degree Celsius - a specification that matters critically when processing transparent materials. Even a 5-degree temperature deviation in a hot runner nozzle will cause visible black specks from localized thermal degradation, or air entrapment bubbles from outgassing. The optimized hot runner manifold design on the EP135 mold eliminates dead zones where melt can stagnate between shots, which is the primary source of color contamination and black spot defects when processing PC or PETG at production speeds.
Investment Return and Production Efficiency Analysis: Why Choose the EP135?
The acquisition cost of the EP135 must be evaluated against five measurable efficiency drivers that determine cost per thousand bottles and payback period. Purchasing engineers who evaluate only machine price - without these five factors - systematically undervalue the IBM platform and overestimate EBM economics for their target application.
1. ஜீரோ ஃபிளாஷ் ஸ்கிராப்
IBM நிறுவனம் பிளாஷ் கழிவுகளையோ அல்லது பிஞ்ச்-லைன் கழிவுகளையோ உருவாக்குவதில்லை. EBM ஒவ்வொரு சுழற்சிக்கும் 20-401 டன் பாட்டில் எடையை கழிவாக உருவாக்குகிறது. ஆண்டுக்கு 200 டன் PP உற்பத்தி செய்யும் நிலையில், கழிவுகள் இல்லாத IBM நிறுவனம் ஆண்டுதோறும் 40-80 டன் ரெசினைச் சேமிக்கிறது. ஒரு டன்னுக்கு 1,500 அமெரிக்க டாலர் என்ற கணக்கில், ஒரே ஒரு இயந்திரத்தின் மூலம் மட்டும் ஆண்டுக்கு 60,000-120,000 அமெரிக்க டாலர் மதிப்புள்ள மூலப்பொருட்கள் சேமிக்கப்படுகின்றன.
2. ஒளிர்வு நீக்கும் தொழிலாளர் இல்லை
EBM requires a secondary deflashing operation - either inline mechanical or manual - adding labor cost, a second machine footprint, and an additional quality failure point. IBM bottles from the EP135 come off the conveyor with zero post-processing required before filling or labeling, saving 1-3 operators per shift.
3. குறுகிய உலர்த்தும் சுழற்சி செயல்திறன்
The EP135 achieves a 4 S dry cycle. With 22 cavities at 60ml, annual output at 6,000 hours run time exceeds 118.0 million bottles. This throughput concentration into a single compact machine reduces total asset investment per unit of capacity versus multi-machine EBM lines at equivalent output.
4. விரைவான அச்சு மாற்றம்
The injection mold and blow mold on the EP135 can be changed in 2-4 hours by a trained two-person team. Recipe recall from the PLC removes setup time entirely for repeat jobs. Facilities running 8-15 SKUs on a single EP135 achieve mold changeover frequency of 2-4 per week with total changeover downtime below 10% of available production hours.
இடத் தேவை மற்றும் பயன்பாட்டுத் திறன்
The EP135 footprint of 5.5x2x2.4 M consolidates injection, blow and ejection into a single machine envelope. Compare this to a two-machine EBM line (extruder plus blow machine, plus deflash press, plus conveyor) which typically occupies 3-4 times the floor area for equivalent throughput. Utility connections - compressed air at 0.7-1.2 MPa, cooling water at 4 M3/h flow, electrical connection at 95 KW total - are all single-point utilities, reducing installation complexity and ongoing maintenance overhead.
Factory building cost in pharmaceutical-grade cleanroom environments can reach 2,000-5,000 USD per square meter. The compact footprint of the EP135 directly reduces the cleanroom area required to produce a given volume of output - a capital benefit that does not appear in machine comparison tables but materially affects total project economics.
EP தொடர் IBM அச்சுப் பண்புகள் மற்றும் வடிவமைப்புத் தரநிலைகள்
- ■செயல்திறன் மிக்க குழி மற்றும் கழுத்துத் தடுப்பு வடிவமைப்பு ஊசி அச்சு குழிகள் மற்றும் கழுத்துப் பகுதிகள் தனித்தனியாக சரிசெய்யக்கூடியவை, இது முழு அச்சுத் தொகுப்பையும் மாற்றாமல் முன்வடிவக் குழாய் உடலின் பரிமாணங்களை நுணுக்கமாக சரிசெய்ய அனுமதிக்கிறது. எண்ணெய் மற்றும் நீர் செல்லும் பாதைகள், நிலையான வெப்பநிலை விநியோகம் மற்றும் எளிதாகப் பிரித்தெடுப்பதற்காகவே பிரத்யேகமாக வடிவமைக்கப்பட்டுள்ளன.
- ■பிரீமியம் எஃகு தரங்கள் ஊசி அச்சு அமைப்புகள் 4Cr13 துருப்பிடிக்காத எஃகு அல்லது இறக்குமதி செய்யப்பட்ட உயர் வலிமை கொண்ட S136 கலப்பு எஃகைப் பயன்படுத்துகின்றன. S136 என்பது 52 HRC வரையிலான முழு கடினத்தன்மை கொண்ட, கண்ணாடி போன்ற பளபளப்பும் அரிப்பை எதிர்க்கும் திறனும் வாய்ந்த ஒரு எஃகு ஆகும். சிறந்த வெப்பக் கடத்துத்திறன் மற்றும் சுழலும் சுழல் கலத்தில் குறைக்கப்பட்ட நிலைம நிறைக்காக, ஊது அச்சு அமைப்புகளை மெக்னீசியம்-அலுமினியக் கலவையில் தயாரிக்கலாம்.
- ■உகந்த வெப்ப ரன்னர் மற்றும் முன்வடிவ வடிவமைப்பு ஹாட் ரன்னர் மேனிஃபோல்டானது, அனைத்துக் குழிகளிலும் கிராம் எடை விலகலைக் குறைக்கவும், ப்ரீஃபார்ம் அமைப்பின் சுவர் தடிமன் மாறுபாட்டைக் குறைக்கவும் வடிவமைக்கப்பட்டுள்ளது. மேண்ட்ரல் வடிவமைப்பானது, சீரான காற்று விநியோகத்தை உறுதிசெய்து, நிலையான ஊதுதல் விரிவாக்கத்தையும் விரைவான குளிரூட்டலையும் வழங்குகிறது.
- ■துல்லியமான கழுத்து நூல் மற்றும் சீல் பரிமாணங்கள் பாட்டிலின் வாய் உள் மற்றும் வெளி விட்டங்கள், திருகு இடைவெளி மற்றும் விளிம்பு வடிவியல் ஆகியவை வரைபடத் துல்லியத்திற்கு ஏற்ப இயந்திரத்தால் செதுக்கப்படுகின்றன. உற்பத்தி செய்யப்படும் மாதிரிகள் அனைத்திலும் மூடியின் காற்றுப்புகாத் தன்மை விகிதம் 100% ஆகும்.
- ■கழுத்து மற்றும் அடிப்பகுதியில் ஒளிப்பிழம்பு இல்லை. - the IBM process geometry eliminates parting-line flash at the bottle mouth and pinch-weld flash at the base. Bottles exit the EP135 with no trimming required at either end.
- ■தயாரிப்பு நிலைத்தன்மை அளவீடுகள் அளவு, எடை, பிரிப்புக் கோட்டின் நிலை மற்றும் சுவரின் தடிமன் ஆகியவை அனைத்துக் குழிகளிலும் மற்றும் உற்பத்தித் தொகுதிகளிலும் சீராக இருப்பதால், மருந்துத் துறை வாடிக்கையாளர்கள் 100% ஆய்வுக்கான கூடுதல் செலவின்றி, ஒவ்வொரு தொகுதிக்குமான புள்ளிவிவர அடிப்படையில் உற்பத்தியைச் சரிபார்க்க முடிகிறது.
Equipment Selection Guide: Is the EP135 Right for Your Production Requirements?
Selecting the correct IBM tonnage requires calculating the intersection of three variables: preform weight, required cavity count, and target output per hour. Use this framework to confirm whether the EP135 is correctly sized for your application, or to understand what production parameters it can support.
படி 1: முன்வடிவத்தின் எடையைக் கணக்கிடுங்கள்
Take the target bottle weight in grams (including the neck, body and base). Add 2-5% for process cushion. The EP135 injection weight of 650 g must be equal to or greater than (target preform weight x number of cavities). For example: a 5g preform at 8 cavities requires 40g shot weight, well within the 650 g capacity.
படி 2: தேவையான பல் சொத்தை எண்ணிக்கையைக் கணக்கிடுங்கள்
Target output (bottles/hour) divided by (3600 seconds / cycle time in seconds) gives required cavities. At a 4 S cycle and 10,000 bottles per hour target: 10,000 / (3600 / 4) = 12 cavities minimum. Cross-check against the cavity table above to confirm the EP135 can deliver this at your bottle volume.
படி 3: அச்சுத் தட்டின் பொருத்தத்தைச் சரிபார்க்கவும்
The injection mould layout (cavity array footprint) must fit within the EP135 max platen size of 1300x500 mm. Wide-bottle (diameter greater than 120mm) or tall-bottle (height greater than 220mm) applications exceed the EP135 mould envelope and require a larger model. Confirm your bottle OD and height before specifying cavity count.
படி 4: மூலப்பொருள் மற்றும் உட்செலுத்தும் அழுத்தம்
PP requires higher injection pressure and melt temperature than LDPE. PC and PETG require even higher barrel temperatures and longer residence-time plasticization. The EP135 hydraulic system pressure of 14 MPa and motor of 37+37 KW supports the injection forces needed for PP and engineering grade materials at the rated injection weight. Confirm your resin specification with the EVER POWER application team before ordering.
EVER POWER application engineers provide free pre-sales technical consultation to validate your container dimensions, material, cavity count and production target against EP135 specifications. Contact us with your bottle drawing and production brief for a written confirmation of suitability.
இயந்திரக் கட்டமைப்பு மேலோட்டம் மற்றும் பராமரிப்பு வழிகாட்டுதல்கள்
The EP135 is built around three core functional modules. Understanding their maintenance requirements is essential for sustaining the machine performance metrics - dry cycle, output rate, and product quality - over the full production life of the equipment.
பாகம் 1 - உட்செலுத்தும் அலகு: திருகு, குழல், வெப்ப இயக்கி
உட்செலுத்தும் அலகு, பிளாஸ்டிக்கை உருக்கி, முன்வடிவக் குழிக்குள் அளந்து செலுத்துகிறது. தினசரிப் பராமரிப்பு: குழல் வெப்பநிலை விவரங்களை நிர்ணயிக்கப்பட்ட அளவுகளுடன் ஒப்பிட்டுச் சரிபார்க்கவும், திருகு முனை மற்றும் சோதனை வளையத்தில் தேய்மானக் குறிகாட்டிகள் உள்ளதா எனப் பரிசோதிக்கவும், மேலும் தொடங்குவதற்கு முன், சூடான ஓட்டப் பகுதி வெப்பநிலைகள் நிர்ணயிக்கப்பட்ட அளவுகளிலிருந்து 2 டிகிரிக்குள் இருப்பதை உறுதி செய்யவும். வாராந்திரம்: குழல் காப்புப் பட்டைகளைப் பரிசோதிக்கவும், உட்செலுத்தும் உருளையின் முத்திரைகளில் எண்ணெய் கசிவு உள்ளதா எனச் சரிபார்க்கவும், மேலும் முந்தைய உற்பத்தியிலிருந்து ஏற்பட்ட ஏதேனும் வண்ணக் கலப்படம் இருந்தால் அதை அகற்றவும். மாதாந்திரம்: சோதனை வளையம் மற்றும் திருகு முனை அமைப்பைக் கழற்றிச் சுத்தம் செய்யவும்; திருகு இறக்கைகளில் தேய்மானம் உள்ளதா எனப் பரிசோதிக்கவும் மற்றும் இடைவெளிக்காகக் குழல் துளையின் விட்டத்தை அளவிடவும். உருகல் வழிப்பாதை மற்றும் குண்டு எடை சீரற்ற தன்மையைத் தடுக்க, இடைவெளி உற்பத்தியாளரின் சகிப்புத்தன்மையை மீறினால் குழலை மாற்றவும்.
சுத்திகரிப்பு முறை: அடர் நிறங்களிலிருந்து வெளிர் நிறங்களுக்கு மாறும்போதோ அல்லது பொறியியல் ரெசினிலிருந்து வணிக ரெசினுக்கு மாறும்போதோ, புதிய பொருளின் செட் பாயிண்ட்டை விட 10 டிகிரி அதிகமுள்ள பேரல் வெப்பநிலையில் ஒரு வணிக சுத்திகரிப்பு கலவையைப் பயன்படுத்தவும். புதிய பொருளுக்கு மாறுவதற்கு முன் 5-10 சுத்திகரிப்பு ஷாட்களை இயக்கவும். சுத்திகரிப்பு செய்யாமல், செயலாக்க வெப்பநிலையில் 20 நிமிடங்களுக்கு மேல் பேரலை ஒருபோதும் சும்மா வைத்திருக்க வேண்டாம் - சும்மா இருக்கும் நேரங்களில் ஏற்படும் வெப்பச் சிதைவே, மீண்டும் தொடங்கும் போது கருப்புப் புள்ளி மாசுபடுதலுக்கு முதன்மைக் காரணமாகும்.
தொகுதி 2 - இறுக்கும் மற்றும் சுழலும் குறியீட்டு அலகு
கிளாம்பிங் சிஸ்டம் மற்றும் ரோட்டரி இன்டெக்சர் ஆகியவை மிக உயர்ந்த இயந்திரவியல் சுமைகளைத் தாங்குவதோடு, மிகவும் துல்லியமான நிலைப்படுத்தல் தேவைகளையும் கொண்டுள்ளன. தினசரி: உயவு அட்டவணைப்படி டை-பார் பரப்புகளிலும் ரோட்டரி டேபிள் கைடு ரெயில்களிலும் கிரீஸைப் பூசவும் (எவர் பவர் கிரீஸின் தரத்தைக் குறிப்பிடுகிறது - இயக்க வெப்பநிலையில் பாகுத்தன்மையை தக்கவைக்காத பொதுப் பயன்பாட்டு கிரீஸை மாற்றாகப் பயன்படுத்த வேண்டாம்). ராட் சீலில் எண்ணெய் கசிவு உள்ளதா என ஹைட்ராலிக் கிளாம்பிங் சிலிண்டரை ஆய்வு செய்யவும். இன்டெக்சிங் சுழற்சியின் போது அசாதாரணமான ஒலிகள் கேட்கிறதா எனக் கவனிக்கவும் - ஏதேனும் உலோகக் கிளிக் அல்லது தயக்கம் ஏற்பட்டால், ஆங்குலர் டிவைடர் பேரிங்கில் ஆய்வு தேவை என்பதைக் குறிக்கிறது.
மாதாந்திரம்: நான்கு டை-பார் நிலைகளில் டயல் இண்டிகேட்டரைப் பயன்படுத்தி பிளேட்டனின் இணைகோட்டுத்தன்மையைச் சரிபார்க்கவும்; 0.05 மிமீ-க்கு மேல் விலகல் இருந்தால், மீண்டும் ஷிம்மிங் செய்ய வேண்டும். டரெட்டில் உள்ள ஒரு குறிப்புப் பரப்பின் மீது டயல் இண்டிகேட்டரை வைத்து, தொடர்ந்து 100 இன்டெக்சிங் சுழற்சிகளுக்குப் பிறகு அதே நிலை 0.02 மிமீ-க்குள் மீண்டும் வருகிறதா என்பதைச் சரிபார்ப்பதன் மூலம் இன்டெக்சிங் நிலையின் துல்லியத்தைச் சோதிக்கவும். விலகல் காணப்பட்டால், மெக்கானிக்கல் ஸ்டாப்பைச் சரிசெய்யவும் அல்லது எவர் பவர் சேவையைத் தொடர்பு கொள்ளவும்.
தொகுதி 3 - நீரியல் அமைப்பு மற்றும் குளிரூட்டும் சுற்று
The hydraulic system is the energy backbone of the EP135. System pressure is set at 14 MPa. Daily: check hydraulic oil level in the tank sight glass, check oil temperature display (normal operating range 40-55 degrees Celsius; above 60 degrees indicates a cooling circuit problem or filter blockage), and inspect all visible hydraulic hose fittings for weeping. The oil filter indicator must be checked every 250 hours - a red indicator requires immediate filter element replacement, not deferral.
Cooling circuit: the EP135 requires clean, scale-free cooling water at 0.3-0.4 MPa pressure and 4 M3/h flow. Install a water treatment system upstream of the machine to prevent calcium scale buildup inside mold cooling channels. Scale buildup of just 1mm in a 6mm channel reduces cooling efficiency by over 30%, extending cycle times and reducing output. Flush cooling circuits with a descaling solution annually. Chiller water quality must be neutral pH (6.5-7.5) and contain an anti-corrosion inhibitor compatible with copper and aluminum alloy mold materials.
எவர் பவர் வழங்கும் முழுமையான தீர்வுகள் மற்றும் தனிப்பயனாக்குதல் சேவைகள்
EVER POWER supplies the EP135 as either a standalone machine or as the centerpiece of a complete turnkey bottle production line. For customers setting up a new facility or expanding into a new container product line, the turnkey approach eliminates the integration risk that comes from sourcing the IBM machine, molds, auxiliaries, and downstream equipment from separate vendors.
அச்சு வடிவமைப்பு மற்றும் உற்பத்தி
எவர் பவர் பொறியாளர்கள், வாடிக்கையாளரின் பாட்டில் வரைபடங்கள் அல்லது 3D கோப்புகளிலிருந்து இன்ஜெக்ஷன் மற்றும் ப்ளோ மோல்ட் செட்களை உருவாக்குகின்றனர். S136 அல்லது 4Cr13 எஃகில் செய்யப்பட்ட பல-குழி ஹாட் ரன்னர் மோல்டுகள். அதிக-குழி உற்பத்தி கருவிகளைப் பயன்படுத்துவதற்கு முன்பு, கொள்கலன் சரிபார்ப்புக்காக முன்மாதிரி ஒற்றை-குழி மோல்டுகள் உருவாக்கப்படுகின்றன. ஏற்றுமதிக்கு முன்பு, தொழிற்சாலையில் T0 மோல்ட் சோதனைகள் நடத்தப்படுகின்றன.
துணை உபகரண ஒருங்கிணைப்பு
The EVER POWER turnkey line includes: screw air compressor, air tank and air dryer, mold temperature controller, industrial chiller, auto loader, conveyor belt, screen printing and labeling system, washing and drying line, and automatic filling and capping machines. All auxiliary equipment is specified and pre-integrated to match the EP135 output rate.
கீழ்நிலை தர அமைப்புகள்
Optional inline bottle visual inspection machine (machine vision system for flash, deformation and contamination detection), automatic leak tester, automatic packing machine, and carton erector. For pharmaceutical lines, 100% inline leak testing and vision inspection are available as integrated modules matched to the EP135 conveyor output speed.
ஜிஎம்பி மற்றும் க்ளீன்ரூம் கட்டமைப்பு
GMP-தர உற்பத்தி தேவைப்படும் மருந்துத் துறை வாடிக்கையாளர்களுக்காக, எவர் பவர் நிறுவனம் பின்வரும் இயந்திரத் தனிப்பயனாக்கங்களை வழங்குகிறது: உற்பத்திப் பகுதி மாசுபடுவதைத் தடுப்பதற்கான மூடிய-அமைப்பு உயவு, துருப்பிடிக்காத எஃகு பாதுகாப்பு உறைகள், வகுப்பு 100,000 தூய்மை அறை இணக்கத்தன்மைக்கான HEPA-வடிகட்டப்பட்ட இயந்திர உறை, மற்றும் உபகரணத் தகுதிப்படுத்தல் (IQ/OQ/PQ) நெறிமுறைகளுக்கான ஆவண ஆதரவு.
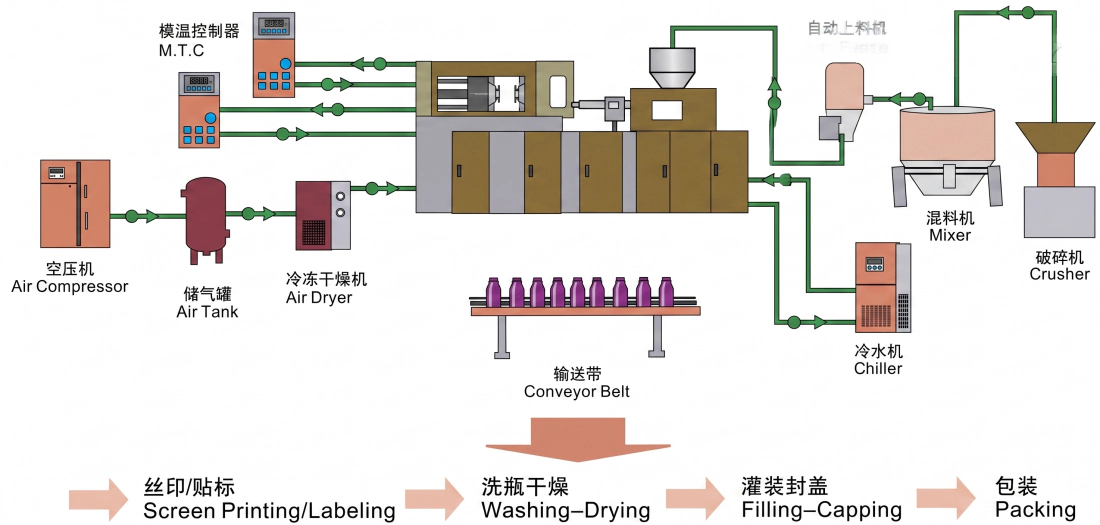
Auxiliary Equipment Available with the EP135

தரக் கட்டுப்பாடு மற்றும் உற்பத்தித் தரநிலைகள்
முக்கியமான பாகங்களின் CNC இயந்திர வேலைப்பாடு
வடிவியல் துல்லியத்திற்கு உத்தரவாதம் அளிப்பதற்காக, இயந்திரப் படுக்கை, இறுக்கும் தட்டுகள் மற்றும் அனைத்து துல்லியமான மேற்பரப்புகளும் ஒரே அமைப்பில் CNC இயந்திரம் மூலம் செதுக்கப்படுகின்றன. தட்டின் இணைகோட்டுத்தன்மை 0.02 மிமீ துல்லியத்திற்கு லேசர் அளவீடு மூலம் சரிபார்க்கப்படுகிறது. தாங்கியில் குறுக்கீடு இல்லாத பொருத்தத்திற்காக, இணைப்புப் பட்டைத் துளைகள் H7 சகிப்புத்தன்மைக்கு மெருகூட்டப்படுகின்றன.
டை-பார் தூண்டல் கடினப்படுத்துதல்
இணைப்புக் கம்பிகள், 52-58 HRC மேற்பரப்புக் கடினத்தன்மைக்கு உயர் அதிர்வெண் தூண்டல் கடினப்படுத்தலுக்கு உட்படுத்தப்பட்டு, அதனைத் தொடர்ந்து துல்லியமாக அரைக்கப்படுகின்றன. இந்த மேற்பரப்புச் செயலாக்கம், மில்லியன் கணக்கான சுழற்சிகளுக்கு மேல் இறுக்கும் தகடுகளின் தொடர்ச்சியான நழுவும் உராய்வினால் ஏற்படும் தேய்மானத்தைத் தாங்கும் திறனை, உராய்வு அல்லது தேய்மானம் ஏற்படாமல் வழங்குகிறது.
ஹைட்ராலிக் சுற்று தூய்மை
அனைத்து ஹைட்ராலிக் சுற்றுகளும் பொருத்துவதற்கு முன்பு சுத்தப்படுத்தப்பட்டு, அழுத்தப் பரிசோதனை செய்யப்பட்டு, துகள் எண்ணிக்கை சரிபார்க்கப்படுகின்றன. ஹைட்ராலிக் எண்ணெயின் தூய்மை குறைந்தபட்சம் ISO 4406 வகுப்பு 17/15/12 அளவில் பராமரிக்கப்படுகிறது. வால்வு ஸ்பூல் ஒட்டிக்கொள்வதைத் தடுக்கவும், நகர்வைக் கட்டுப்படுத்தவும், விகிதாசார மற்றும் செர்வோ வால்வுகளின் மாசுபடும் உணர்திறனுக்கு இந்த அளவிலான தூய்மை அவசியமாகிறது.
72 மணி நேர தொழிற்சாலை இயக்கி சோதனை
Every EP135 undergoes a minimum 72-hour continuous loaded run test at the factory before shipment. During this period, production output samples are measured for weight consistency, wall thickness uniformity, and dimensional accuracy. Any parameter outside specification triggers a hold and corrective action before the machine is cleared for delivery.
CE பாதுகாப்பு வழிகாட்டுதல்
The EP135 is CE-marked in compliance with EU Machinery Directive requirements. Safety features include: interlocked safety doors with hydraulic circuit interrupt, light curtain protection at the operator access zone, emergency stop at all operator positions, and two-hand operator control for manual mold setting. CE documentation is provided with every machine.
விற்பனைக்குப் பிந்தைய சேவை மற்றும் தொழில்நுட்ப ஆதரவு
நிறுவுதல் மற்றும் செயல்பாட்டுக்குக் கொண்டுவருதல்
எவர் பவர் நிறுவனத்தின் மூத்த பொறியாளர்கள், இயந்திரத்தை நிறுவுதல், செயல்பாட்டிற்குக் கொண்டுவருதல் மற்றும் ஏற்புச் சோதனைகளுக்குப் பொறுப்பானவர்கள். இயந்திரம் நிலையான உற்பத்தி நிலையை அடையும் வரை பொறியாளர் பணியிடத்திலேயே இருப்பார். மேலும், அனைத்து இயக்குபவர்களுக்கும் இயந்திரச் செயல்பாடு, அச்சு மாற்றம் மற்றும் வழக்கமான பராமரிப்பு ஆகியவற்றில் பயிற்சி அளிக்கப்படும். ஏற்பு அளவுகோல்கள், ஏற்றுமதிக்கு முன்பே ஒப்புக்கொள்ளப்பட்டு, செயல்பாட்டிற்குக் கொண்டுவரும் அறிக்கையில் ஆவணப்படுத்தப்படுகின்றன.
தடுப்பு பராமரிப்பு திட்டம்
எவர் பவர், பயன்பாட்டில் உள்ள அனைத்து இயந்திரங்களுக்கும் திட்டமிடப்பட்ட பராமரிப்பு நினைவூட்டல் சேவையை வழங்குகிறது. இந்தப் பராமரிப்பு நாட்காட்டி, தினசரி, வாராந்திர, மாதாந்திர மற்றும் வருடாந்திரப் பணிகளை உள்ளடக்கியுள்ளது. முன்கூட்டியே செய்யப்படும் பராமரிப்பு, திட்டமிடப்படாத பழுதுகளைத் தடுப்பதோடு, அதிக செலவுள்ள அவசர உதிரிபாக விநியோகத் தேவையையும் குறைக்கிறது. தடுப்புப் பராமரிப்பு அட்டவணையைப் பின்பற்றும் வாடிக்கையாளர்கள், இயந்திரத்தின் பயன்பாட்டு நேரம் 95%-க்கு மேல் இருப்பதாகத் தொடர்ந்து தெரிவிக்கின்றனர்.
24x7 சேவை ஹாட்லைன்
எவர் பவர் சேவை உதவி எண், வாரத்தில் 7 நாட்களும், 24 மணி நேரமும் செயல்படும். அவசர உற்பத்திப் பழுதுகளுக்கு, சேவை எண்ணிற்கு அழைக்கவும் அல்லது குறுஞ்செய்தி அனுப்பவும். தகுதிவாய்ந்த பொறியாளர் ஒருவர் 2 மணி நேரத்திற்குள் பதிலளித்து, தொலைவிலிருந்து சிக்கலைக் கண்டறிவார். உங்கள் இடத்திற்கே வந்து சேவை தேவைப்பட்டால், எவர் பவர் உங்கள் இருப்பிடத்திற்கு ஏற்ற குறைந்தபட்ச பதிலளிப்பு நேரத்துடன் ஒரு தொழில்நுட்ப வல்லுநரை அனுப்பும்.
உதிரி பாகங்களின் இருப்பு
EVER POWER maintains a comprehensive spare parts inventory for all EP135 components including hydraulic seals, proportional valve cartridges, heating bands, temperature sensors, drive belts and electrical components. Parts can be shipped globally within 48 hours for items in stock. Critical fast-wear items are available for customer-held local inventory based on EVER POWER recommendations.
தொழில்நுட்பப் பயிற்சித் திட்டங்கள்
வழக்கமான நிறுவல் பயிற்சிக்கு அப்பால், எவர் பவர் நிறுவனம் இயந்திர இயக்கம், அச்சு செயல்முறை மேம்படுத்தல், அச்சு மாற்றம் மற்றும் அமைத்தல், ஹைட்ராலிக் அமைப்பு பராமரிப்பு, மற்றும் PP, LDPE, PCTG போன்ற குறிப்பிட்ட பொருட்களுக்கான செயல்முறைப் பழுதுநீக்கம் போன்ற பிரத்யேகப் பயிற்சித் தொகுதிகளை வழங்குகிறது. இந்தப் பயிற்சியை எவர் பவர் தொழிற்சாலையிலோ அல்லது வாடிக்கையாளரின் இடத்திலோ நடத்தலாம்.
Frequently Asked Questions - EVER POWER EP135
What materials can the EP135 process?
The EP135 is compatible with HDPE, LDPE, PP, PS (including lactic acid bacteria grade transparent PS), ABS, EVA, bio-based corn material, PCTG, and similar thermoplastics. For engineering resins such as PC, PETG and Tritan, the screw L/D of 22:1 and the 6+N heating zones provide the residence time and temperature profile needed for thorough, degradation-free plasticization. Confirm your resin grade with EVER POWER application engineering before ordering.
Can the EP135 be used for pharmaceutical GMP production?
Yes. The EP135 can be configured for pharmaceutical GMP production environments. Key features supporting GMP include: the one-step process eliminates inter-machine bottle transfer that introduces contamination risk in two-stage systems; the closed lubrication system prevents lubricant contamination of the product zone; and the machine can be specified with a stainless steel safety enclosure suitable for cleanroom installation. EVER POWER can provide equipment documentation to support IQ/OQ/PQ qualification processes for pharmaceutical facility validation.
How long does mould changeover take on the EP135?
A trained two-person team can complete a full mold changeover (injection mold, blow mold, and mandrel set) on the EP135 in approximately 2-4 hours, depending on the mold design and the changeover frequency experience of the team. PLC recipe recall eliminates parameter re-entry time for repeat mold sets. Facilities that invest in quick-release clamping plates for the mold base can reduce changeover to under 2 hours.
What certifications does the EP135 carry?
The EP135 is CE-marked for the European market. The machine design complies with EU Machinery Directive safety requirements including interlocked guards, emergency stop systems, and electrical safety standards. EVER POWER is an ISO-certified manufacturer. Machine documentation is provided in English and can be supplied in other languages upon request for export markets.
What is the lead time for the EP135 and an associated mould set?
Standard machine lead time for the EP135 is 45-75 days from order confirmation and deposit receipt, depending on production schedule at time of order. Mold sets are typically supplied in 60-90 days from final confirmation of bottle drawings and material specification. The machine and mold sets can be scheduled to arrive simultaneously for a coordinated installation. Contact EVER POWER for current lead time at time of inquiry.
Ready to Specify the EVER POWER EP135 for Your Production Line?
உங்கள் பாட்டில் வரைபடம், இலக்கு கொள்ளளவு, மூலப்பொருள் விவரக்குறிப்பு மற்றும் ஒரு மணி நேரத்திற்குத் தேவைப்படும் வெளியீடு ஆகியவற்றை எங்கள் பயன்பாட்டுப் பொறியியல் குழுவிற்கு அனுப்பவும். நாங்கள் சரியான குழி எண்ணிக்கை மற்றும் இயந்திர உள்ளமைப்பை எழுத்துப்பூர்வமாக உறுதிசெய்து, 3 வேலை நாட்களுக்குள் ஒரு விரிவான வணிக முன்மொழிவை வழங்குவோம்.
கூடுதல் தகவல்
| திருத்தப்பட்டது | ஹைவ் மூலம் |
|---|
தொடர்புடைய தயாரிப்புகள்
-
EP60HE அதிவேக முழு மின்சார ஊசி ஊது அச்சு இயந்திரம், ஹைட்ராலிக் இல்லாத 2.5 வினாடி சுழற்சி
-
அதிக கொள்ளளவு கொண்ட பாட்டில்களுக்கான தொழில்துறை ஊசி ஊது அச்சு இயந்திரம் EP110 1100KN தானியங்கி IBM உபகரணம்
-
அதிக உற்பத்தித் திறன் கொண்ட ஊசி ஊது அச்சு இயந்திரம் EP80 800KN பிளாஷ் இல்லாத பாட்டில் அச்சு உபகரணம்
-
தானியங்கி ஒரு-படி ஊசி ஊது அச்சு இயந்திரம் EP60 600KN மருந்து அழகுசாதனப் புட்டி உற்பத்தியாளர்
-
மருந்து மற்றும் அழகுசாதனப் பாட்டில்களுக்கான தானியங்கி ஒற்றை-படி ஊசி ஊது அச்சு இயந்திரம் EP40 400KN CE ISO


