
بڑے حجم کی بوتلوں کے لیے صنعتی انجکشن بلو مولڈنگ مشین EP110 1100KN خودکار IBM آلات
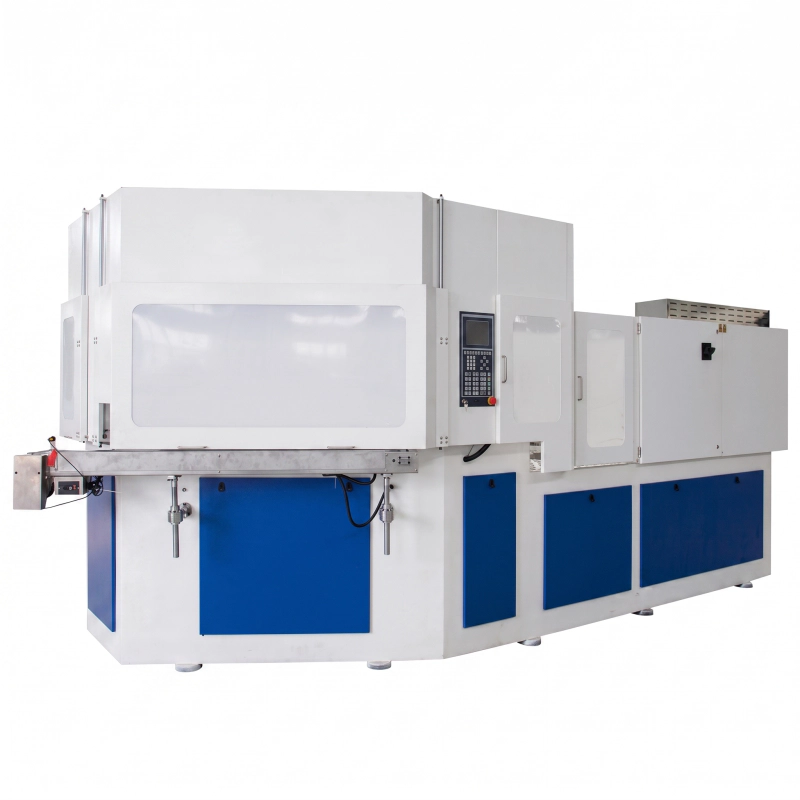
EVER POWER EP110 injection blow molding machine delivers 1100KN clamping force, 540g injection weight and up to 24 cavities for 10ml bottles. Standard dual hydraulic system, high-precision angle divider, 4s dry cycle. Suitable for 1-2000ml pharmaceutical, cosmetic and daily chemical containers. 15 Ton, CE ISO, 80KW total power.
What Is the EVER POWER EP110 One-Step Injection Blow Molding Machine?
The EVER POWER EP110 is a fully automatic one-step IBM (Injection Blow Molding) machine engineered for precision hollow container production. As a dedicated انجیکشن بلو مولڈنگ مشین بنانے والا, EVER POWER نے کئی دہائیوں کی ٹولنگ اور عمل کی مہارت کو اس ماڈل میں مرتکز کیا ہے، ایک ایسی مشین کی فراہمی جہاں پوری بوتل - پریفارم انجیکشن سے لے کر فائنل بلونگ تک - آپریٹر کی مداخلت کے بغیر، مشینوں کے درمیان مواد کی منتقلی کے بغیر، اور فلیش اور پارٹنگ لائن ویسٹ کے بغیر مکمل ہوتی ہے جو اخراج بلو سسٹم کی خصوصیت رکھتے ہیں۔
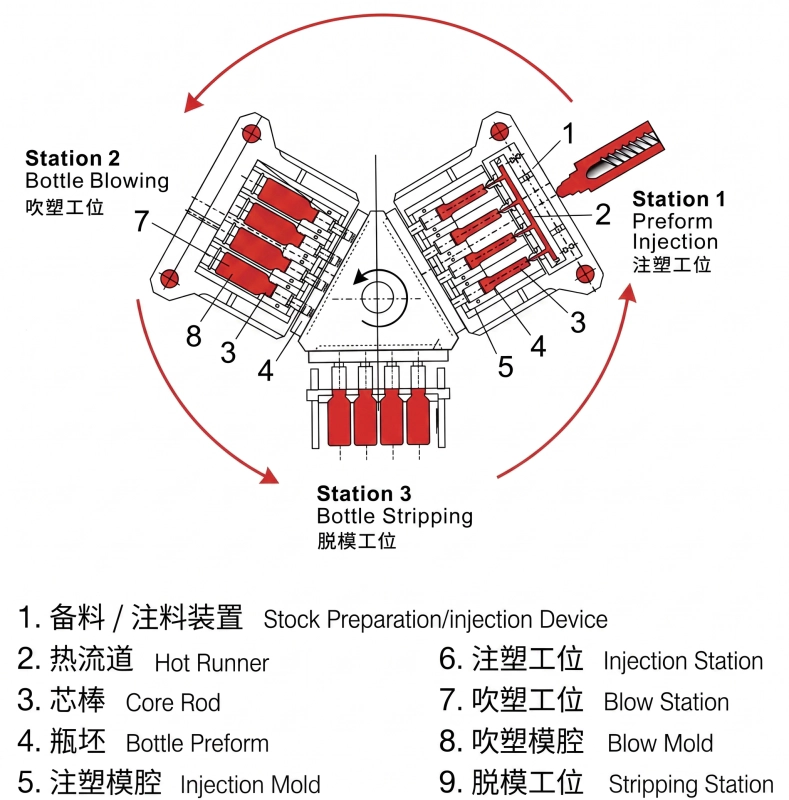
یہ ایک قدم IBM مشین is the preferred choice for pharmaceutical bottle blowing and cosmetic container manufacturing where dimensional consistency is non-negotiable. Each cycle on the EP110 runs three simultaneous operations: while new preforms are being injection-molded at Station 1, the previous batch is being blown to final shape at Station 2, and the completed bottles from Station 2 are being stripped and conveyed to the outfeed conveyor at Station 3. This triaxial parallelism means the productive output equals the injection cycle time alone - not the sum of injection plus blowing plus ejection - giving the EP110 a significant throughput advantage over two-stage stretch blow systems for small and medium volume containers.
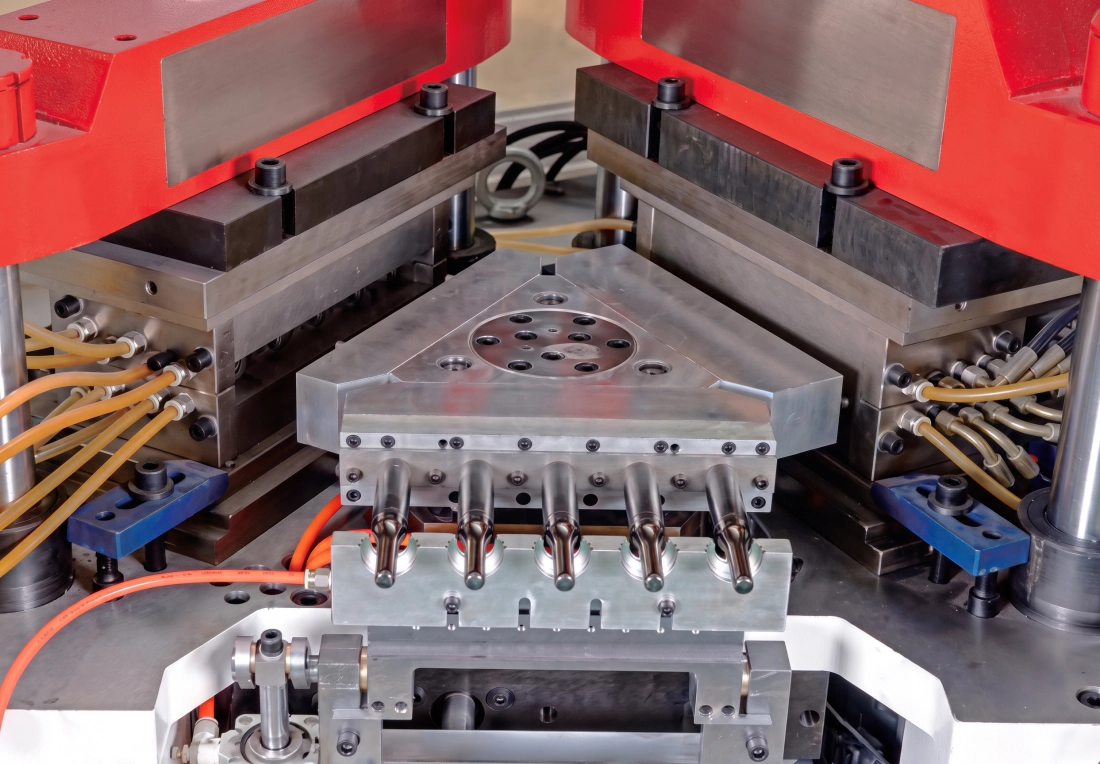
Three-Station Process: How the EP110 Works
اسٹیشن 1 - پریفارم انجیکشن
پلاسٹک کے دانے بیرل میں پگھلائے جاتے ہیں اور کنٹرول شدہ دباؤ کے تحت انجیکشن کیویٹی میں انجکشن لگائے جاتے ہیں۔ بوتل کی گردن اور دھاگے کی جیومیٹری ٹھیک ٹھیک انجیکشن مولڈ میں بنتی ہے۔ انجیکشن مولڈ کھلتا ہے اور گرم پریفارم کو لے جانے والا مینڈریل روٹری برج کے ذریعے اسٹیشن 2 میں منتقل ہوتا ہے۔
اسٹیشن 2 - بلو مولڈنگ
گرم پریفارم مینڈرل کور سے کمپریسڈ ہوا کے ذریعہ فلایا جاتا ہے۔ بوتل کی شکل مکمل طور پر بلو مولڈ گہا سے طے ہوتی ہے۔ ہوا ٹھنڈے مولڈ کی دیواروں کے خلاف پرفارم کو باہر کی طرف بڑھاتی ہے، اور بوتل اپنی آخری جہت کو سنبھال لیتی ہے۔ مولڈ کھلتا ہے اور برج اسٹیشن 3 کی طرف بڑھتا ہے۔
اسٹیشن 3 - نکالنا اور پہنچانا
تیار شدہ، ٹھنڈی بوتلوں کو مینڈریل سے چھین لیا جاتا ہے اور آؤٹ فیڈ کنویئر پر چھوڑ دیا جاتا ہے۔ چونکہ تینوں اسٹیشن ایک ساتھ کام کرتے ہیں، اس لیے یہ سائیکل مسلسل دہرایا جاتا ہے۔ کوئی ثانوی آپریشن نہیں ہے، کوئی ڈیفلیشنگ پریس نہیں ہے، اور بوتل کو دوبارہ گرم کرنے کی ضرورت نہیں ہے - تینوں آپریشن ایک سائیکل کلاک کا اشتراک کرتے ہیں۔
Main Technical Parameters - EVER POWER EP110
| پیرامیٹر | آئٹم (EN) | یونٹ | ای پی 110 |
|---|---|---|---|
| انجیکشن سسٹم | |||
| سکرو قطر | سکرو قطر | ملی میٹر | 65 mm |
| سکرو L/D تناسب | سکرو L/D | - | 22:1 |
| انجکشن کا وزن | انجکشن کا وزن | جی | 540 g |
| حرارتی طاقت | حرارتی طاقت | کلو واٹ | 20 KW |
| بیرل ہیٹنگ زونز | بیرل زونز کی تعداد | - | 5+N |
| انجیکشن اسٹروک | انجیکشن اسٹروک | ملی میٹر | 200 mm |
| کلیمپنگ سسٹم | |||
| انجیکشن کلیمپ فورس | انجیکشن کی کلیمپنگ فورس | کے این | 1100 |
| انجیکشن اوپننگ اسٹروک | انجیکشن کے لئے افتتاحی اسٹروک | ملی میٹر | 140 ملی میٹر |
| بلو کلیمپ فورس | اڑانے کی کلیمپنگ فورس | کے این | 150 |
| بلو اوپننگ اسٹروک | اڑانے کے لیے افتتاحی اسٹروک | ملی میٹر | 140 ملی میٹر |
| ٹاور لفٹ کی اونچائی | روٹری ٹیبل کی اونچائی اٹھانا | ملی میٹر | 70 ملی میٹر |
| سانچہ | |||
| زیادہ سے زیادہ پلیٹن سائز (LxW) | زیادہ سے زیادہ پلیٹن سائز (L x W) | ملی میٹر | 1100x460 mm |
| مولڈ موٹائی | مولڈ موٹائی | ملی میٹر | 280 mm |
| زیادہ سے زیادہ بوتل قطر | دیا بوتل کی | ملی میٹر | 120 ملی میٹر |
| زیادہ سے زیادہ بوتل کی اونچائی | بوتل کی اونچائی | ملی میٹر | 220 ملی میٹر |
| بوتل کے حجم کی حد | مناسب بوتل والیوم | ملی لیٹر | 1-2000 |
| سٹرپنگ اسٹروک | سٹرپنگ اسٹروک | ملی میٹر | 260 mm |
| ہائیڈرولک نظام | |||
| ہائیڈرولک پریشر | ہائیڈرولک پریشر | ایم پی اے | 14 |
| موٹر پاور | موٹر پاور | کلو واٹ | 22+22 KW |
| خشک سائیکل کا وقت | خشک سائیکل | ایس | 4 |
| کل پاور | کل پاور | کلو واٹ | 80 |
| آپریٹنگ پاور | آپریٹنگ پاور | % | 52-70 |
| دوسرے پیرامیٹرز | |||
| کمپریسڈ ہوا کا دباؤ | کم سے کم ہوا کا دباؤ | ایم پی اے | 0.7-1.2 |
| ہوا کی صلاحیت | کمپریسڈ ہوا کی صلاحیت | M3/منٹ | 0.7 |
| ٹھنڈا پانی کا بہاؤ | پانی کا بہاؤ | M3/h | 4 |
| کولنگ واٹر پریشر | کولنگ واٹر پریشر | ایم پی اے | 0.3-0.4 |
| طول و عرض (L x W x H) | مجموعی طول و عرض | ایم | 5x1.8x2.2 M |
| خالص وزن | خالص وزن | ٹن | 15 Ton |
نوٹ: تمام پیرامیٹرز صرف حوالہ کے لیے ہیں۔ EVER POWER آلات میں بہتری کی وجہ سے وضاحتیں تبدیل کرنے کا حق محفوظ رکھتا ہے۔
Max Cavity Count per Container Volume (EP110 - For Reference)
| حجم | 10 ملی لیٹر | 30 ملی لیٹر | 60 ملی لیٹر | 100 ملی لیٹر | 250 ملی لیٹر | 500 ملی لیٹر | 1000 ملی لیٹر |
|---|---|---|---|---|---|---|---|
| زیادہ سے زیادہ cavities | 24 | 22 | 18 | 14 | 10 | 8 | 6 |
Core Hardware Architecture of the EP110
مکمل یورپی طرز کا اسٹیل فریم
CNC-machined monolithic machine bed and platen mounts ensure parallelism between injection and blow clamping platens. Tie-bar surfaces are induction-hardened. The EP110 clamping force is 20-30% above equivalent-tonnage competitors due to the boosted pressurized clamping structure.
Bimetallic سکرو اور بیرل
The plasticizing unit uses a bimetallic-lined barrel and a hardened alloy screw rated for glass-fiber and mineral-filled compounds. The EP110 screw diameter of 65 mm at 22:1 L/D delivers thorough homogenization with a 540 g shot capacity, covering the full range of bottle weights for this tonnage class.
متناسب والو ہائیڈرولک کنٹرول
انجیکشن پریشر اور بلو پریشر دونوں کو سرو پروپرشنل ہائیڈرولک والوز کے ذریعے ریگولیٹ کیا جاتا ہے۔ یہ پتلی دیواروں والے پرفارمز کے لیے ملٹی اسٹیج انجیکشن پروفائلنگ (فل رفتار، سوئچ اوور، پیک پریشر) اور عین مطابق بلو پریشر ریمپ کنٹرول کی اجازت دیتا ہے جو سنگل اسٹیج بلو والو سسٹمز میں عام ریڈیل ویبنگ نقائص کو ختم کرتا ہے۔
PLC ٹچ اسکرین کنٹرول سسٹم
The EP110 control panel runs a full-color PLC touch-screen with parameter recipe storage. All process variables - temperatures, pressures, velocities, timings - are set and monitored from a single screen. Alarm history, production counters and fault codes are logged and displayed in real time.
آپٹمائزڈ ہاٹ رنر سسٹم
انجیکشن مولڈ ہاٹ رنر مینی فولڈ کو صفر ڈیڈ زون کے بہاؤ کے لیے ڈیزائن کیا گیا ہے، اس بات کو یقینی بناتا ہے کہ تمام گہاوں میں گرام وزن کے انحراف کو کم سے کم کیا جائے۔ درجہ حرارت کو کنٹرول کرنے کی درستگی جمع یا مائنس 1 ڈگری تک گرمی سے متعلق حساس مواد کے انحطاط کو روکتی ہے اور شفاف کنٹینرز میں مسلسل وضاحت کے لیے ضروری ہے۔
خصوصی کور راڈ ڈیزائن
The mandrels (core rods) feature internal cooling channels that reduce core temperature between the injection and blow stations, accelerating the cooling phase. Fast-cycle mandrels enable the EP110 to achieve a 4 S dry cycle without sacrificing preform cooling uniformity or dimensional stability.
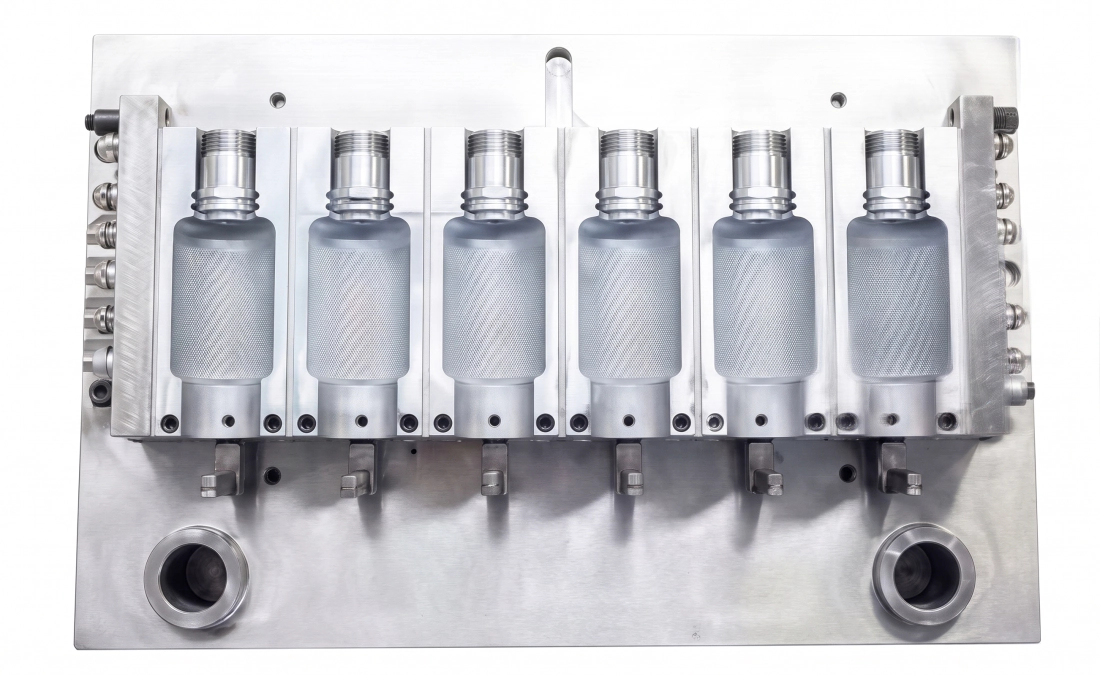
انجکشن بلو مولڈنگ بمقابلہ ایکسٹروژن بلو مولڈنگ: IBM صحت سے متعلق کنٹینرز کے لئے کیوں جیتتا ہے
Buyers evaluating hollow container equipment often compare IBM and EBM on capital cost alone. The EP110 is more than a machine choice - it is a process choice that determines your long-term production economics and the quality ceiling your facility can achieve. The comparison below reflects real production differences that directly affect your cost per thousand bottles and your ability to win pharmaceutical and cosmetic supply contracts.
| نہیں | موازنہ آئٹم | انجیکشن اڑانا (IBM) | اخراج اڑانا (EBM) |
|---|---|---|---|
| 1 | بوتل کے وزن میں مستقل مزاجی | وزن میں فرق تقریباً 1% | وزن میں فرق تقریباً 3% |
| 2 | دیوار کی موٹائی کی یکسانیت | پوری دیوار کی یکساں موٹائی | دیوار کی موٹائی 10-20% مختلف ہوتی ہے۔ |
| 3 | بوتل کی گردن / دھاگہ | کوئی فلیش نہیں، گردن پر کوئی جدا ہونے والی لکیر نہیں۔ | کٹ آف نشان، کمزور بنیاد اور گردن |
| 4 | بیس convexity | مضبوط مثبت محدب، مستحکم بنیاد | چوٹکی والی ویلڈ کی وجہ سے کمزور محدب |
| 5 | مادی فضلہ | صفر فضلہ - کوئی فلیش یا سکریپ نہیں | پنچ فلیش سے 20-40% سکریپ |
| 6 | انتہائی پتلی دیوار کی صلاحیت | بہت پتلی دیواروں کے لیے کم موزوں | کنٹرولر کے ذریعے دیوار کی موٹائی سایڈست |
| 7 | ماحولیاتی حساسیت | محیطی تبدیلیوں کے لیے حساس نہیں۔ | بار بار ایڈجسٹمنٹ کی ضرورت ہے۔ |
| 8 | کیوٹی کاؤنٹ اور آؤٹ پٹ | اعلی cavitation، اعلی پیداوار، فلیٹ منہ | کم گہا، کم پیداوار، ناہموار گردن |
| 9 | مولڈ لائف اور لاگت | طویل سڑنا زندگی، سوٹ مسلسل اعلی حجم رنز | مختصر سڑنا زندگی، کم ابتدائی لاگت |
| 10 | قدموں کا نشان | کومپیکٹ انٹیگریٹڈ سسٹم، چھوٹے زیر اثر | مزید معاون سامان، فرش کا بڑا علاقہ |
| 11 | اوول کنٹینر کی تشکیل | بیضوی شکلیں بنانا زیادہ مشکل ہے۔ | اوول پروفائلز بنانا آسان ہے۔ |
Application Fields and Container Types for the EP110
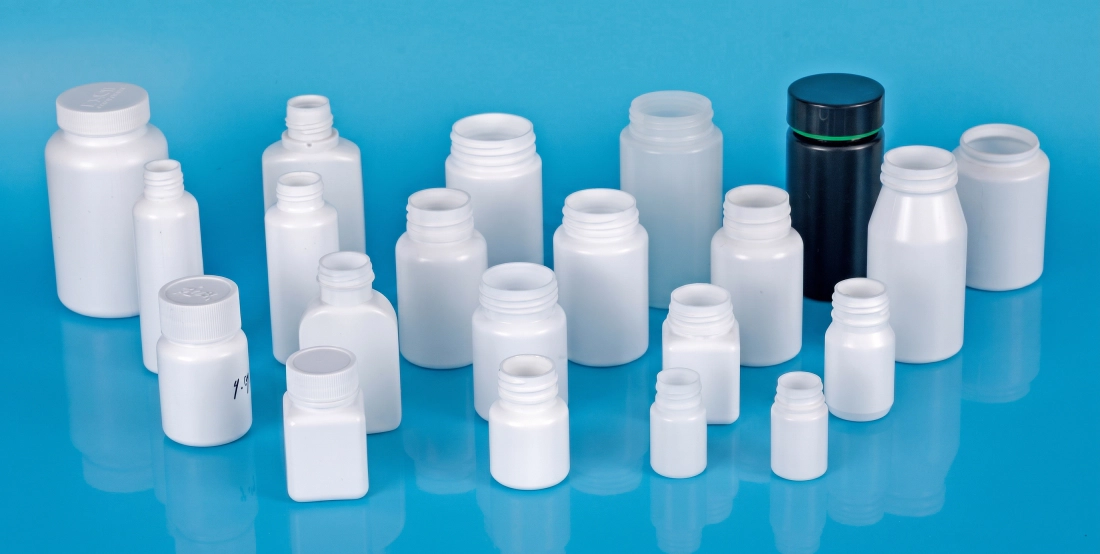
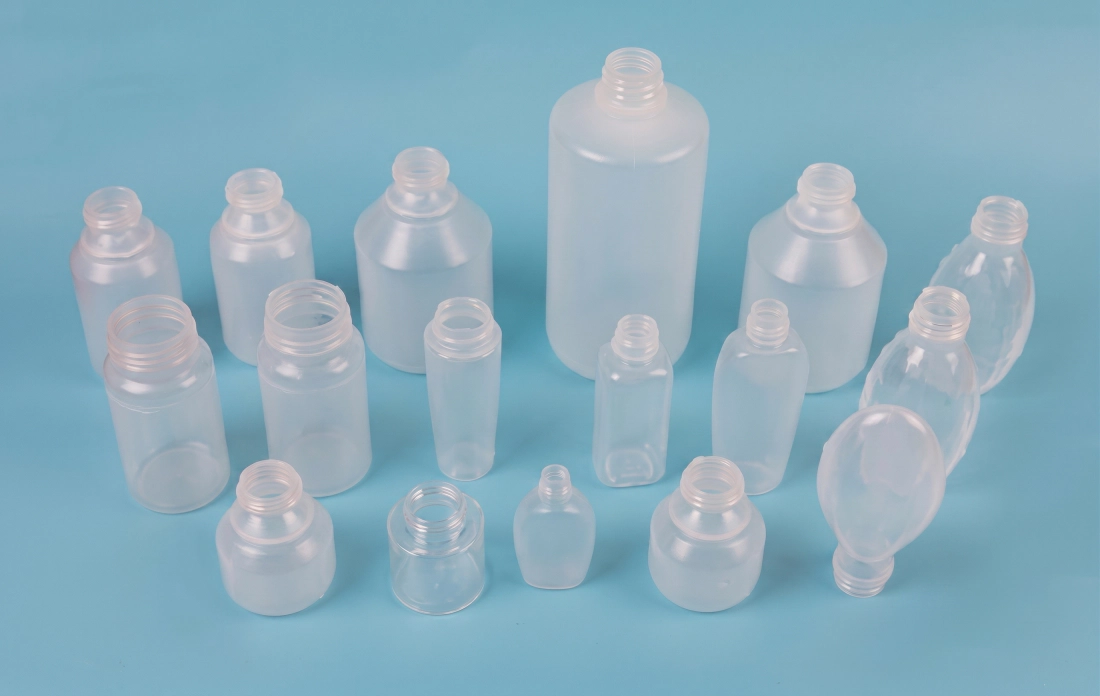
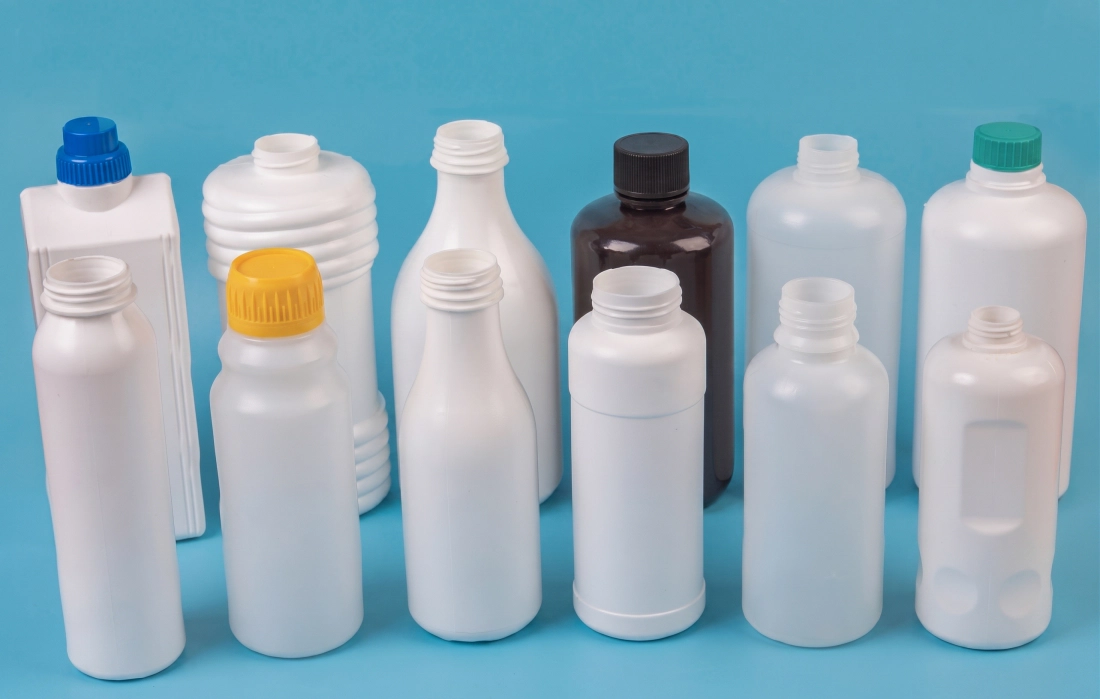
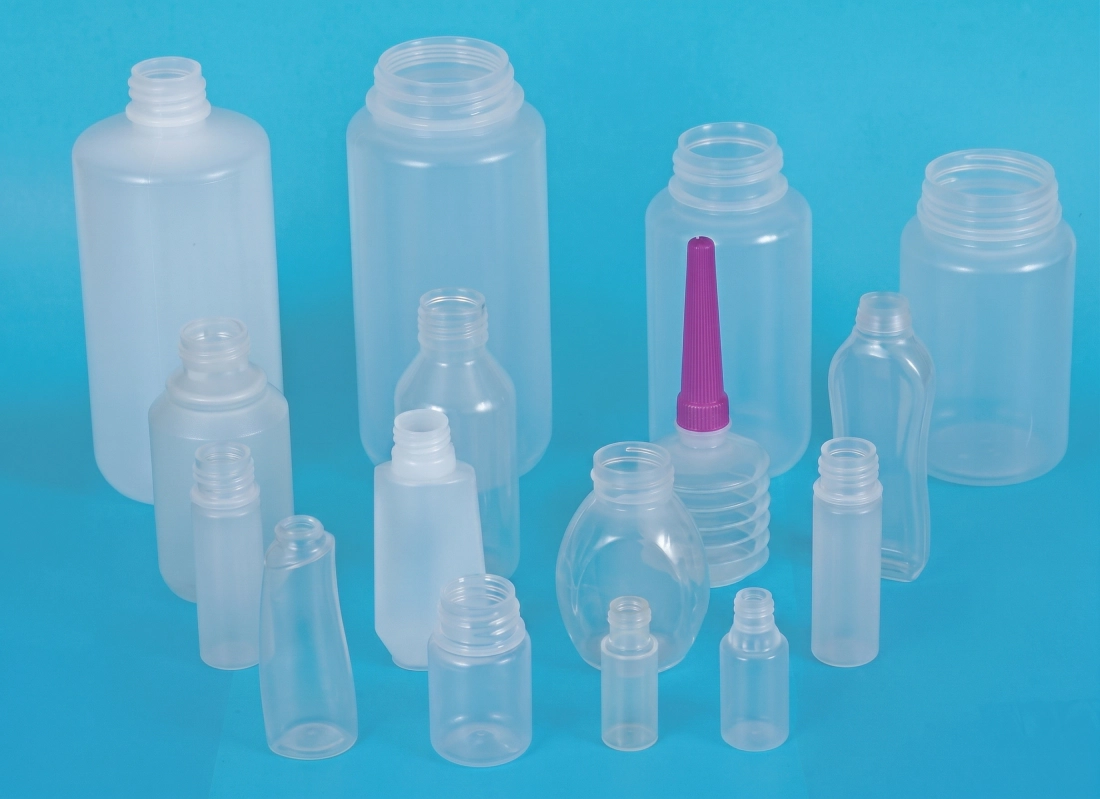
The EP110 is designed to produce bottles and containers from 1ml to the maximum volume for this model, covering the full range of primary packaging needs across four major market verticals. The table below shows the container types and industry segments where this خودکار انجیکشن بلو مولڈنگ کا سامان اپنی سب سے زیادہ تجارتی واپسی فراہم کرتا ہے۔
فارماسیوٹیکل انڈسٹری
- آئی ڈراپ بوتلیں (LDPE، 5-30ml)
- زبانی گولی اور کیپسول کی بوتلیں (HDPE، 30-500ml)
- ناک سپرے اور پمپ کی بوتلیں (PP)
- بچوں کے لیے مزاحم ٹوپیاں کے ساتھ مائع ادویات کی بوتلیں۔
- ویکسین اور ری ایجنٹ کی شیشیوں (LDPE، 1-20ml)
- جی ایم پی گریڈ امبر اور سفید ایچ ڈی پی ای گولی کی بوتلیں۔
کاسمیٹکس انڈسٹری
- رول آن ڈیوڈورنٹ ایپلی کیٹر بوتلیں (PE، 50-100ml)
- کاجل کی ٹیوبیں اور چھڑی کی بوتلیں (PP, 5-20ml)
- نیل پالش کی بوتلیں (PS، 10-30ml)
- لوشن اور سیرم پمپ کی بوتلیں (PCTG، 30-200ml)
- چوڑے منہ والی کریم جار (PP/PS)
- فاؤنڈیشن اور ٹونر کی بوتلیں۔
بچوں کی مصنوعات اور خوراک
- بچوں کو دودھ پلانے والی بوتلیں (PP، PPSU، 150-300ml)
- شیر خوار فارمولا سکوپنگ بوتلیں۔
- شہد اور شربت کے برتن (LDPE)
- چھوٹے حجم کے خصوصی مشروبات کے کنٹینرز
- خوردنی تیل کے نمونے کی بوتلیں۔
- دہی اور دودھ کی پیکیجنگ
روزانہ کیمیکل اور صنعتی
- شیمپو اور کنڈیشنر کی بوتلیں (HDPE/PP)
- ہینڈ سینیٹائزر اور لوشن ڈسپنسر
- آٹوموٹو سیال نمونے کی بوتلیں۔
- زرعی کیمیائی مرتکز بوتلیں۔
- مصنوعات کے کنٹینرز کی صفائی
- عین مطابق گردنوں کے ساتھ صنعتی ری ایجنٹ کی بوتلیں۔
Industrial Connectivity and Remote Diagnostics for the EP110
The EP110 is equipped with a PLC-based control platform that supports recipe management for multiple mold configurations. Each mold set - defined by its preform weight, blow pressure profile, cooling time and stripping sequence - can be saved as a named production recipe and recalled in under 60 seconds during a mold changeover. For OEM and contract manufacturers running 10 or more SKUs on a single machine, this eliminates the operator setup errors that traditionally cause the first 200-500 bottles of a new run to fall outside specification.
The control system logs cycle time, injection pressure peak, clamp force, motor amperage and hydraulic oil temperature for every production cycle. This real-time data stream can be connected to a factory SCADA system via standard industrial protocols. For overseas customers, EVER POWER engineers can connect to the machine remotely to review alarm logs, adjust process parameters, and guide local operators through fault recovery without requiring an on-site service visit - substantially reducing downtime cost for facilities far from a service center.
Energy monitoring is built into the EP110 dashboard: cumulative kWh consumption per production batch, energy cost per thousand bottles (configured with local electricity price), and OEE (Overall Equipment Efficiency) tracking across shifts. This data enables production managers to identify energy anomalies - such as a worn hydraulic seal increasing pump load - before they escalate into unplanned downtime. The transition from reactive maintenance to condition-based maintenance is one of the most significant cost reduction levers available to high-volume bottle manufacturers, and the EP110 makes it accessible without third-party hardware investment.
Investment Return and Production Efficiency Analysis: Why Choose the EP110?
The acquisition cost of the EP110 must be evaluated against five measurable efficiency drivers that determine cost per thousand bottles and payback period. Purchasing engineers who evaluate only machine price - without these five factors - systematically undervalue the IBM platform and overestimate EBM economics for their target application.
1. زیرو فلیش سکریپ
IBM کوئی فلیش اور کوئی پنچ لائن سکریپ تیار نہیں کرتا ہے۔ EBM بوتل کے وزن کا 20-40% فی سائیکل سکریپ کے طور پر پیدا کرتا ہے۔ ہر سال 200 ٹن PP پر، صفر سکریپ IBM سالانہ 40-80 ٹن رال بچاتا ہے۔ 1,500 USD فی ٹن پر، یعنی صرف ایک مشین سے خام مال کی بچت میں 60,000-120,000 USD ہے۔
2. کوئی ڈیفلیشنگ لیبر نہیں۔
EBM requires a secondary deflashing operation - either inline mechanical or manual - adding labor cost, a second machine footprint, and an additional quality failure point. IBM bottles from the EP110 come off the conveyor with zero post-processing required before filling or labeling, saving 1-3 operators per shift.
3. مختصر ڈرائی سائیکل تھرو پٹ
The EP110 achieves a 4 S dry cycle. With 18 cavities at 60ml, annual output at 6,000 hours run time exceeds 97.0 million bottles. This throughput concentration into a single compact machine reduces total asset investment per unit of capacity versus multi-machine EBM lines at equivalent output.
4. فوری مولڈ چینج اوور
The injection mold and blow mold on the EP110 can be changed in 2-4 hours by a trained two-person team. Recipe recall from the PLC removes setup time entirely for repeat jobs. Facilities running 8-15 SKUs on a single EP110 achieve mold changeover frequency of 2-4 per week with total changeover downtime below 10% of available production hours.
فوٹ پرنٹ اور افادیت کی کارکردگی
The EP110 footprint of 5x1.8x2.2 M consolidates injection, blow and ejection into a single machine envelope. Compare this to a two-machine EBM line (extruder plus blow machine, plus deflash press, plus conveyor) which typically occupies 3-4 times the floor area for equivalent throughput. Utility connections - compressed air at 0.7-1.2 MPa, cooling water at 4 M3/h flow, electrical connection at 80 KW total - are all single-point utilities, reducing installation complexity and ongoing maintenance overhead.
Factory building cost in pharmaceutical-grade cleanroom environments can reach 2,000-5,000 USD per square meter. The compact footprint of the EP110 directly reduces the cleanroom area required to produce a given volume of output - a capital benefit that does not appear in machine comparison tables but materially affects total project economics.
EP سیریز IBM مولڈ کی خصوصیات اور ڈیزائن کے معیارات
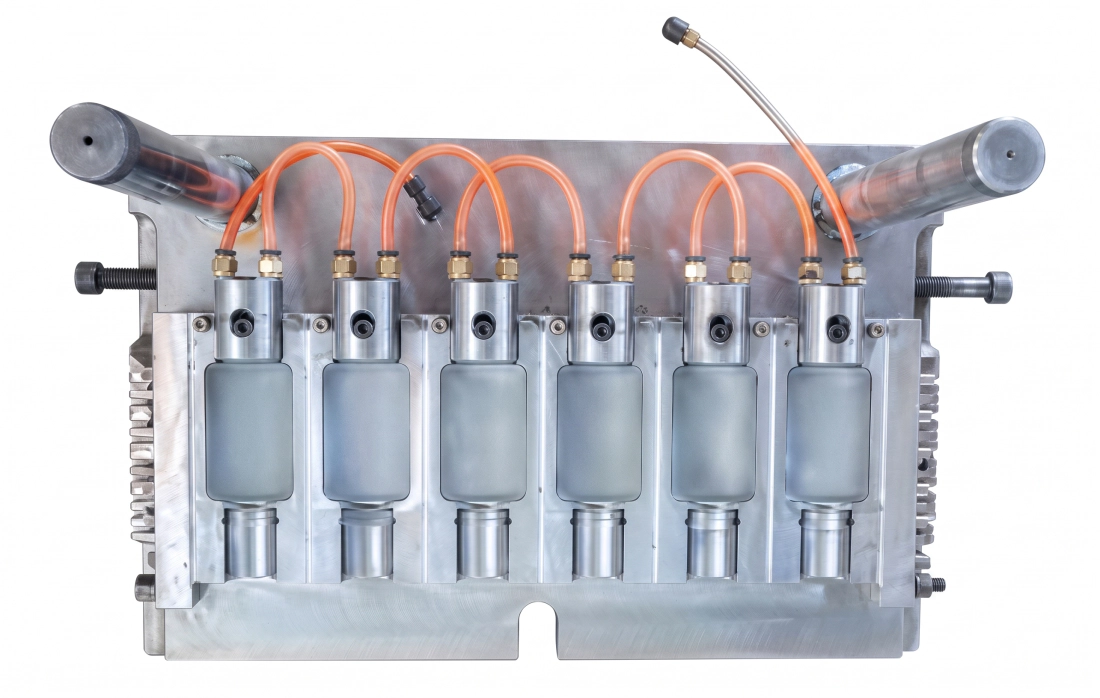
- ■فعال گہا اور گردن بلاک ڈیزائن - انجیکشن مولڈ کیویٹیز اور گردن کے بلاکس آزادانہ طور پر ایڈجسٹ ہوتے ہیں، جس سے پرفارم ٹیوب کے جسم کے طول و عرض کو پورے مولڈ سیٹ کو تبدیل کیے بغیر ٹھیک بنایا جا سکتا ہے۔ تیل اور پانی کے راستے مستحکم درجہ حرارت کی تقسیم اور آسانی سے جدا کرنے کے لیے ڈیزائن کیے گئے ہیں۔
- ■پریمیم سٹیل کے درجات - انجیکشن مولڈ باڈیز 4Cr13 سٹینلیس سٹیل یا امپورٹڈ اعلی طاقت S136 الائے سٹیل استعمال کرتی ہیں۔ S136 ایک آئینہ پولش، سنکنرن مزاحم اسٹیل ہے جس میں 52 HRC تک سختی ہے۔ بلو مولڈ باڈیز کو میگنیشیم-ایلومینیم الائے میں بہتر تھرمل چالکتا اور روٹری برج پر کم جڑتا ماس کے لیے تیار کیا جا سکتا ہے۔
- ■آپٹمائزڈ ہاٹ رنر اور پریفارم ڈیزائن - گرم رنر مینی فولڈ کو تمام گہاوں میں گرام وزن کے انحراف کو کم کرنے اور پیشگی جسم میں دیوار کی موٹائی کے فرق کو کم کرنے کے لیے انجنیئر کیا گیا ہے۔ مینڈریل ڈیزائن مسلسل دھچکے کی توسیع اور تیز ٹھنڈک کے لیے یکساں ہوا کی ترسیل کو یقینی بناتا ہے۔
- ■صحت سے متعلق گردن کے دھاگے اور مہر کے طول و عرض - بوتل کے منہ کے اندرونی اور بیرونی قطر، دھاگے کی پچ اور فلینج جیومیٹری ڈرائنگ رواداری کے لیے مشینی ہیں۔ پروڈکشن سے چلنے والے نمونوں میں کیپ سیلنگ کی شرح 100% ہے۔
- ■گردن اور بیس پر صفر فلیش - the IBM process geometry eliminates parting-line flash at the bottle mouth and pinch-weld flash at the base. Bottles exit the EP110 with no trimming required at either end.
- ■مصنوعات کی مستقل مزاجی کی پیمائش - سائز، وزن، الگ کرنے والی لائن کی پوزیشن اور دیوار کی موٹائی تمام گہاوں اور پروڈکشن بیچوں میں یکساں ہے، جس سے فارماسیوٹیکل کلائنٹس کو 100% انسپکشن اوور ہیڈ کے بغیر فی بیچ شماریاتی بنیاد پر پیداوار کی توثیق کرنے کے قابل بناتا ہے۔
Equipment Selection Guide: Is the EP110 Right for Your Production Requirements?
Selecting the correct IBM tonnage requires calculating the intersection of three variables: preform weight, required cavity count, and target output per hour. Use this framework to confirm whether the EP110 is correctly sized for your application, or to understand what production parameters it can support.
مرحلہ 1: پیشگی وزن کا حساب لگائیں۔
Take the target bottle weight in grams (including the neck, body and base). Add 2-5% for process cushion. The EP110 injection weight of 540 g must be equal to or greater than (target preform weight x number of cavities). For example: a 5g preform at 8 cavities requires 40g shot weight, well within the 540 g capacity.
مرحلہ 2: مطلوبہ گہا کی گنتی کا حساب لگائیں۔
Target output (bottles/hour) divided by (3600 seconds / cycle time in seconds) gives required cavities. At a 4 S cycle and 10,000 bottles per hour target: 10,000 / (3600 / 4) = 12 cavities minimum. Cross-check against the cavity table above to confirm the EP110 can deliver this at your bottle volume.
مرحلہ 3: مولڈ پلیٹن فٹ کی تصدیق کریں۔
The injection mould layout (cavity array footprint) must fit within the EP110 max platen size of 1100x460 mm. Wide-bottle (diameter greater than 120mm) or tall-bottle (height greater than 220mm) applications exceed the EP110 mould envelope and require a larger model. Confirm your bottle OD and height before specifying cavity count.
مرحلہ 4: مواد اور انجکشن کا دباؤ
PP requires higher injection pressure and melt temperature than LDPE. PC and PETG require even higher barrel temperatures and longer residence-time plasticization. The EP110 hydraulic system pressure of 14 MPa and motor of 22+22 KW supports the injection forces needed for PP and engineering grade materials at the rated injection weight. Confirm your resin specification with the EVER POWER application team before ordering.
EVER POWER application engineers provide free pre-sales technical consultation to validate your container dimensions, material, cavity count and production target against EP110 specifications. Contact us with your bottle drawing and production brief for a written confirmation of suitability.
مشین کی ساخت کا جائزہ اور دیکھ بھال کے رہنما خطوط
The EP110 is built around three core functional modules. Understanding their maintenance requirements is essential for sustaining the machine performance metrics - dry cycle, output rate, and product quality - over the full production life of the equipment.
ماڈیول 1 - انجکشن یونٹ: سکرو، بیرل، گرم رنر
انجیکشن یونٹ پلاسٹک کو پگھلتا ہے اور پرفارم گہا میں میٹر کرتا ہے۔ روزانہ کی دیکھ بھال: سیٹ پوائنٹس کے خلاف بیرل کے درجہ حرارت کے پروفائلز کو چیک کریں، سکرو ٹپ کا معائنہ کریں اور پہننے کے اشارے کے لیے انگوٹھی کی جانچ کریں، اور تصدیق کریں کہ ہاٹ رنر زون کا درجہ حرارت شروع ہونے سے پہلے سیٹ پوائنٹس کے 2 ڈگری کے اندر ہے۔ ہفتہ وار: بیرل موصلیت کے بینڈ کا معائنہ کریں، تیل رونے کے لیے انجیکشن سلنڈر کی مہریں چیک کریں، اور پچھلی پیداوار سے کسی بھی رنگ کی آلودگی کو صاف کریں۔ ماہانہ: چیک رنگ اور سکرو ٹپ اسمبلی کو کھینچ کر صاف کریں۔ پہننے کے لیے سکرو فلائٹس کا معائنہ کریں اور کلیئرنس کے لیے بیرل بور کے قطر کی پیمائش کریں۔ بیرل کو تبدیل کریں اگر کلیئرنس مینوفیکچرر کی برداشت سے زیادہ ہو تاکہ پگھلنے والے بائی پاس اور شاٹ وزن میں تضاد کو روکا جا سکے۔
صاف کرنے کا طریقہ کار: جب گہرے سے ہلکے رنگوں میں یا انجینئرنگ رال سے کموڈٹی رال میں تبدیل ہو رہا ہو تو، نئے میٹریل سیٹ پوائنٹ سے 10 ڈگری اوپر بیرل کے درجہ حرارت پر کمرشل صاف کرنے والا کمپاؤنڈ استعمال کریں۔ نئے مواد پر سوئچ کرنے سے پہلے 5-10 پرج شاٹس چلائیں۔ بیرل کو پروسیسنگ درجہ حرارت پر 20 منٹ سے زیادہ کے لیے بغیر صاف کیے کبھی بھی بیکار نہ چھوڑیں - بیکار ادوار کے دوران تھرمل انحطاط دوبارہ شروع ہونے پر کالے دھبے کی آلودگی کی بنیادی وجہ ہے۔
ماڈیول 2 - کلیمپنگ اور روٹری انڈیکسنگ یونٹ
کلیمپنگ سسٹم اور روٹری انڈیکسر سب سے زیادہ مکینیکل بوجھ اٹھاتے ہیں اور سب سے زیادہ درست پوزیشن کے تقاضے ہوتے ہیں۔ روزانہ: چکنائی کو ٹائی بار کی سطحوں اور روٹری ٹیبل گائیڈ ریلوں پر چکنائی کے شیڈول کے مطابق لگائیں (کبھی طاقت چکنائی کے درجے کی وضاحت کرتی ہے - عام مقصد والی چکنائی کے ساتھ متبادل نہ کریں، جو آپریٹنگ درجہ حرارت پر چپکنے والی پن کو برقرار نہیں رکھ سکتی ہے)۔ راڈ سیل پر تیل کے اخراج کے لیے ہائیڈرولک کلیمپنگ سلنڈر کا معائنہ کریں۔ اشاریہ سازی کی گردش کے دوران غیر معمولی آوازیں سنیں - کوئی بھی دھاتی کلک یا ہچکچاہٹ ایک زاویہ تقسیم کرنے والے بیئرنگ کی نشاندہی کرتی ہے جس کے لیے معائنہ کی ضرورت ہوتی ہے۔
ماہانہ: چار ٹائی بار پوزیشنوں پر ڈائل انڈیکیٹر کے ساتھ پلیٹن کے متوازی کو چیک کریں۔ 0.05mm سے زیادہ انحراف کے لیے دوبارہ چمکنے کی ضرورت ہوتی ہے۔ برج پر حوالہ کی سطح کے خلاف ڈائل انڈیکیٹر لگا کر اور اس بات کی تصدیق کرتے ہوئے کہ 100 لگاتار انڈیکسنگ سائیکلوں کے بعد اسی پوزیشن کو 0.02 ملی میٹر کے اندر دہرایا گیا ہے۔ اگر بڑھنے کا مشاہدہ کیا جائے تو، مکینیکل سٹاپ کو ایڈجسٹ کریں یا ایور پاور سروس سے رابطہ کریں۔
ماڈیول 3 - ہائیڈرولک سسٹم اور کولنگ سرکٹ
The hydraulic system is the energy backbone of the EP110. System pressure is set at 14 MPa. Daily: check hydraulic oil level in the tank sight glass, check oil temperature display (normal operating range 40-55 degrees Celsius; above 60 degrees indicates a cooling circuit problem or filter blockage), and inspect all visible hydraulic hose fittings for weeping. The oil filter indicator must be checked every 250 hours - a red indicator requires immediate filter element replacement, not deferral.
Cooling circuit: the EP110 requires clean, scale-free cooling water at 0.3-0.4 MPa pressure and 4 M3/h flow. Install a water treatment system upstream of the machine to prevent calcium scale buildup inside mold cooling channels. Scale buildup of just 1mm in a 6mm channel reduces cooling efficiency by over 30%, extending cycle times and reducing output. Flush cooling circuits with a descaling solution annually. Chiller water quality must be neutral pH (6.5-7.5) and contain an anti-corrosion inhibitor compatible with copper and aluminum alloy mold materials.
ایور پاور سے ٹرنکی سلوشنز اور حسب ضرورت خدمات
EVER POWER supplies the EP110 as either a standalone machine or as the centerpiece of a complete turnkey bottle production line. For customers setting up a new facility or expanding into a new container product line, the turnkey approach eliminates the integration risk that comes from sourcing the IBM machine, molds, auxiliaries, and downstream equipment from separate vendors.
مولڈ ڈیزائن اور مینوفیکچرنگ
ایور پاور انجینئرز کسٹمر بوتل ڈرائنگ یا تھری ڈی فائلوں سے انجکشن اور بلو مولڈ سیٹ تیار کرتے ہیں۔ S136 یا 4Cr13 سٹیل میں ملٹی کیویٹی ہاٹ رنر موڈز۔ پروٹوٹائپ سنگل کیویٹی موڈز کنٹینر کی توثیق کے لیے ہائی کیویٹی پروڈکشن ٹولنگ سے پہلے۔ T0 مولڈ ٹرائلز شپمنٹ سے پہلے فیکٹری میں کیے گئے۔
معاون آلات کا انضمام
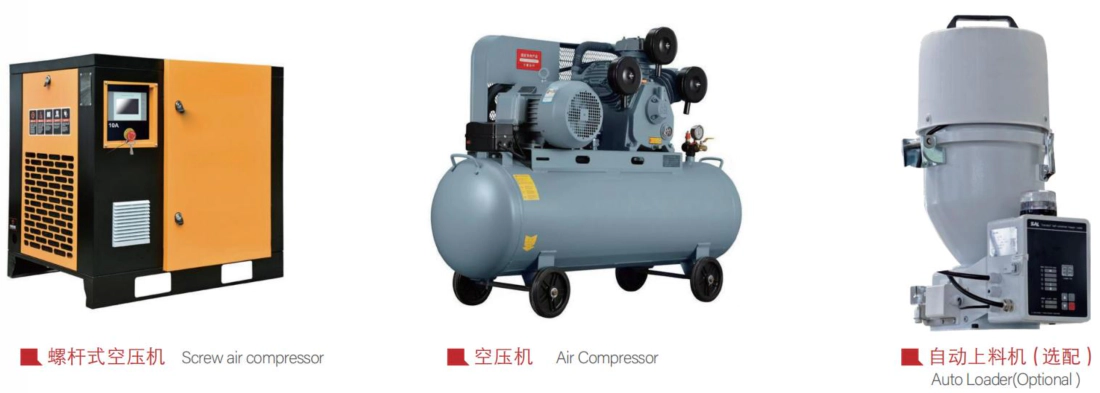
The EVER POWER turnkey line includes: screw air compressor, air tank and air dryer, mold temperature controller, industrial chiller, auto loader, conveyor belt, screen printing and labeling system, washing and drying line, and automatic filling and capping machines. All auxiliary equipment is specified and pre-integrated to match the EP110 output rate.
ڈاؤن اسٹریم کوالٹی سسٹمز
Optional inline bottle visual inspection machine (machine vision system for flash, deformation and contamination detection), automatic leak tester, automatic packing machine, and carton erector. For pharmaceutical lines, 100% inline leak testing and vision inspection are available as integrated modules matched to the EP110 conveyor output speed.
جی ایم پی اور کلین روم کنفیگریشن
فارماسیوٹیکل کلائنٹس کے لیے جن کو GMP-گریڈ پروڈکشن کی ضرورت ہوتی ہے، EVER POWER مشین کو حسب ضرورت پیش کرتا ہے بشمول: پروڈکٹ زون کی آلودگی کو روکنے کے لیے بند نظام کی چکنا، سٹینلیس سٹیل کے حفاظتی انکلوژرز، کلاس 100,000 کلین روم کی مطابقت کے لیے HEPA فلٹرڈ مشین انکلوژر، اور آلات کے لیے کوالیفیکیشن سپورٹ (QIQ/Ocol)
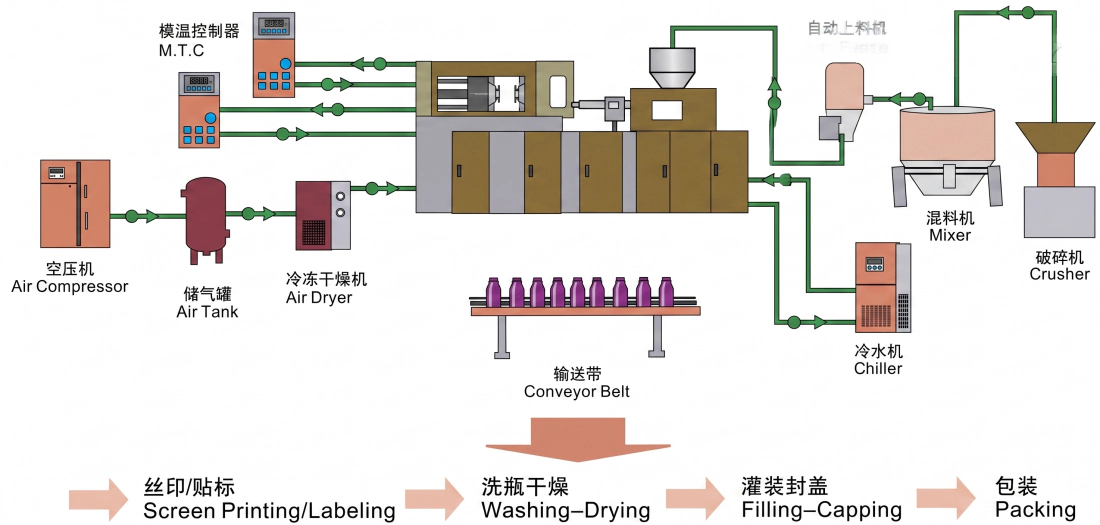
Auxiliary Equipment Available with the EP110
کوالٹی کنٹرول اور مینوفیکچرنگ کے معیارات
اہم اجزاء کی CNC مشینی
جیومیٹرک درستگی کی ضمانت کے لیے مشینی بستر، کلیمپنگ پلاٹین، اور تمام درست سطحوں کو سنگل سیٹ اپ میں CNC مشین سے بنایا گیا ہے۔ پلیٹن کے متوازی کی تصدیق لیزر پیمائش سے 0.02 ملی میٹر تک ہوتی ہے۔ مداخلت سے پاک بیئرنگ فٹ ہونے کے لیے ٹائی بار کے بوروں کو H7 رواداری کے مطابق بنایا جاتا ہے۔
ٹائی بار انڈکشن سخت کرنا
ٹائی بارز 52-58 HRC کی سطح کی سختی کے لیے ہائی فریکوئنسی انڈکشن سختی سے گزرتی ہیں اور اس کے بعد درست پیسنا ہوتا ہے۔ یہ سطحی علاج لاکھوں چکروں میں کلیمپنگ پلیٹین کے بار بار سلائیڈنگ رابطے کے خلاف لباس کی مزاحمت فراہم کرتا ہے بغیر کسی گھبراہٹ کے۔
ہائیڈرولک سرکٹ کی صفائی
تمام ہائیڈرولک سرکٹس کو فلش کیا جاتا ہے، پریشر ٹیسٹ کیا جاتا ہے اور اسمبلی سے پہلے پارٹیکل کاؤنٹ کی تصدیق کی جاتی ہے۔ ہائیڈرولک تیل کی صفائی کو کم از کم ISO 4406 کلاس 17/15/12 پر برقرار رکھا جاتا ہے۔ متناسب اور سرو والو آلودگی کی حساسیت کے لیے اس سطح کی صفائی کی ضرورت ہوتی ہے تاکہ والو اسپول کے چپکنے اور بڑھنے کو کنٹرول کیا جا سکے۔
72 گھنٹے کا فیکٹری رن ان ٹیسٹ
Every EP110 undergoes a minimum 72-hour continuous loaded run test at the factory before shipment. During this period, production output samples are measured for weight consistency, wall thickness uniformity, and dimensional accuracy. Any parameter outside specification triggers a hold and corrective action before the machine is cleared for delivery.
سی ای سیفٹی کی تعمیل
The EP110 is CE-marked in compliance with EU Machinery Directive requirements. Safety features include: interlocked safety doors with hydraulic circuit interrupt, light curtain protection at the operator access zone, emergency stop at all operator positions, and two-hand operator control for manual mold setting. CE documentation is provided with every machine.
فروخت کے بعد سروس اور تکنیکی مدد
تنصیب اور کمیشننگ
ایور پاور سینئر انجینئرز انسٹالیشن، کمیشننگ اور قبولیت کی جانچ کے ذمہ دار ہیں۔ انجینئر اس وقت تک سائٹ پر رہتا ہے جب تک کہ مشین مستحکم پیداواری حالت حاصل نہیں کر لیتی اور تمام آپریٹرز کو مشین کے آپریشن، مولڈ کی تبدیلی اور معمول کی دیکھ بھال کی تربیت دی جاتی ہے۔ قبولیت کے معیار پر شپمنٹ سے پہلے اتفاق کیا جاتا ہے اور کمیشننگ رپورٹ میں دستاویزی کیا جاتا ہے۔
بچاؤ کی بحالی کا پروگرام
ایور پاور سروس میں موجود تمام مشینوں کے لیے ایک طے شدہ دیکھ بھال کی یاد دہانی کی خدمت فراہم کرتا ہے۔ بحالی کیلنڈر روزانہ، ہفتہ وار، ماہانہ اور سالانہ کاموں کا احاطہ کرتا ہے۔ فعال دیکھ بھال غیر منصوبہ بند خرابیوں کو روکتی ہے اور مہنگے ہنگامی حصوں کی ترسیل کی ضرورت کو کم کرتی ہے۔ احتیاطی دیکھ بھال کے شیڈول کی پیروی کرنے والے صارفین مسلسل 95% سے اوپر مشین کی دستیابی کی اطلاع دیتے ہیں۔
24x7 سروس ہاٹ لائن
ایور پاور سروس ہاٹ لائن دن کے 24 گھنٹے، ہفتے کے 7 دن دستیاب ہے۔ فوری پروڈکشن خرابی کے لیے، سروس لائن کو کال کریں یا میسج کریں اور ایک مستند انجینئر 2 گھنٹے کے اندر جواب دے گا تاکہ دور سے مسئلہ کی تشخیص کی جا سکے۔ اگر آن سائٹ سروس درکار ہو تو، ایور پاور آپ کے مقام کے لیے دستیاب کم از کم رسپانس ٹائم کے ساتھ ٹیکنیشن بھیجتا ہے۔
اسپیئر پارٹس کی انوینٹری
EVER POWER maintains a comprehensive spare parts inventory for all EP110 components including hydraulic seals, proportional valve cartridges, heating bands, temperature sensors, drive belts and electrical components. Parts can be shipped globally within 48 hours for items in stock. Critical fast-wear items are available for customer-held local inventory based on EVER POWER recommendations.
تکنیکی تربیتی پروگرام
معیاری تنصیب کی تربیت کے علاوہ، ایور پاور وقف تربیتی ماڈیولز پیش کرتا ہے: مشین آپریشن، مولڈ پروسیس آپٹیمائزیشن، مولڈ چینج اور سیٹ اپ، ہائیڈرولک سسٹم مینٹیننس، اور مخصوص مواد جیسے PP، LDPE اور PCTG کے لیے پراسیس ٹربل شوٹنگ۔ تربیت ایور پاور فیکٹری یا کسٹمر کی سہولت پر منعقد کی جا سکتی ہے۔
Frequently Asked Questions - EVER POWER EP110
What materials can the EP110 process?
The EP110 is compatible with HDPE, LDPE, PP, PS (including lactic acid bacteria grade transparent PS), ABS, EVA, bio-based corn material, PCTG, and similar thermoplastics. For engineering resins such as PC, PETG and Tritan, the screw L/D of 22:1 and the 5+N heating zones provide the residence time and temperature profile needed for thorough, degradation-free plasticization. Confirm your resin grade with EVER POWER application engineering before ordering.
Can the EP110 be used for pharmaceutical GMP production?
Yes. The EP110 can be configured for pharmaceutical GMP production environments. Key features supporting GMP include: the one-step process eliminates inter-machine bottle transfer that introduces contamination risk in two-stage systems; the closed lubrication system prevents lubricant contamination of the product zone; and the machine can be specified with a stainless steel safety enclosure suitable for cleanroom installation. EVER POWER can provide equipment documentation to support IQ/OQ/PQ qualification processes for pharmaceutical facility validation.
How long does mould changeover take on the EP110?
A trained two-person team can complete a full mold changeover (injection mold, blow mold, and mandrel set) on the EP110 in approximately 2-4 hours, depending on the mold design and the changeover frequency experience of the team. PLC recipe recall eliminates parameter re-entry time for repeat mold sets. Facilities that invest in quick-release clamping plates for the mold base can reduce changeover to under 2 hours.
What certifications does the EP110 carry?
The EP110 is CE-marked for the European market. The machine design complies with EU Machinery Directive safety requirements including interlocked guards, emergency stop systems, and electrical safety standards. EVER POWER is an ISO-certified manufacturer. Machine documentation is provided in English and can be supplied in other languages upon request for export markets.
What is the lead time for the EP110 and an associated mould set?
Standard machine lead time for the EP110 is 45-75 days from order confirmation and deposit receipt, depending on production schedule at time of order. Mold sets are typically supplied in 60-90 days from final confirmation of bottle drawings and material specification. The machine and mold sets can be scheduled to arrive simultaneously for a coordinated installation. Contact EVER POWER for current lead time at time of inquiry.
Ready to Specify the EVER POWER EP110 for Your Production Line?
اپنی بوتل کی ڈرائنگ، ہدف کا حجم، مواد کی تفصیلات اور فی گھنٹہ مطلوبہ آؤٹ پٹ ہماری ایپلی کیشن انجینئرنگ ٹیم کو بھیجیں۔ ہم گہا کی درست گنتی اور مشین کی ترتیب کی تحریری طور پر تصدیق کریں گے اور 3 کام کے دنوں کے اندر ایک تفصیلی تجارتی تجویز فراہم کریں گے۔
اضافی معلومات
| ترمیم شدہ | hyw کی طرف سے |
|---|
متعلقہ مصنوعات
-
EP60HE ہائی سپیڈ مکمل طور پر الیکٹرک انجکشن بلو مولڈنگ مشین زیرو ہائیڈرولک 2.5s سائیکل
-
کاسمیٹک دواسازی کی بوتلوں کے لیے ہیوی ڈیوٹی انجکشن بلو مولڈنگ مشین EP135 1350KN ہائی کیوٹی IBM
-
ہائی آؤٹ پٹ انجکشن بلو مولڈنگ مشین EP80 800KN فلیش فری بوتل مولڈنگ کا سامان
-
خودکار ون سٹیپ انجکشن بلو مولڈنگ مشین EP60 600KN فارما کاسمیٹک بوتل بنانے والا
-
فارما کاسمیٹک بوتلوں کے لیے خودکار ایک قدمی انجکشن بلو مولڈنگ مشین EP40 400KN CE ISO


