
Mesin Cetak Tiup Injeksi Industri EP110 1100KN Peralatan IBM Otomatis untuk Botol Bervolume Besar
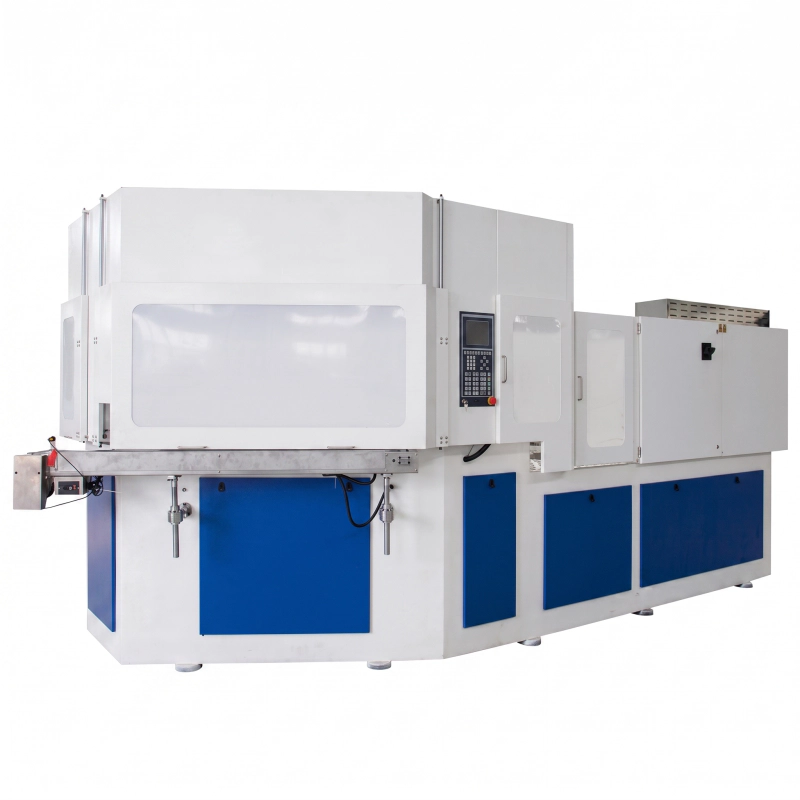
EVER POWER EP110 injection blow molding machine delivers 1100KN clamping force, 540g injection weight and up to 24 cavities for 10ml bottles. Standard dual hydraulic system, high-precision angle divider, 4s dry cycle. Suitable for 1-2000ml pharmaceutical, cosmetic and daily chemical containers. 15 Ton, CE ISO, 80KW total power.
What Is the EVER POWER EP110 One-Step Injection Blow Molding Machine?
The EVER POWER EP110 is a fully automatic one-step IBM (Injection Blow Molding) machine engineered for precision hollow container production. As a dedicated produsen mesin cetak tiup injeksiEVER POWER telah memusatkan keahlian puluhan tahun dalam bidang perkakas dan proses ke dalam model ini, menghadirkan mesin di mana seluruh botol - dari injeksi preform hingga peniupan akhir hingga pengeluaran - diselesaikan dalam satu siklus mesin tanpa intervensi operator, tanpa transfer material antar mesin, dan tanpa sisa material dan limbah garis pemisah yang menjadi ciri sistem peniupan ekstrusi.
Ini mesin IBM satu langkah is the preferred choice for pharmaceutical bottle blowing and cosmetic container manufacturing where dimensional consistency is non-negotiable. Each cycle on the EP110 runs three simultaneous operations: while new preforms are being injection-molded at Station 1, the previous batch is being blown to final shape at Station 2, and the completed bottles from Station 2 are being stripped and conveyed to the outfeed conveyor at Station 3. This triaxial parallelism means the productive output equals the injection cycle time alone - not the sum of injection plus blowing plus ejection - giving the EP110 a significant throughput advantage over two-stage stretch blow systems for small and medium volume containers.
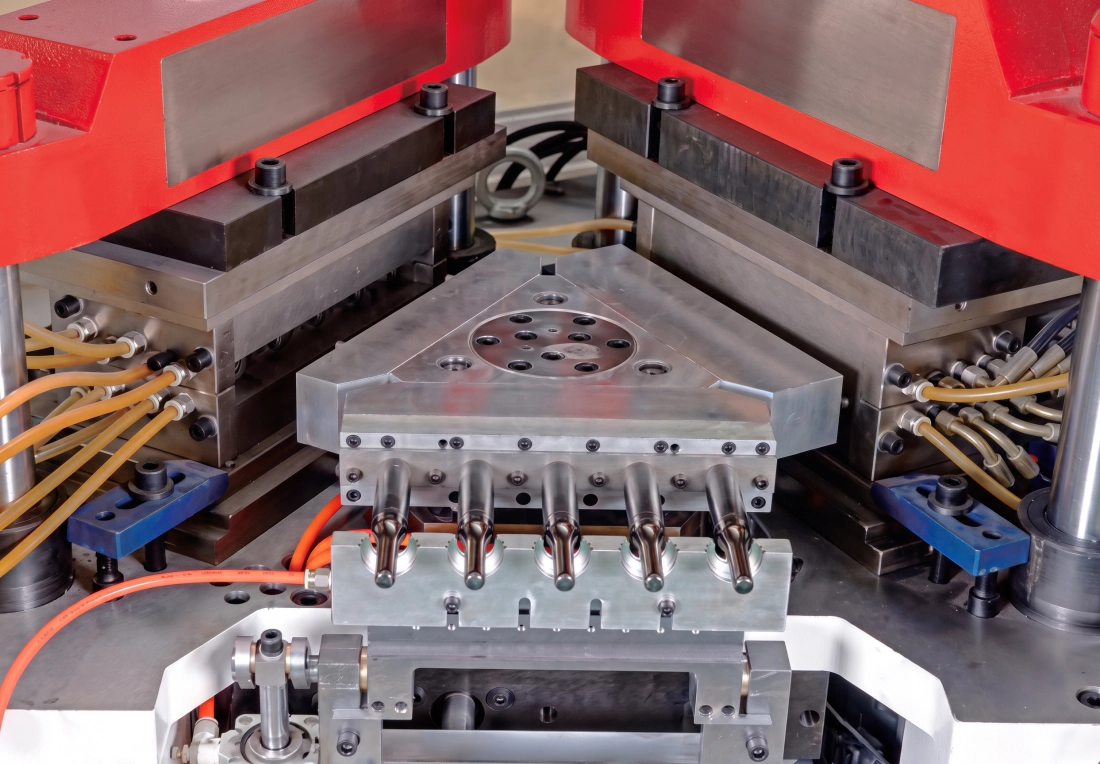
Three-Station Process: How the EP110 Works
Stasiun 1 - Injeksi Preform
Butiran plastik dilelehkan di dalam tabung dan disuntikkan ke dalam rongga injeksi di bawah tekanan terkontrol. Leher botol dan geometri ulir dibentuk secara presisi di dalam cetakan injeksi. Cetakan injeksi terbuka dan mandrel yang membawa preform panas berpindah ke Stasiun 2 melalui turret putar.
Stasiun 2 - Pencetakan Tiup
Preform panas dipompa dengan udara bertekanan dari inti mandrel. Bentuk botol ditentukan sepenuhnya oleh rongga cetakan tiup. Udara memompa preform ke luar melawan dinding cetakan yang telah didinginkan, dan botol tersebut mengambil dimensi akhirnya. Cetakan terbuka dan turret bergerak maju ke Stasiun 3.
Stasiun 3 - Pengeluaran dan Pengangkutan
Botol-botol yang sudah jadi dan dingin dilepas dari mandrel dan dikeluarkan ke konveyor pengeluaran. Karena ketiga stasiun beroperasi secara bersamaan, siklus berulang terus menerus. Tidak ada operasi sekunder, tidak ada mesin penghilang sisa cetakan, dan tidak ada pemanasan ulang botol yang diperlukan - ketiga operasi tersebut menggunakan satu siklus waktu yang sama.
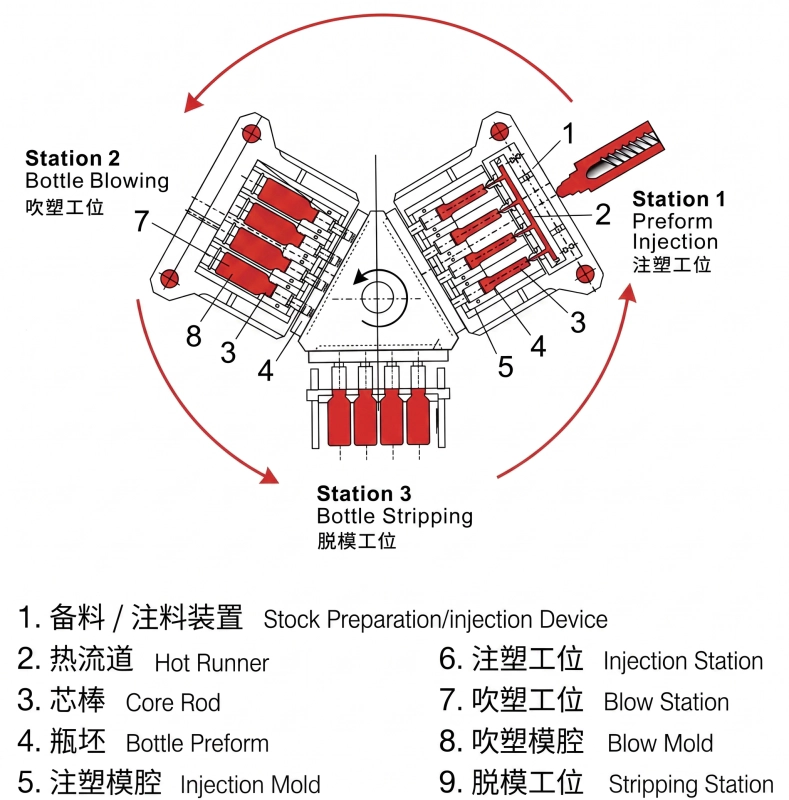
Main Technical Parameters - EVER POWER EP110
| Parameter | Item (EN) | Satuan | EP110 |
|---|---|---|---|
| Sistem Injeksi | |||
| Diameter Sekrup | Diameter Sekrup | mm | 65 mm |
| Rasio Panjang/Kedalaman Sekrup | Sekrup L/D | - | 22:1 |
| Berat Injeksi | Berat Injeksi | G | 540 g |
| Daya Pemanas | Daya Pemanas | KW | 20 KW |
| Zona Pemanasan Tong | Jumlah Zona Barel | - | 5+N |
| Langkah Injeksi | Langkah Injeksi | mm | 200 mm |
| Sistem Penjepit | |||
| Gaya Jepit Injeksi | Gaya Jepit Injeksi | KN | 1100 |
| Langkah Pembukaan Injeksi | Langkah Pembukaan untuk Injeksi | mm | 140 mm |
| Gaya Jepit Tiup | Gaya Jepit Tiupan | KN | 150 |
| Pukulan Pembuka | Langkah Pembuka untuk Meniup | mm | 140 mm |
| Tinggi Lift Menara | Tinggi Angkat Meja Putar | mm | 70 mm |
| Cetakan | |||
| Ukuran Pelat Maksimum (PxL) | Ukuran Pelat Maksimum (P x L) | mm | 1100x460 mm |
| Ketebalan Cetakan | Ketebalan Cetakan | mm | 280 mm |
| Diameter Botol Maksimum | Diameter Botol | mm | 120 mm |
| Tinggi Botol Maksimum | Tinggi Botol | mm | 220 mm |
| Kisaran Volume Botol | Volume Botol yang Sesuai | ml | 1-2000 |
| Gerakan Mengupas | Gerakan Mengupas | mm | 260 mm |
| Sistem Hidrolik | |||
| Tekanan Hidraulik | Tekanan Hidraulik | MPa | 14 |
| Tenaga Motor | Tenaga Motor | KW | 22+22 KW |
| Waktu Siklus Pengeringan | Siklus Kering | S | 4 |
| Daya Total | Daya Total | KW | 80 |
| Daya Operasi | Daya Operasi | % | 52-70 |
| Parameter Lainnya | |||
| Tekanan Udara Terkompresi | Tekanan Udara Minimum | MPa | 0.7-1.2 |
| Kapasitas Udara | Kapasitas Udara Terkompresi | M3/menit | 0.7 |
| Aliran Air Pendingin | Aliran Air | M3/jam | 4 |
| Tekanan Air Pendingin | Tekanan Air Pendingin | MPa | 0.3-0.4 |
| Dimensi (P x L x T) | Dimensi Keseluruhan | M | 5x1.8x2.2 M |
| Berat Bersih | Berat Bersih | Ton | 15 Ton |
Catatan: Semua parameter hanya sebagai referensi. EVER POWER berhak untuk mengubah spesifikasi karena peningkatan peralatan.
Max Cavity Count per Container Volume (EP110 - For Reference)
| Volume | 10 ml | 30 ml | 60 ml | 100 ml | 250 ml | 500 ml | 1000 ml |
|---|---|---|---|---|---|---|---|
| Maksimum Rongga | 24 | 22 | 18 | 14 | 10 | 8 | 6 |
Core Hardware Architecture of the EP110
Rangka Baja Bergaya Eropa Sepenuhnya
CNC-machined monolithic machine bed and platen mounts ensure parallelism between injection and blow clamping platens. Tie-bar surfaces are induction-hardened. The EP110 clamping force is 20-30% above equivalent-tonnage competitors due to the boosted pressurized clamping structure.
Sekrup dan Laras Bimetal
The plasticizing unit uses a bimetallic-lined barrel and a hardened alloy screw rated for glass-fiber and mineral-filled compounds. The EP110 screw diameter of 65 mm at 22:1 L/D delivers thorough homogenization with a 540 g shot capacity, covering the full range of bottle weights for this tonnage class.
Kontrol Hidraulik Katup Proporsional
Tekanan injeksi dan tekanan tiup diatur melalui katup hidrolik servo-proporsional. Hal ini memungkinkan profil injeksi multi-tahap (kecepatan pengisian, peralihan, tekanan pemadatan) untuk preform berdinding tipis, dan kontrol peningkatan tekanan tiup yang presisi yang menghilangkan cacat pembentukan jaring radial yang umum terjadi pada sistem katup tiup satu tahap.
Sistem Kontrol Layar Sentuh PLC
The EP110 control panel runs a full-color PLC touch-screen with parameter recipe storage. All process variables - temperatures, pressures, velocities, timings - are set and monitored from a single screen. Alarm history, production counters and fault codes are logged and displayed in real time.
Sistem Hot Runner yang Dioptimalkan
Manifold hot runner cetakan injeksi dirancang untuk aliran tanpa zona mati, memastikan penyimpangan berat gram di semua rongga diminimalkan. Akurasi kontrol suhu hingga plus atau minus 1 derajat mencegah degradasi material yang sensitif terhadap panas dan sangat penting untuk kejernihan yang konsisten pada wadah transparan.
Desain Batang Inti Khusus
The mandrels (core rods) feature internal cooling channels that reduce core temperature between the injection and blow stations, accelerating the cooling phase. Fast-cycle mandrels enable the EP110 to achieve a 4 S dry cycle without sacrificing preform cooling uniformity or dimensional stability.
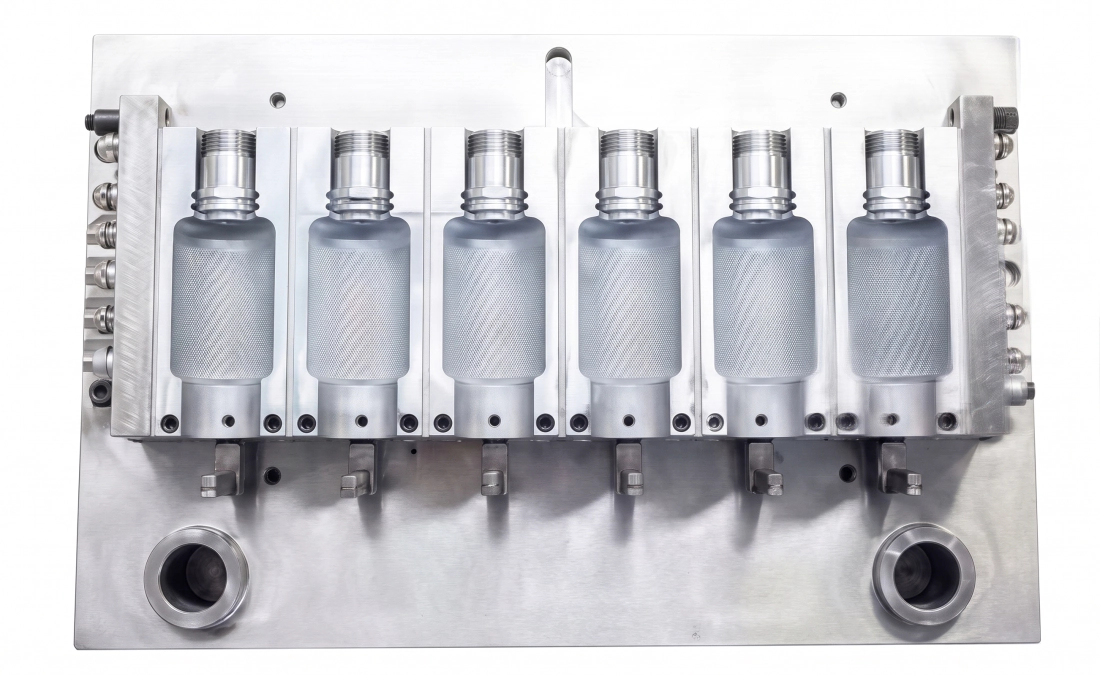
Pencetakan Tiup Injeksi vs. Pencetakan Tiup Ekstrusi: Mengapa IBM Unggul dalam Kontainer Presisi
Buyers evaluating hollow container equipment often compare IBM and EBM on capital cost alone. The EP110 is more than a machine choice - it is a process choice that determines your long-term production economics and the quality ceiling your facility can achieve. The comparison below reflects real production differences that directly affect your cost per thousand bottles and your ability to win pharmaceutical and cosmetic supply contracts.
| TIDAK. | Item Perbandingan | Injeksi Tiup (IBM) | Ekstrusi Tiup (EBM) |
|---|---|---|---|
| 1 | Konsistensi Berat Botol | Variasi berat sekitar 1% | Variasi berat sekitar 3% |
| 2 | Keseragaman Ketebalan Dinding | Ketebalan dinding seragam di seluruh bagian | Ketebalan dinding bervariasi 10-20% |
| 3 | Leher Botol / Ulir | Tidak ada kilatan cahaya, tidak ada garis belahan di leher. | Tanda terpotong, dasar dan leher yang melemah |
| 4 | Kekonveksitas Dasar | Konveksitas positif yang kuat, dasar yang stabil. | Cembung yang lemah karena pengelasan jepit |
| 5 | Limbah Material | Nol limbah - tanpa sisa atau sampah | 20-40% sisa dari kilatan jepit |
| 6 | Kemampuan Dinding Ultra Tipis | Kurang cocok untuk dinding yang sangat tipis. | Ketebalan dinding dapat disesuaikan melalui pengontrol. |
| 7 | Sensitivitas Lingkungan | Tidak sensitif terhadap perubahan lingkungan sekitar. | Penyesuaian sering diperlukan |
| 8 | Jumlah Rongga dan Keluaran | Kavitasi tinggi, hasil tinggi, mulut datar | Jumlah rongga lebih sedikit, output lebih rendah, leher tidak rata. |
| 9 | Masa Pakai dan Biaya Cetakan | Masa pakai cetakan yang panjang, cocok untuk produksi dalam jumlah besar secara berkelanjutan. | Masa pakai cetakan lebih pendek, biaya awal lebih rendah |
| 10 | Tapak | Sistem terintegrasi yang ringkas, ukuran kecil. | Lebih banyak peralatan pendukung, luas lantai lebih besar. |
| 11 | Pembentukan Wadah Oval | Membentuk bentuk oval lebih menantang. | Lebih mudah membentuk profil oval |
Application Fields and Container Types for the EP110
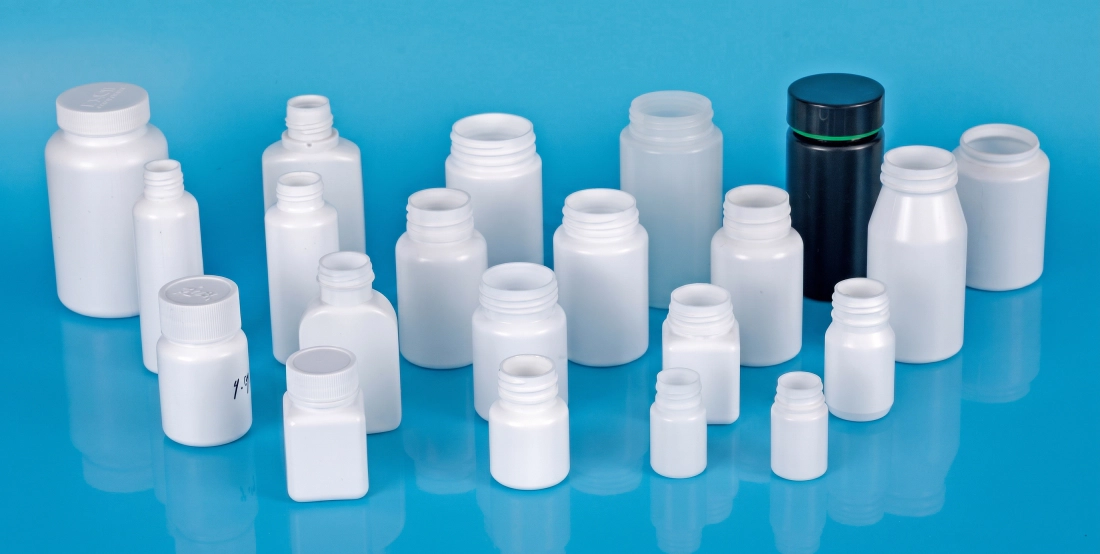
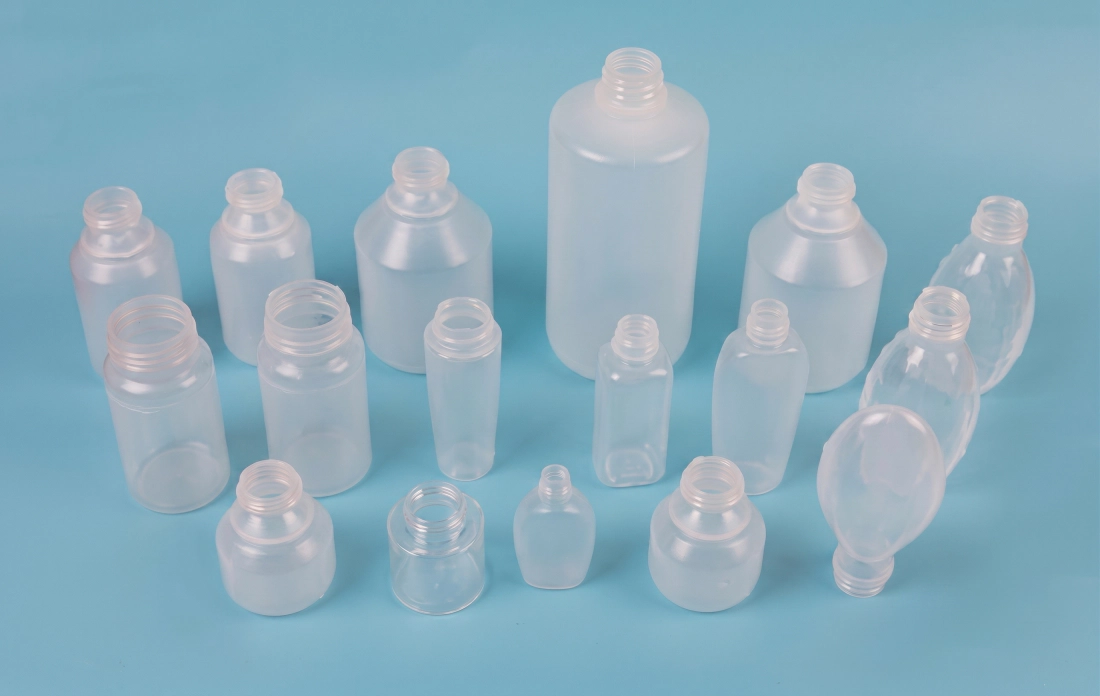
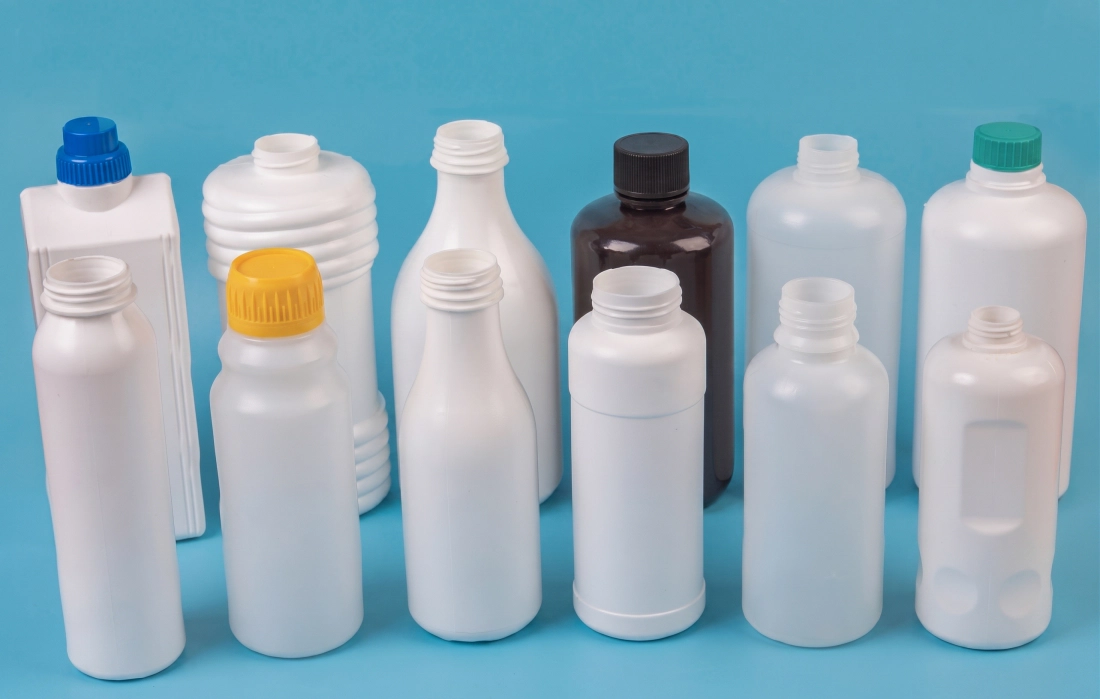
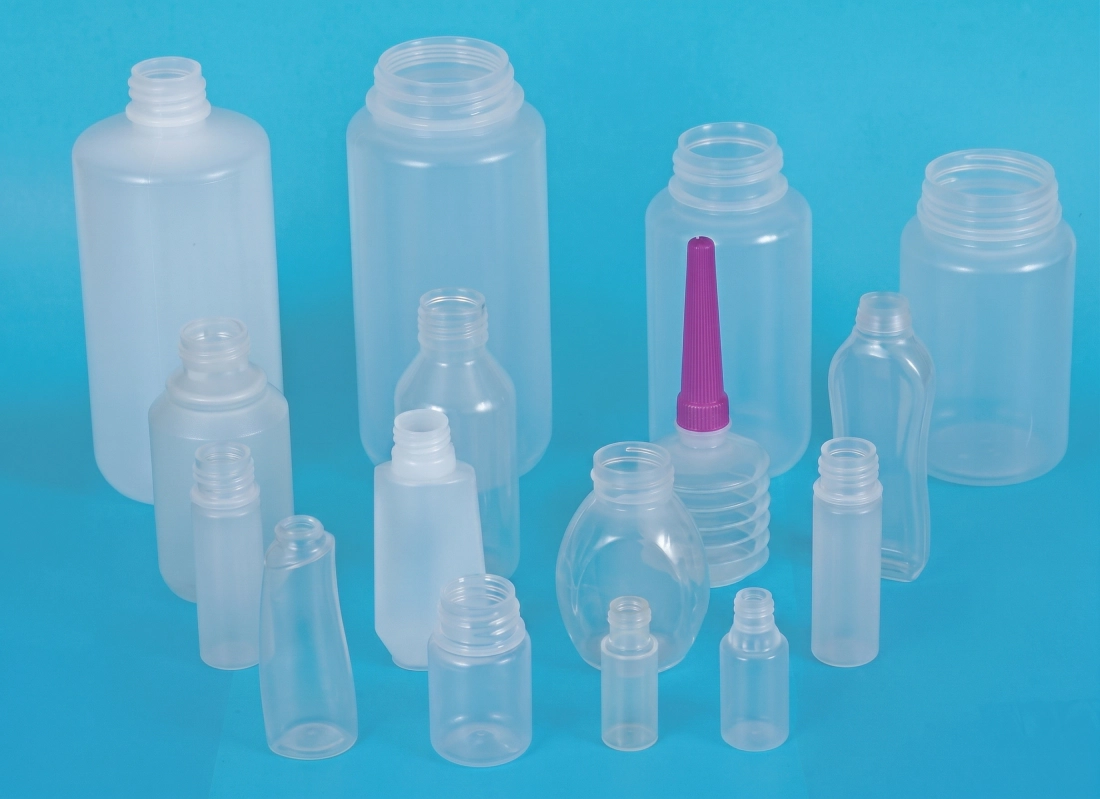
The EP110 is designed to produce bottles and containers from 1ml to the maximum volume for this model, covering the full range of primary packaging needs across four major market verticals. The table below shows the container types and industry segments where this peralatan pencetakan tiup injeksi otomatis menghasilkan pengembalian komersial tertinggi.
Industri Farmasi
- Botol tetes mata (LDPE, 5-30ml)
- Botol tablet dan kapsul oral (HDPE, 30-500ml)
- Semprotan hidung dan botol pompa (PP)
- Botol obat cair dengan tutup pengaman anak.
- Vial vaksin dan reagen (LDPE, 1-20ml)
- Botol pil HDPE berwarna kuning dan putih berstandar GMP.
Industri Kosmetik
- Botol aplikator deodoran roll-on (PE, 50-100ml)
- Tabung maskara dan botol aplikator (PP, 5-20ml)
- Botol cat kuku (PS, 10-30ml)
- Botol pompa losion dan serum (PCTG, 30-200ml)
- Stoples krim bermulut lebar (PP/PS)
- Botol alas bedak dan toner
Produk dan Makanan Bayi
- Botol susu bayi (PP, PPSU, 150-300ml)
- botol sendok susu formula bayi
- Wadah madu dan sirup (LDPE)
- Wadah minuman khusus bervolume kecil
- Botol sampel minyak goreng
- Kemasan yogurt dan produk susu
Kimia dan Industri Harian
- Botol sampo dan kondisioner (HDPE/PP)
- Dispenser pembersih tangan dan losion
- Botol sampel cairan otomotif
- Botol konsentrat bahan kimia pertanian
- Wadah produk pembersih
- Botol reagen industri dengan leher yang presisi
Industrial Connectivity and Remote Diagnostics for the EP110
The EP110 is equipped with a PLC-based control platform that supports recipe management for multiple mold configurations. Each mold set - defined by its preform weight, blow pressure profile, cooling time and stripping sequence - can be saved as a named production recipe and recalled in under 60 seconds during a mold changeover. For OEM and contract manufacturers running 10 or more SKUs on a single machine, this eliminates the operator setup errors that traditionally cause the first 200-500 bottles of a new run to fall outside specification.
The control system logs cycle time, injection pressure peak, clamp force, motor amperage and hydraulic oil temperature for every production cycle. This real-time data stream can be connected to a factory SCADA system via standard industrial protocols. For overseas customers, EVER POWER engineers can connect to the machine remotely to review alarm logs, adjust process parameters, and guide local operators through fault recovery without requiring an on-site service visit - substantially reducing downtime cost for facilities far from a service center.
Energy monitoring is built into the EP110 dashboard: cumulative kWh consumption per production batch, energy cost per thousand bottles (configured with local electricity price), and OEE (Overall Equipment Efficiency) tracking across shifts. This data enables production managers to identify energy anomalies - such as a worn hydraulic seal increasing pump load - before they escalate into unplanned downtime. The transition from reactive maintenance to condition-based maintenance is one of the most significant cost reduction levers available to high-volume bottle manufacturers, and the EP110 makes it accessible without third-party hardware investment.
Investment Return and Production Efficiency Analysis: Why Choose the EP110?
The acquisition cost of the EP110 must be evaluated against five measurable efficiency drivers that determine cost per thousand bottles and payback period. Purchasing engineers who evaluate only machine price - without these five factors - systematically undervalue the IBM platform and overestimate EBM economics for their target application.
1. Nol Limbah Flash
IBM tidak menghasilkan sisa produk (flash) dan tidak ada sisa produk di garis sambungan. EBM menghasilkan sisa produk seberat 20-401 TP3T per siklus. Dengan produksi 200 ton PP per tahun, IBM yang tanpa sisa produk menghemat 40-80 ton resin setiap tahunnya. Dengan harga 1.500 USD per ton, itu berarti penghematan bahan baku sebesar 60.000-120.000 USD per tahun hanya dari satu mesin saja.
2. Tidak ada tenaga kerja untuk menghilangkan sisa-sisa kapal yang terbakar.
EBM requires a secondary deflashing operation - either inline mechanical or manual - adding labor cost, a second machine footprint, and an additional quality failure point. IBM bottles from the EP110 come off the conveyor with zero post-processing required before filling or labeling, saving 1-3 operators per shift.
3. Siklus Pengeringan Singkat
The EP110 achieves a 4 S dry cycle. With 18 cavities at 60ml, annual output at 6,000 hours run time exceeds 97.0 million bottles. This throughput concentration into a single compact machine reduces total asset investment per unit of capacity versus multi-machine EBM lines at equivalent output.
4. Pergantian Cetakan Cepat
The injection mold and blow mold on the EP110 can be changed in 2-4 hours by a trained two-person team. Recipe recall from the PLC removes setup time entirely for repeat jobs. Facilities running 8-15 SKUs on a single EP110 achieve mold changeover frequency of 2-4 per week with total changeover downtime below 10% of available production hours.
Jejak Karbon dan Efisiensi Utilitas
The EP110 footprint of 5x1.8x2.2 M consolidates injection, blow and ejection into a single machine envelope. Compare this to a two-machine EBM line (extruder plus blow machine, plus deflash press, plus conveyor) which typically occupies 3-4 times the floor area for equivalent throughput. Utility connections - compressed air at 0.7-1.2 MPa, cooling water at 4 M3/h flow, electrical connection at 80 KW total - are all single-point utilities, reducing installation complexity and ongoing maintenance overhead.
Factory building cost in pharmaceutical-grade cleanroom environments can reach 2,000-5,000 USD per square meter. The compact footprint of the EP110 directly reduces the cleanroom area required to produce a given volume of output - a capital benefit that does not appear in machine comparison tables but materially affects total project economics.
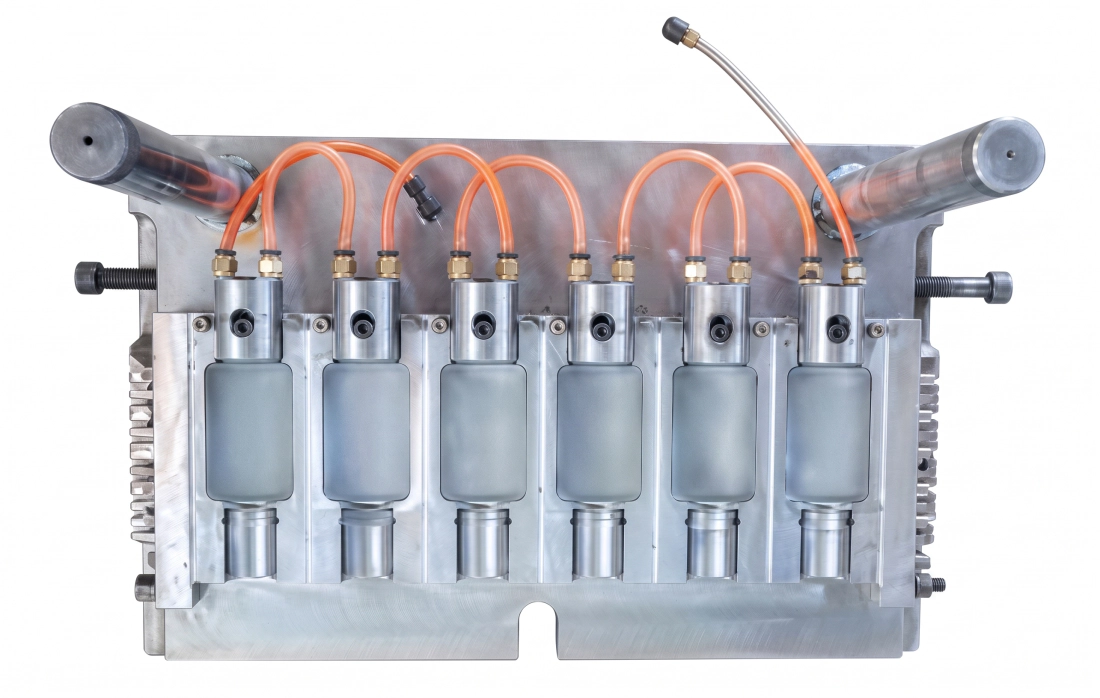
Karakteristik dan Standar Desain Cetakan Seri EP IBM
- ■Desain rongga aktif dan blok leher - Rongga cetakan injeksi dan blok leher dapat disesuaikan secara independen, memungkinkan dimensi badan tabung preform disesuaikan dengan tepat tanpa mengganti seluruh set cetakan. Saluran minyak dan air dirancang khusus untuk distribusi suhu yang stabil dan pembongkaran yang mudah.
- ■Baja kelas premium - Badan cetakan injeksi menggunakan baja tahan karat 4Cr13 atau baja paduan S136 berkekuatan tinggi impor. S136 adalah baja tahan korosi dengan permukaan yang dipoles seperti cermin dan kekerasan hingga 52 HRC. Badan cetakan tiup dapat diproduksi dari paduan magnesium-aluminium untuk konduktivitas termal yang unggul dan massa inersia yang lebih rendah pada turret putar.
- ■Desain hot runner dan preform yang dioptimalkan. - Manifold hot runner dirancang untuk meminimalkan penyimpangan berat gram di semua rongga dan mengurangi variasi ketebalan dinding pada badan preform. Desain mandrel memastikan pengiriman udara yang seragam untuk ekspansi tiup yang konsisten dan pendinginan yang cepat.
- ■Dimensi ulir dan segel leher yang presisi - Diameter dalam dan luar mulut botol, jarak ulir, dan geometri flensa dikerjakan dengan mesin sesuai toleransi gambar. Tingkat penyegelan tutup adalah 100% di seluruh sampel produksi.
- ■Tidak ada kilatan cahaya di bagian leher dan dasar. - the IBM process geometry eliminates parting-line flash at the bottle mouth and pinch-weld flash at the base. Bottles exit the EP110 with no trimming required at either end.
- ■Metrik konsistensi produk - Ukuran, berat, posisi garis pemisah, dan ketebalan dinding konsisten di semua rongga dan di seluruh batch produksi, memungkinkan klien farmasi untuk memvalidasi produksi secara statistik per batch tanpa biaya tambahan inspeksi 100%.
Equipment Selection Guide: Is the EP110 Right for Your Production Requirements?
Selecting the correct IBM tonnage requires calculating the intersection of three variables: preform weight, required cavity count, and target output per hour. Use this framework to confirm whether the EP110 is correctly sized for your application, or to understand what production parameters it can support.
Langkah 1: Hitung Berat Preform
Take the target bottle weight in grams (including the neck, body and base). Add 2-5% for process cushion. The EP110 injection weight of 540 g must be equal to or greater than (target preform weight x number of cavities). For example: a 5g preform at 8 cavities requires 40g shot weight, well within the 540 g capacity.
Langkah 2: Hitung Jumlah Rongga yang Diperlukan
Target output (bottles/hour) divided by (3600 seconds / cycle time in seconds) gives required cavities. At a 4 S cycle and 10,000 bottles per hour target: 10,000 / (3600 / 4) = 12 cavities minimum. Cross-check against the cavity table above to confirm the EP110 can deliver this at your bottle volume.
Langkah 3: Verifikasi Kesesuaian Pelat Cetakan
The injection mould layout (cavity array footprint) must fit within the EP110 max platen size of 1100x460 mm. Wide-bottle (diameter greater than 120mm) or tall-bottle (height greater than 220mm) applications exceed the EP110 mould envelope and require a larger model. Confirm your bottle OD and height before specifying cavity count.
Langkah 4: Material dan Tekanan Injeksi
PP requires higher injection pressure and melt temperature than LDPE. PC and PETG require even higher barrel temperatures and longer residence-time plasticization. The EP110 hydraulic system pressure of 14 MPa and motor of 22+22 KW supports the injection forces needed for PP and engineering grade materials at the rated injection weight. Confirm your resin specification with the EVER POWER application team before ordering.
EVER POWER application engineers provide free pre-sales technical consultation to validate your container dimensions, material, cavity count and production target against EP110 specifications. Contact us with your bottle drawing and production brief for a written confirmation of suitability.
Gambaran Umum Struktur Mesin dan Pedoman Perawatan
The EP110 is built around three core functional modules. Understanding their maintenance requirements is essential for sustaining the machine performance metrics - dry cycle, output rate, and product quality - over the full production life of the equipment.
Modul 1 - Unit Injeksi: Sekrup, Barrel, Hot Runner
Unit injeksi melelehkan dan mengukur plastik ke dalam rongga preform. Perawatan harian: periksa profil suhu barel terhadap titik pengaturan, periksa ujung sekrup dan cincin periksa untuk indikator keausan, dan verifikasi suhu zona hot runner berada dalam jarak 2 derajat dari titik pengaturan sebelum memulai. Mingguan: periksa pita isolasi barel, periksa segel silinder injeksi untuk kebocoran oli, dan bersihkan kontaminasi warna dari produksi sebelumnya. Bulanan: lepas dan bersihkan rakitan cincin periksa dan ujung sekrup; periksa ulir sekrup untuk keausan dan ukur diameter lubang barel untuk jarak bebas. Ganti barel jika jarak bebas melebihi toleransi pabrikan untuk mencegah kebocoran lelehan dan ketidaksesuaian berat tembakan.
Prosedur pembersihan: saat mengganti warna gelap ke terang atau dari resin rekayasa ke resin komoditas, gunakan senyawa pembersih komersial pada suhu laras 10 derajat di atas titik pengaturan material baru. Lakukan 5-10 kali pembersihan sebelum beralih ke material baru. Jangan pernah membiarkan laras diam pada suhu pemrosesan selama lebih dari 20 menit tanpa pembersihan - degradasi termal selama periode diam adalah penyebab utama kontaminasi bintik hitam saat memulai kembali.
Modul 2 - Unit Penjepit dan Pengindeksan Putar
Sistem penjepit dan pengindeks putar menanggung beban mekanis tertinggi dan memiliki persyaratan posisi yang paling presisi. Setiap hari: oleskan gemuk pada permukaan batang pengikat dan rel pemandu meja putar sesuai jadwal pelumasan (EVER POWER menentukan jenis gemuk - jangan diganti dengan gemuk serbaguna, yang mungkin tidak mempertahankan viskositas pada suhu operasi). Periksa silinder penjepit hidrolik untuk kebocoran oli pada segel batang. Dengarkan suara yang tidak biasa selama rotasi pengindeksan - bunyi klik logam atau jeda apa pun menunjukkan bantalan pembagi sudut yang perlu diperiksa.
Bulanan: periksa paralelisme pelat dengan indikator dial di keempat posisi batang pengikat; penyimpangan lebih besar dari 0,05 mm memerlukan penyetelan ulang. Periksa akurasi posisi pengindeksan dengan menempatkan indikator dial pada permukaan referensi di turret dan verifikasi bahwa posisi yang sama diulang hingga dalam batas 0,02 mm setelah 100 siklus pengindeksan berturut-turut. Jika terjadi penyimpangan, sesuaikan penghenti mekanis atau hubungi layanan EVER POWER.
Modul 3 - Sistem Hidrolik dan Sirkuit Pendingin
The hydraulic system is the energy backbone of the EP110. System pressure is set at 14 MPa. Daily: check hydraulic oil level in the tank sight glass, check oil temperature display (normal operating range 40-55 degrees Celsius; above 60 degrees indicates a cooling circuit problem or filter blockage), and inspect all visible hydraulic hose fittings for weeping. The oil filter indicator must be checked every 250 hours - a red indicator requires immediate filter element replacement, not deferral.
Cooling circuit: the EP110 requires clean, scale-free cooling water at 0.3-0.4 MPa pressure and 4 M3/h flow. Install a water treatment system upstream of the machine to prevent calcium scale buildup inside mold cooling channels. Scale buildup of just 1mm in a 6mm channel reduces cooling efficiency by over 30%, extending cycle times and reducing output. Flush cooling circuits with a descaling solution annually. Chiller water quality must be neutral pH (6.5-7.5) and contain an anti-corrosion inhibitor compatible with copper and aluminum alloy mold materials.
Solusi Siap Pakai dan Layanan Kustomisasi dari EVER POWER
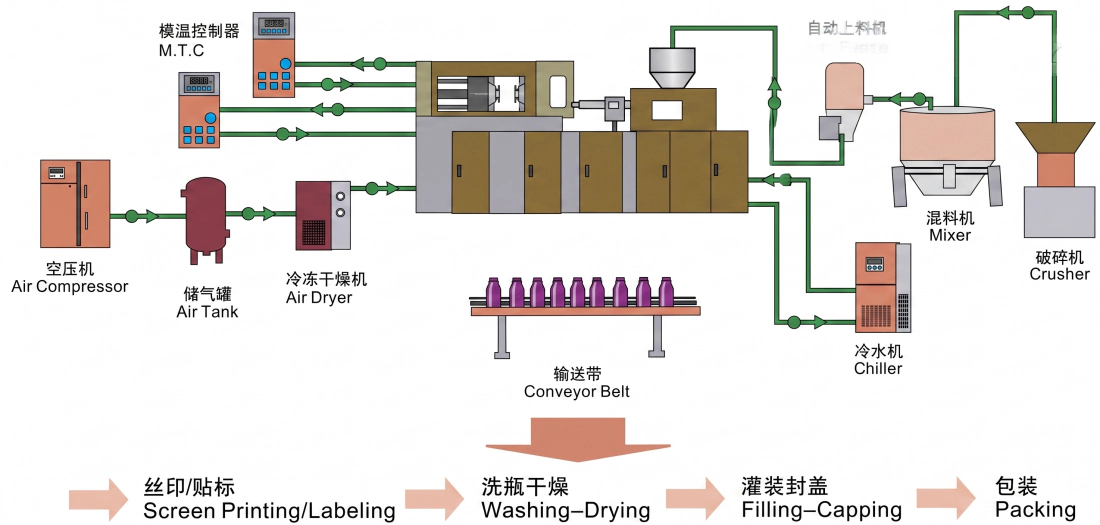
EVER POWER supplies the EP110 as either a standalone machine or as the centerpiece of a complete turnkey bottle production line. For customers setting up a new facility or expanding into a new container product line, the turnkey approach eliminates the integration risk that comes from sourcing the IBM machine, molds, auxiliaries, and downstream equipment from separate vendors.
Desain dan Pembuatan Cetakan
Para insinyur EVER POWER mengembangkan set cetakan injeksi dan tiup dari gambar botol pelanggan atau file 3D. Cetakan hot runner multi-rongga dalam baja S136 atau 4Cr13. Prototipe cetakan rongga tunggal untuk validasi wadah sebelum berkomitmen pada perkakas produksi rongga tinggi. Uji coba cetakan T0 dilakukan di pabrik sebelum pengiriman.
Integrasi Peralatan Bantu
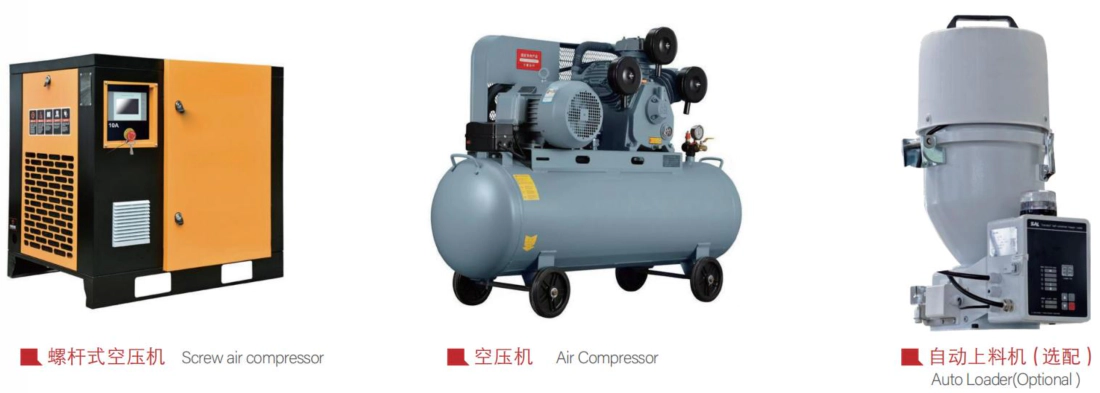
The EVER POWER turnkey line includes: screw air compressor, air tank and air dryer, mold temperature controller, industrial chiller, auto loader, conveyor belt, screen printing and labeling system, washing and drying line, and automatic filling and capping machines. All auxiliary equipment is specified and pre-integrated to match the EP110 output rate.
Sistem Mutu Hilir
Optional inline bottle visual inspection machine (machine vision system for flash, deformation and contamination detection), automatic leak tester, automatic packing machine, and carton erector. For pharmaceutical lines, 100% inline leak testing and vision inspection are available as integrated modules matched to the EP110 conveyor output speed.
Konfigurasi GMP dan Ruang Bersih
Untuk klien farmasi yang membutuhkan produksi berstandar GMP, EVER POWER menawarkan kustomisasi mesin termasuk: pelumasan sistem tertutup untuk mencegah kontaminasi zona produk, penutup pengaman baja tahan karat, penutup mesin dengan filter HEPA agar kompatibel dengan ruang bersih Kelas 100.000, dan dukungan dokumentasi untuk protokol kualifikasi peralatan (IQ/OQ/PQ).
Auxiliary Equipment Available with the EP110
Pengendalian Mutu dan Standar Manufaktur
Pemesinan CNC Komponen Kritis
Rangka mesin, pelat penjepit, dan semua permukaan presisi dikerjakan dengan mesin CNC dalam satu kali pengaturan untuk menjamin akurasi geometris. Paralelisme pelat diverifikasi dengan pengukuran laser hingga 0,02 mm. Lubang batang pengikat diasah hingga toleransi H7 untuk pemasangan bantalan tanpa interferensi.
Pengerasan Induksi Batang Pengikat
Batang pengikat menjalani pengerasan induksi frekuensi tinggi hingga kekerasan permukaan 52-58 HRC diikuti dengan penggerindaan presisi. Perlakuan permukaan ini memberikan ketahanan aus terhadap kontak geser berulang dari pelat penjepit selama jutaan siklus tanpa menyebabkan pengikisan atau gesekan.
Kebersihan Sirkuit Hidraulik
Semua sirkuit hidrolik dibilas, diuji tekanannya, dan jumlah partikelnya diverifikasi sebelum perakitan. Kebersihan oli hidrolik dijaga minimal pada standar ISO 4406 Kelas 17/15/12. Sensitivitas kontaminasi katup proporsional dan servo memerlukan tingkat kebersihan ini untuk mencegah kemacetan katup dan penyimpangan kontrol.
Uji Coba Pabrik Selama 72 Jam
Every EP110 undergoes a minimum 72-hour continuous loaded run test at the factory before shipment. During this period, production output samples are measured for weight consistency, wall thickness uniformity, and dimensional accuracy. Any parameter outside specification triggers a hold and corrective action before the machine is cleared for delivery.
Kepatuhan Keselamatan CE
The EP110 is CE-marked in compliance with EU Machinery Directive requirements. Safety features include: interlocked safety doors with hydraulic circuit interrupt, light curtain protection at the operator access zone, emergency stop at all operator positions, and two-hand operator control for manual mold setting. CE documentation is provided with every machine.
Layanan Purna Jual dan Dukungan Teknis
Instalasi dan Pengoperasian
Insinyur senior EVER POWER bertanggung jawab atas instalasi, pengoperasian awal, dan pengujian penerimaan. Insinyur tetap berada di lokasi hingga mesin mencapai kondisi produksi yang stabil dan semua operator dilatih tentang pengoperasian mesin, penggantian cetakan, dan perawatan rutin. Kriteria penerimaan disepakati sebelum pengiriman dan didokumentasikan dalam laporan pengoperasian awal.
Program Pemeliharaan Preventif
EVER POWER menyediakan layanan pengingat perawatan terjadwal untuk semua mesin yang beroperasi. Kalender perawatan mencakup tugas harian, mingguan, bulanan, dan tahunan. Perawatan proaktif mencegah kerusakan yang tidak direncanakan dan mengurangi kebutuhan pengiriman suku cadang darurat yang mahal. Pelanggan yang mengikuti jadwal perawatan preventif secara konsisten melaporkan ketersediaan mesin di atas 95%.
Layanan Hotline 24x7
Layanan hotline EVER POWER tersedia 24 jam sehari, 7 hari seminggu. Untuk kerusakan produksi yang mendesak, hubungi atau kirim pesan ke layanan hotline dan teknisi yang berkualifikasi akan merespons dalam waktu 2 jam untuk mendiagnosis masalah dari jarak jauh. Jika layanan di lokasi diperlukan, EVER POWER akan mengirimkan teknisi dengan waktu respons minimum yang tersedia untuk lokasi Anda.
Inventaris Suku Cadang
EVER POWER maintains a comprehensive spare parts inventory for all EP110 components including hydraulic seals, proportional valve cartridges, heating bands, temperature sensors, drive belts and electrical components. Parts can be shipped globally within 48 hours for items in stock. Critical fast-wear items are available for customer-held local inventory based on EVER POWER recommendations.
Program Pelatihan Teknis
Selain pelatihan instalasi standar, EVER POWER menawarkan modul pelatihan khusus: pengoperasian mesin, optimasi proses cetakan, penggantian dan pengaturan cetakan, perawatan sistem hidrolik, dan pemecahan masalah proses untuk material tertentu seperti PP, LDPE, dan PCTG. Pelatihan dapat dilakukan di pabrik EVER POWER atau di fasilitas pelanggan.
Frequently Asked Questions - EVER POWER EP110
What materials can the EP110 process?
The EP110 is compatible with HDPE, LDPE, PP, PS (including lactic acid bacteria grade transparent PS), ABS, EVA, bio-based corn material, PCTG, and similar thermoplastics. For engineering resins such as PC, PETG and Tritan, the screw L/D of 22:1 and the 5+N heating zones provide the residence time and temperature profile needed for thorough, degradation-free plasticization. Confirm your resin grade with EVER POWER application engineering before ordering.
Can the EP110 be used for pharmaceutical GMP production?
Yes. The EP110 can be configured for pharmaceutical GMP production environments. Key features supporting GMP include: the one-step process eliminates inter-machine bottle transfer that introduces contamination risk in two-stage systems; the closed lubrication system prevents lubricant contamination of the product zone; and the machine can be specified with a stainless steel safety enclosure suitable for cleanroom installation. EVER POWER can provide equipment documentation to support IQ/OQ/PQ qualification processes for pharmaceutical facility validation.
How long does mould changeover take on the EP110?
A trained two-person team can complete a full mold changeover (injection mold, blow mold, and mandrel set) on the EP110 in approximately 2-4 hours, depending on the mold design and the changeover frequency experience of the team. PLC recipe recall eliminates parameter re-entry time for repeat mold sets. Facilities that invest in quick-release clamping plates for the mold base can reduce changeover to under 2 hours.
What certifications does the EP110 carry?
The EP110 is CE-marked for the European market. The machine design complies with EU Machinery Directive safety requirements including interlocked guards, emergency stop systems, and electrical safety standards. EVER POWER is an ISO-certified manufacturer. Machine documentation is provided in English and can be supplied in other languages upon request for export markets.
What is the lead time for the EP110 and an associated mould set?
Standard machine lead time for the EP110 is 45-75 days from order confirmation and deposit receipt, depending on production schedule at time of order. Mold sets are typically supplied in 60-90 days from final confirmation of bottle drawings and material specification. The machine and mold sets can be scheduled to arrive simultaneously for a coordinated installation. Contact EVER POWER for current lead time at time of inquiry.
Ready to Specify the EVER POWER EP110 for Your Production Line?
Kirimkan gambar botol Anda, volume target, spesifikasi material, dan output per jam yang dibutuhkan ke tim teknik aplikasi kami. Kami akan mengkonfirmasi jumlah rongga dan konfigurasi mesin yang tepat secara tertulis dan memberikan proposal komersial terperinci dalam waktu 3 hari kerja.
Informasi Tambahan
| diedit | oleh hyw |
|---|
Produk Terkait
-
Mesin Cetak Tiup Injeksi Elektrik Sepenuhnya Kecepatan Tinggi EP60HE Tanpa Hidrolik, Siklus 2,5 detik
-
Mesin Cetak Tiup Injeksi Tugas Berat EP135 1350KN IBM Rongga Tinggi untuk Botol Kosmetik dan Farmasi
-
Mesin Cetak Tiup Injeksi Berkecepatan Tinggi EP80 800KN Peralatan Cetak Botol Bebas Sisa Cetakan
-
Mesin Cetak Tiup Injeksi Satu Langkah Otomatis EP60 600KN untuk Produsen Botol Farmasi dan Kosmetik
-
Mesin Cetak Tiup Injeksi Satu Langkah Otomatis EP40 400KN untuk Botol Farmasi dan Kosmetik CE ISO


